Granular fertilizer pneumatic conveying systems represent a critical advancement in bulk material handling technology, particularly within agricultural and industrial sectors. These systems enable efficient, low-loss transport of granular fertilizers through pneumatic means, replacing traditional mechanical methods that often suffer from material degradation and increased maintenance requirements. The core of these systems lies in their ability to use air or gas to suspend and move particles, ensuring consistent performance and reliability across various operational conditions.
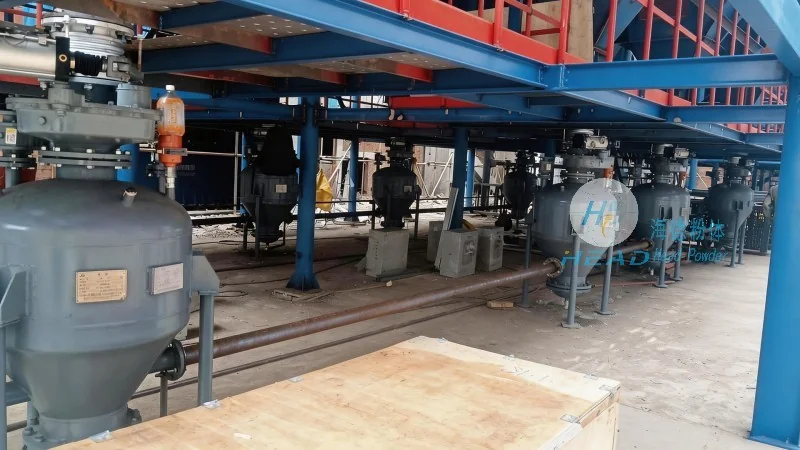
At the heart of granular fertilizer pneumatic conveying systems is the integration of mechanical and pneumatic engineering principles to achieve seamless material transfer. Unlike conventional conveyors such as belt or screw systems, pneumatic conveyors eliminate the need for physical contact with the material, reducing wear and tear on both the equipment and the fertilizer itself. This method is particularly advantageous for friable or sensitive granular fertilizers, as it minimizes breakage and maintains product integrity throughout the conveying process.
The structural design of a granular fertilizer pneumatic conveying system is meticulously engineered to optimize performance and durability. The primary components include:
1. Hopper and Feeder: The hopper serves as the primary storage and feeding unit, where granular fertilizer is held before being introduced into the system. Constructed from corrosion-resistant materials like stainless steel or high-density polyethylene, the hopper ensures longevity and resistance to chemical and physical wear from the fertilizer particles. The feeder, typically a rotary valve or screw feeder, regulates the flow rate of material into the pipeline, maintaining a consistent feed to prevent clogging or uneven transport.
2. Air Compressor or Blower: This component generates the necessary air pressure to propel the fertilizer particles through the pipeline. The choice between a blower and a compressor depends on the system's operational parameters, such as the distance of material transport and the desired air velocity. High-efficiency models are preferred to minimize energy consumption while delivering sufficient pressure to maintain particle suspension.
3. Pipeline Network: The pipeline is the main conduit for transporting the fertilizer. Made from materials like stainless steel or PVC, it is designed to withstand the pressure and abrasive nature of the granular material. The diameter and length of the pipeline are critical design factors, as they directly impact air velocity, pressure drop, and overall system efficiency. Properly sized elbows and fittings ensure smooth material flow and prevent turbulence or blockages.
4. Discharge and Collection Equipment: At the end of the pipeline, a discharge device—such as a rotary valve or a dust collector—controls the release of fertilizer into the target container or storage area. This component ensures that material is discharged smoothly and without creating excessive dust or spillage. In some systems, a dust collector is integrated to filter the air after it has passed through the pipeline, allowing for air recirculation and reducing environmental impact.
The operation of a granular fertilizer pneumatic conveying system follows a systematic sequence, which can be broken down into distinct stages:
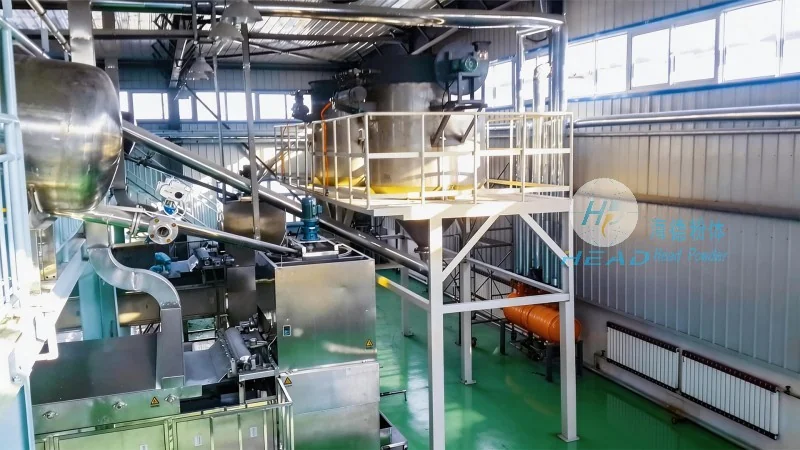
1. Material Loading: Granular fertilizer is loaded into the hopper from a storage silo or delivery truck. The feeder then regulates the flow, ensuring a consistent supply of material into the pipeline.
2. Air Compression and Introduction: The air compressor or blower draws in ambient air and compresses it to a specific pressure. This pressurized air is then introduced into the pipeline, creating a flow that propels the fertilizer particles.
3. Particle Suspension and Transport: As the pressurized air moves through the pipeline, it suspends the fertilizer particles, carrying them along the line. The air velocity must be sufficient to keep particles in suspension and prevent settling or clogging. The system's design ensures that the air velocity remains within optimal ranges to maintain efficient transport.
4. Material Discharge: Upon reaching the discharge point, the pressurized air is released, and the fertilizer is deposited into the target container. The discharge device controls the flow to prevent overfilling or spillage, ensuring precise material delivery.
5. Air Filtration and Recirculation: In systems equipped with dust collectors, the air is filtered to remove particulate matter. The filtered air is then recirculated back into the system, reducing energy consumption and minimizing environmental emissions.
Granular fertilizer pneumatic conveying systems offer several key advantages over traditional conveying methods, making them a preferred choice for many applications:
1. High Efficiency and Low Maintenance: These systems are engineered for continuous operation with minimal downtime, reducing maintenance costs and increasing productivity. The absence of moving parts in the pipeline itself reduces wear and tear, extending equipment lifespan.
2. Minimal Material Loss and Degradation: Unlike mechanical conveyors, pneumatic systems prevent material degradation and reduce loss due to spillage or clogging. This ensures that the fertilizer quality is maintained throughout the conveying process, preserving its nutritional value.
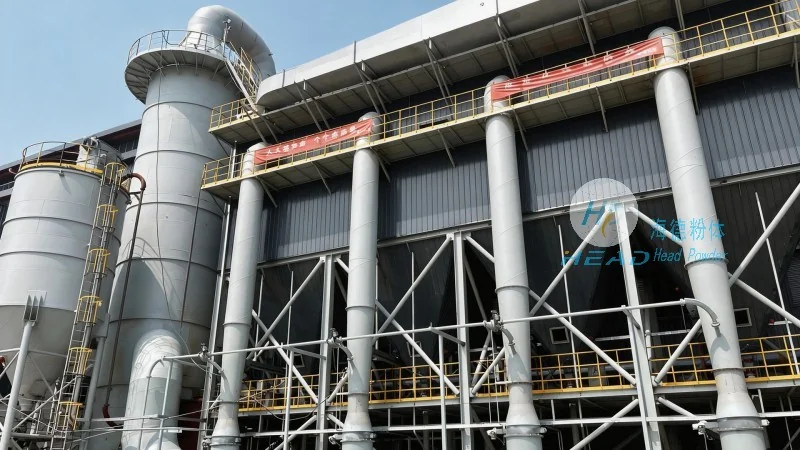
3. Versatility and Scalability: The systems can be customized to handle different types of granular fertilizers and can be scaled up or down to meet the specific needs of the application. This flexibility makes them suitable for a wide range of industrial and agricultural settings, from small-scale farms to large-scale fertilizer production facilities.
4. Energy Efficiency: Modern pneumatic conveying systems are equipped with energy-efficient blowers and compressors, reducing operational costs and environmental impact. The use of recirculated air further enhances energy savings, making these systems environmentally friendly.
Granular fertilizer pneumatic conveying systems are widely utilized across various industries, including:
Agricultural Fertilizer Handling: These systems are commonly employed in farms and fertilizer production facilities to transport bulk granular fertilizers from storage to application equipment or to trucks for distribution. They are particularly useful for transporting nitrogen, phosphorus, and potassium (NPK) fertilizers, which are critical for crop growth.
Industrial Bulk Material Handling: Industries such as chemical, food processing, and mining also utilize pneumatic conveying systems to transport granular materials, including fertilizers, powders, and other bulk products. The systems' ability to handle abrasive or sensitive materials makes them ideal for these applications.
Construction and Infrastructure: In construction projects, these systems can be used to transport granular materials like sand, gravel, and cement, improving efficiency and reducing labor costs. They are particularly useful in large-scale projects where material transport over long distances is required.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of granular fertilizer pneumatic conveying systems, specializes in providing high-quality, customized solutions for bulk material handling. With a focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the industry. HeadPowder's systems are designed to meet the specific needs of clients, ensuring reliable and efficient operation. The company's headquarters is located in Shandong, China, where it continues to develop and improve its products to meet the evolving demands of the market. By leveraging advanced engineering and manufacturing techniques, HeadPowder delivers systems that enhance productivity and reduce operational costs for its customers.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top