For industries that require efficient and reliable material transfer, vacuum pneumatic conveying systems offer a versatile solution. These systems are designed to handle a wide range of bulk materials, from powders and granules to fine particles, with precision and minimal product degradation. The equipment, often referred to as vacuum material handling systems, is engineered to meet the demands of various sectors, including pharmaceuticals, food processing, and chemical manufacturing. In this overview, we will explore the key components, operational principles, and practical applications of vacuum pneumatic conveying equipment, highlighting how it enhances productivity and operational efficiency.
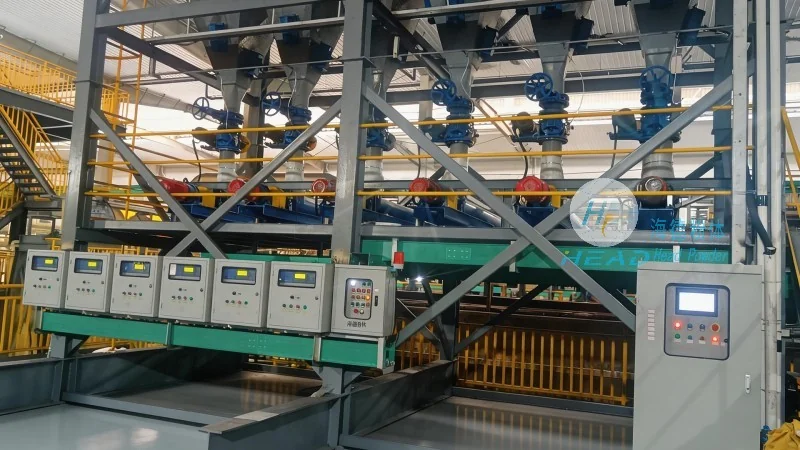
Vacuum material handling systems are integral to modern industrial processes, providing a clean, closed-loop method for transporting bulk materials. Unlike positive pressure systems that use compressed air to push material through pipelines, vacuum systems operate by creating a negative pressure environment that draws material from the source to the destination. This approach minimizes dust emissions, reduces product contamination, and ensures a safer working environment. The technology is particularly advantageous for materials that are sensitive to air exposure or require gentle handling, such as pharmaceutical powders, food ingredients, and fine chemicals.
The vacuum conveying system consists of several critical components that work in tandem to achieve efficient material transfer. The main elements include a vacuum pump, a material feed hopper, a conveying line, a receiver or collection tank, and a control system. The vacuum pump is the heart of the system, generating the negative pressure necessary to draw material into the pipeline. The feed hopper is where the material is loaded, and it often includes a rotary valve or feeder to regulate the flow. The conveying line, typically made of stainless steel or other corrosion-resistant materials, transports the material from the source to the receiver. The receiver collects the material and may include a filter or cyclone to separate any entrained air or particles. The control system manages the operation of the pump, feed valve, and other components, ensuring smooth and consistent operation.
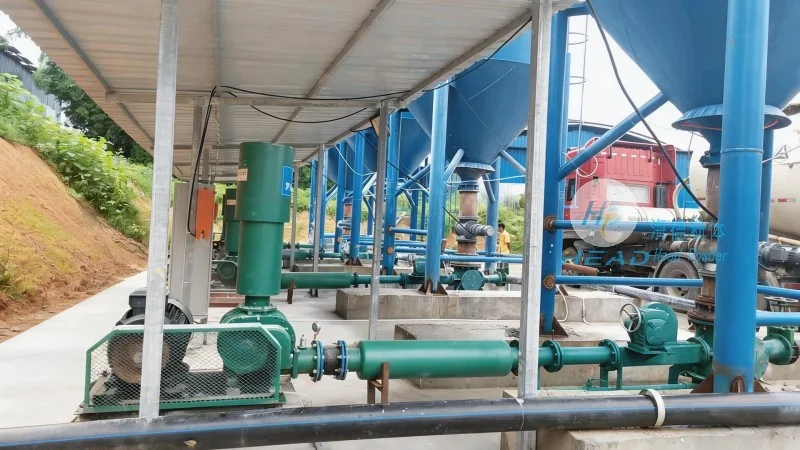
The operational principle of a vacuum pneumatic conveying system is based on the creation of a pressure differential between the source and the destination. The vacuum pump reduces the pressure inside the conveying line, creating a negative pressure that pulls material from the feed hopper into the pipeline. As the material is drawn into the line, it is mixed with a small amount of air, forming a slurry or suspension that travels through the pipeline. The receiver at the end of the line then separates the material from the air, typically using a filter or cyclone, and collects the material in a storage container. The air, now free of material particles, is either vented to the atmosphere or recirculated back to the system, depending on the design. This closed-loop operation ensures minimal air loss and maintains the integrity of the material being conveyed.
Vacuum pneumatic conveying equipment is widely used across various industries due to its versatility and efficiency. In the pharmaceutical industry, it is used to transfer sensitive powders and granules, ensuring product purity and preventing contamination. In food processing, it handles ingredients like flour, sugar, and spices, maintaining food safety standards. The chemical industry utilizes these systems for transporting fine chemicals and powders, reducing the risk of dust explosions and product degradation. The benefits of vacuum conveying include reduced labor costs, improved product quality, and enhanced safety. Additionally, the closed system minimizes dust emissions, making it environmentally friendly and compliant with regulatory standards.
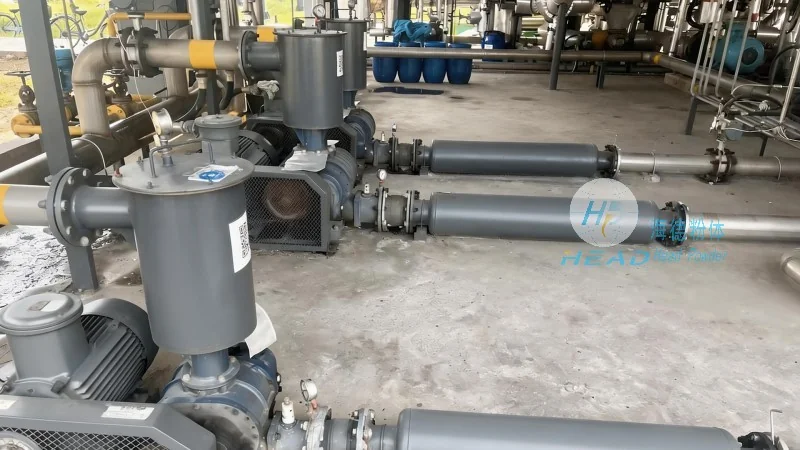
Headpowder, the professional manufacturer of vacuum pneumatic conveying equipment, is dedicated to providing high-quality solutions for material handling challenges. With years of experience in the industry, the company specializes in designing and manufacturing customized vacuum conveying systems tailored to the specific needs of clients. Headpowder's products are engineered with precision and durability, ensuring long-term performance and reliability. The company's headquarters is located in Shandong, China, where a team of skilled engineers and technicians work to develop innovative solutions that meet the evolving demands of the market. Headpowder's commitment to quality and customer satisfaction has made it a trusted partner for industries worldwide, offering reliable and efficient material handling solutions.
Vacuum pneumatic conveying equipment is a critical component in modern industrial operations, offering efficient, safe, and reliable material transfer solutions. By understanding the structure and working principles of these systems, industries can optimize their processes and enhance productivity. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can access advanced vacuum conveying systems that meet their specific requirements, ensuring long-term success and operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top