HeadPowder, a leading provider of industrial conveying solutions, specializes in advanced pneumatic conveying systems tailored for various industrial applications. This article provides an overview of the desulfurization sodium bicarbonate pneumatic conveying system, detailing its structural design and operational principles to help clients understand its functionality and benefits.
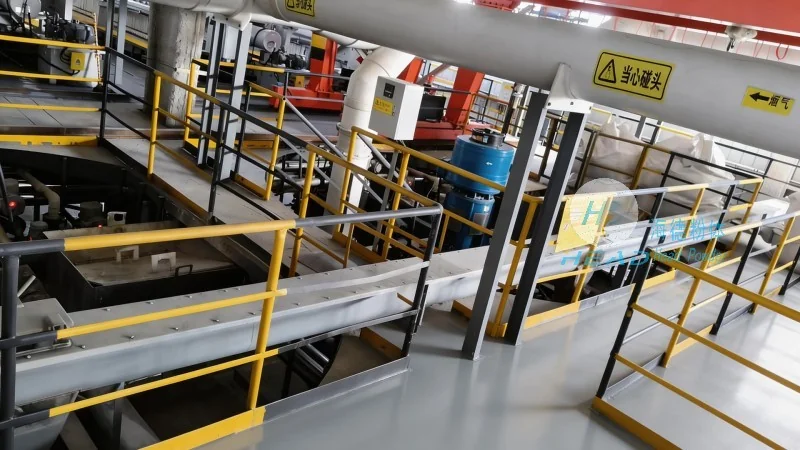
The desulfurization sodium bicarbonate pneumatic conveying system is engineered to efficiently transport sodium bicarbonate, a key chemical used in flue gas desulfurization processes. This system combines precision engineering with robust materials to ensure reliable performance in demanding industrial environments. HeadPowder's expertise in material handling and process optimization has led to the development of this specialized system, which meets the stringent requirements of modern desulfurization plants.
The system comprises several critical components that work in tandem to achieve efficient material transport. These include a feed hopper for material storage and dosing, a rotary airlock valve to control material flow, a main conveying pipe network that transports the material, and a receiver for material discharge. The design incorporates high-quality stainless steel and corrosion-resistant materials to withstand the chemical properties of sodium bicarbonate and the operational conditions of desulfurization plants. Additionally, the system features adjustable air pressure controls and flow monitoring mechanisms to ensure optimal performance and prevent material blockages or system inefficiencies.
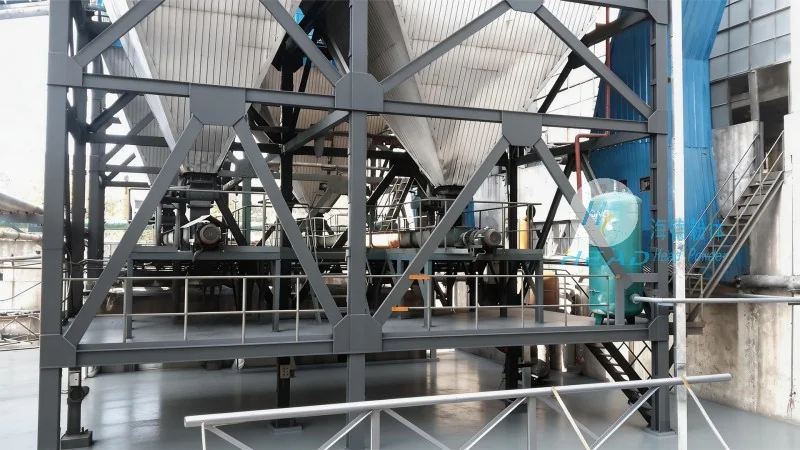
The pneumatic conveying process operates on the principle of using compressed air to move material through a pipeline. In the desulfurization sodium bicarbonate system, the process begins with material being fed from the hopper into the rotary airlock valve. The airlock valve regulates the flow of sodium bicarbonate into the conveying pipe, where it is mixed with high-pressure air. The air and material mixture is then propelled through the pipeline to the receiver, where the material is separated from the air and collected. The system utilizes positive displacement or dilute phase conveying methods, depending on the specific application requirements, to ensure efficient and consistent material transport. The air pressure and flow rate are carefully controlled to maintain the optimal velocity for material movement, minimizing wear on components and maximizing system efficiency.
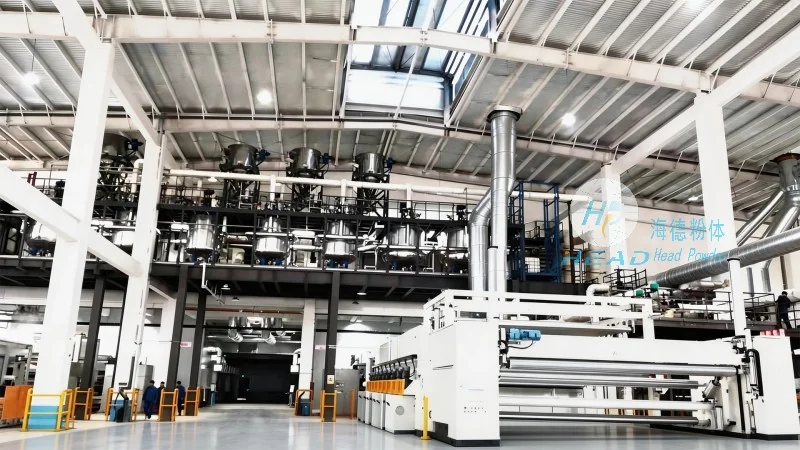
Implementing the desulfurization sodium bicarbonate pneumatic conveying system offers several advantages for industrial facilities. The system enhances operational efficiency by reducing manual handling and labor costs, while ensuring consistent material delivery to the desulfurization reactors. It also minimizes material loss and contamination, which is crucial for maintaining the quality of the desulfurization process. Furthermore, the system's compact design and flexible installation options make it suitable for various plant layouts and space constraints. HeadPowder's system is widely used in power plants, chemical manufacturing facilities, and other industrial sites where reliable and efficient transport of sodium bicarbonate is essential for effective flue gas desulfurization.
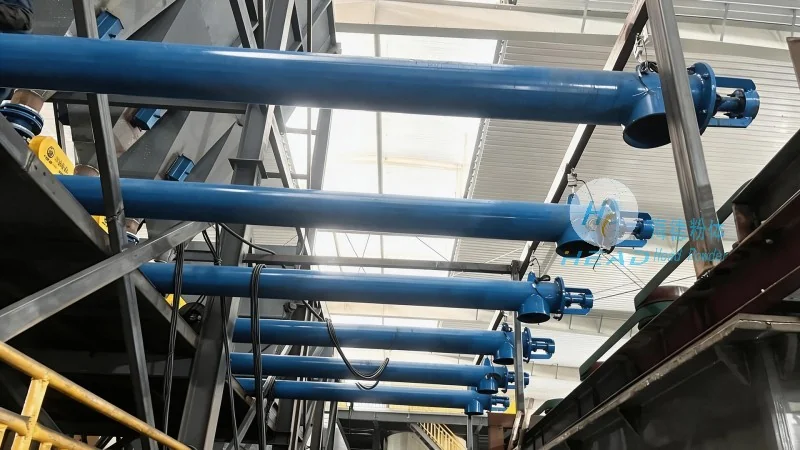
HeadPowder offers customizable solutions to meet the unique needs of each client. The desulfurization sodium bicarbonate pneumatic conveying system can be tailored with different pipe diameters, air pressure ranges, and material handling capacities. The system can also be integrated with automation controls, such as PLC systems, to enhance monitoring and control capabilities. Additionally, the company provides comprehensive technical support and maintenance services to ensure the long-term reliability and performance of the system. With a focus on durability and efficiency, HeadPowder's system is designed to deliver consistent performance over extended operational periods, providing a reliable solution for industrial material transport needs.
The desulfurization sodium bicarbonate pneumatic conveying system by Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated and efficient solution for transporting sodium bicarbonate in flue gas desulfurization processes. By combining advanced structural design with reliable operational principles, the system ensures optimal performance, minimal maintenance, and cost-effective operation. HeadPowder's commitment to quality and innovation has made this system a preferred choice for industrial facilities seeking to enhance their material handling capabilities and improve overall process efficiency. With its headquarters in Shandong, China, HeadPowder continues to provide cutting-edge solutions to meet the evolving needs of the industrial sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top