For industrial applications that require precise and efficient material handling, the tonne bag quantitative feeding pneumatic conveying system has emerged as a reliable solution. This equipment is designed to handle bulk materials from large tonne bags with high accuracy and minimal waste, making it ideal for various sectors including food processing, pharmaceuticals, and chemical manufacturing. The system integrates advanced technology to ensure consistent material flow and maintain product integrity throughout the conveying process.
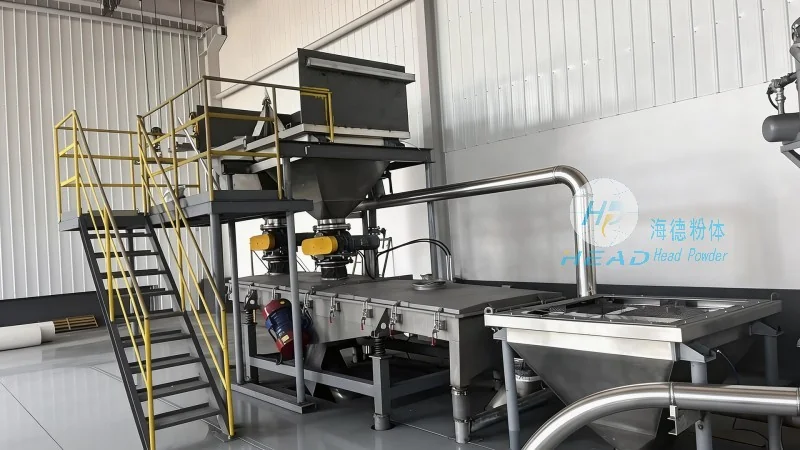
The tonne bag quantitative feeding pneumatic conveying equipment is a specialized system developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of powder handling technology. This system is engineered to automate the process of extracting and conveying bulk materials from tonne bags, which are commonly used for storing large quantities of dry powders and granules. The primary goal of this equipment is to provide a precise, controlled, and hygienic method for material transfer, reducing manual labor and enhancing operational efficiency in industrial settings.
The pneumatic conveying system consists of several critical components that work in tandem to achieve accurate material feeding and transport. The main parts include the hopper, the feeding mechanism, the airlock valve, the conveying line, and the discharge outlet. The hopper is designed to hold the material from the tonne bag and provide a stable feed source. The feeding mechanism, often a rotary valve or a screw feeder, regulates the flow of material into the conveying line. The airlock valve, typically a rotary or sliding type, ensures that material is discharged from the hopper into the conveying line without air leakage or backflow. The conveying line, usually made of stainless steel or other corrosion-resistant materials, transports the material through the system under pressure. The discharge outlet is where the material is released into the next processing stage, such as a mixer or a storage silo.
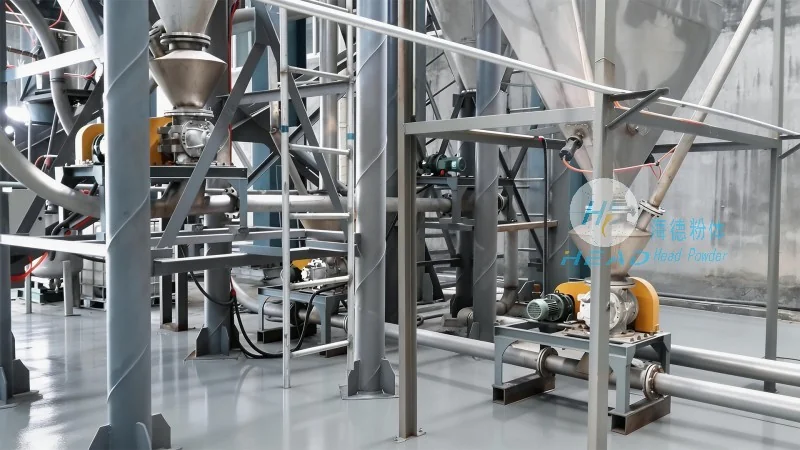
The operation of the tonne bag quantitative feeding pneumatic conveying equipment is based on the principle of pneumatic transport, where air is used to move the material through a pipeline. The system operates by creating a pressure differential between the hopper and the discharge point. Compressed air is introduced into the hopper, which lifts the material and draws it into the conveying line. The air and material mixture travels through the pipeline under pressure, and the airlock valve at the discharge end controls the release of material into the subsequent process. The system is equipped with sensors and control panels to monitor and adjust the flow rate, ensuring that the material is conveyed at the desired rate and with the required accuracy. This closed-loop system minimizes dust emissions and maintains a clean working environment, which is crucial for industries that handle sensitive or hygienic materials.
A key feature of the tonne bag quantitative feeding pneumatic conveying equipment is its ability to provide precise and consistent material feeding. The system is designed to handle a wide range of materials, from fine powders to coarse granules, with minimal segregation or degradation. The feeding mechanism is adjustable, allowing operators to set the desired flow rate based on the material properties and processing requirements. This precision feeding capability is essential for applications where accurate dosing is critical, such as in pharmaceutical manufacturing or food processing, where product quality and consistency are paramount. The equipment also features a dust collection system to capture any airborne particles, ensuring that the working environment remains clean and safe for personnel.
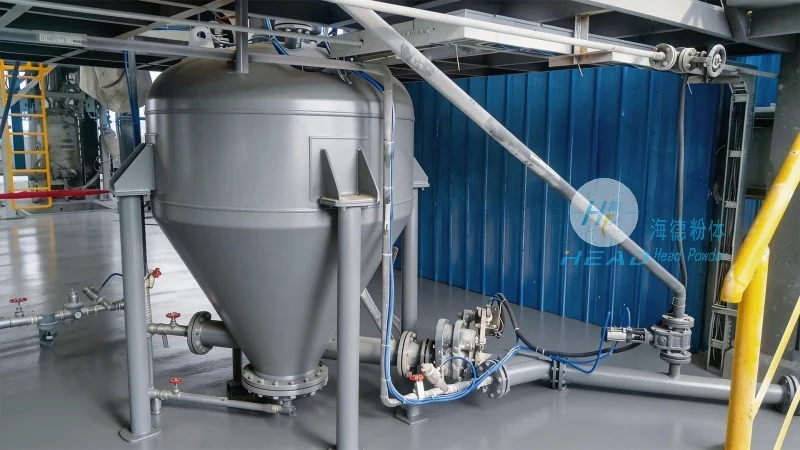
The tonne bag quantitative feeding pneumatic conveying equipment offers several advantages over traditional material handling methods. It reduces the need for manual handling of large tonne bags, which can be heavy and cumbersome. The automated system minimizes human error and improves safety by eliminating the risk of overfilling or underfilling. Additionally, the closed system prevents dust contamination and maintains product purity, which is essential for industries that require high standards of hygiene. The equipment is versatile and can be adapted to various industrial applications, including chemical processing, food and beverage production, and pharmaceutical manufacturing. It is particularly useful in facilities that handle large volumes of bulk materials, as it can significantly increase throughput and reduce processing time.
Shandong HeadPowder Engineering Co., Ltd. has developed the tonne bag quantitative feeding pneumatic conveying equipment as a reliable solution for efficient and precise material handling. The system combines advanced technology with robust construction to meet the demands of modern industrial applications. By automating the process of extracting and conveying bulk materials from tonne bags, the equipment enhances operational efficiency, reduces labor costs, and maintains product quality. With its precision feeding capabilities and hygienic design, this equipment is an ideal choice for industries that require high standards of material handling and processing. Based in China, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide cutting-edge solutions for the powder handling industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top