Activated carbon is a critical material in various industrial applications, including air purification, water treatment, and chemical processing. The efficient and reliable transportation of activated carbon from storage to processing units is essential for maintaining production efficiency and product quality. Pneumatic conveying systems offer a versatile solution for handling activated carbon, leveraging the principles of air flow to move material through pipelines. This article provides an overview of the structure and working principles of activated carbon pneumatic conveying systems, highlighting key components and operational mechanisms.
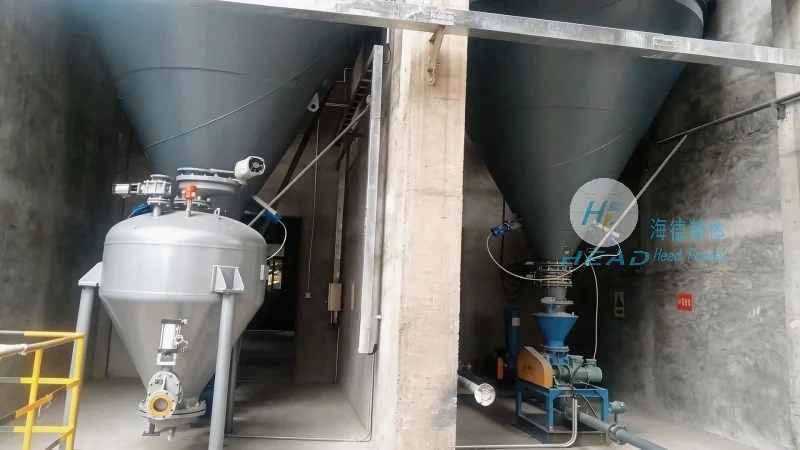
The activated carbon pneumatic conveying system consists of several essential components that work in concert to transport material. The primary components include a material hopper, a rotary airlock valve, a conveying pipeline, a venturi or airlock device for material discharge, and a dust collector or filter system. The material hopper is designed to store the activated carbon, ensuring a consistent feed to the system. The rotary airlock valve, positioned at the hopper outlet, controls the flow of activated carbon into the pipeline, preventing backflow and maintaining a steady material feed rate. The conveying pipeline, typically made of stainless steel or other corrosion-resistant materials, is designed to withstand the abrasive nature of activated carbon and the pressure differentials involved in the conveying process. The venturi or airlock device at the discharge end facilitates the separation of material from the air stream, allowing for the collection of activated carbon in the receiving vessel. Finally, the dust collector or filter system is crucial for capturing any airborne particles, ensuring compliance with environmental regulations and maintaining a clean operational environment.
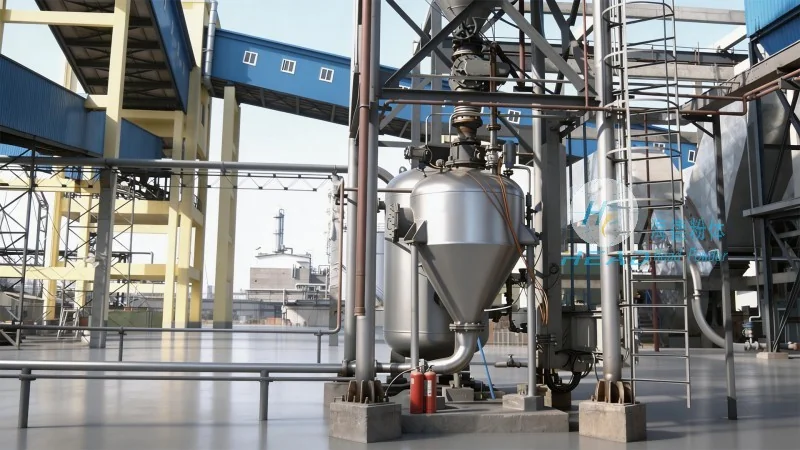
The operation of an activated carbon pneumatic conveying system is based on the principle of air flow and pressure differentials. There are two main types of pneumatic conveying systems: dilute-phase and dense-phase. Dilute-phase systems operate at higher air velocities, typically 20-30 m/s, and are suitable for short to medium-distance transport. In this system, the activated carbon is suspended in the air stream as a fine mist, allowing for efficient transport through the pipeline. The material is introduced into the pipeline via the rotary airlock valve, and the high-velocity air stream carries the material forward. At the discharge end, the venturi or airlock device reduces the air velocity, causing the activated carbon to settle out and be collected. Dense-phase systems, on the other hand, operate at lower air velocities, typically 5-10 m/s, and are used for longer-distance transport or when handling more abrasive materials. In dense-phase systems, the activated carbon is conveyed in a slurry-like state, with the air stream providing the necessary pressure to move the material through the pipeline. The rotary airlock valve and conveying pipeline work together to maintain the material's flow, and the discharge device ensures a controlled release of the material into the receiving container.
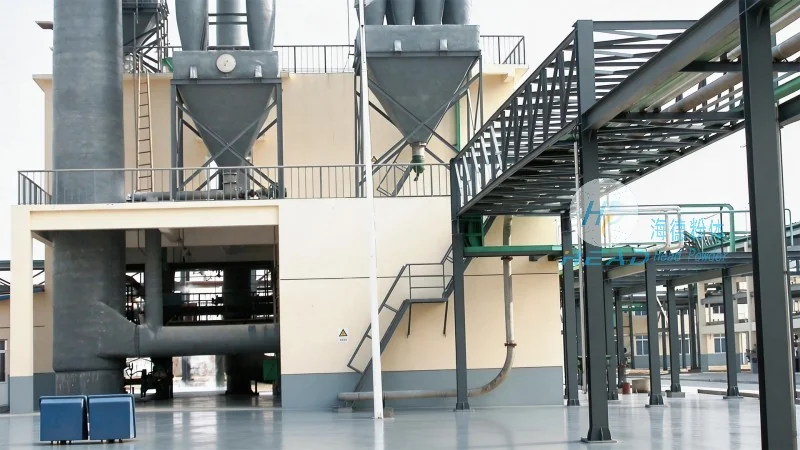
Activated carbon pneumatic conveying systems offer several advantages over traditional mechanical conveying methods. These include reduced labor costs, as the system can operate automatically with minimal human intervention. The enclosed pipeline system minimizes dust emissions, improving workplace safety and environmental compliance. Additionally, the system is highly flexible, allowing for easy integration with existing production lines and the ability to transport activated carbon to multiple destinations. The ability to handle abrasive materials without causing wear and tear on equipment is another significant advantage. Furthermore, the system's compact design and low maintenance requirements contribute to overall operational efficiency and cost-effectiveness.
Activated carbon pneumatic conveying systems are widely used in various industries that rely on activated carbon for their processes. In the chemical industry, these systems are used to transport activated carbon for adsorption processes, where the material is used to remove impurities from liquids or gases. The food and beverage industry utilizes activated carbon for water treatment and flavor removal, requiring efficient and clean transportation of the material. The pharmaceutical industry also benefits from these systems, as they help maintain the purity and quality of activated carbon used in drug manufacturing and purification processes. Additionally, the environmental industry, particularly in water treatment plants, relies on activated carbon for removing contaminants from wastewater, making the pneumatic conveying system an essential part of the overall treatment process.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of pneumatic conveying systems and related equipment. With a focus on innovation and quality, HeadPowder has established itself as a trusted partner in the industry, providing customized solutions for various material handling needs. The company's products are designed to meet the specific requirements of different industries, ensuring optimal performance and reliability. HeadPowder's commitment to customer satisfaction and technological advancement has made it a preferred choice for businesses seeking efficient and effective material handling solutions. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility and research and development center. HeadPowder's team of experts is dedicated to providing comprehensive support, from system design and installation to maintenance and after-sales service, ensuring that clients receive the best possible service throughout the lifecycle of their equipment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top