For industrial applications involving sodium hydroxide (NaOH), efficient and reliable material handling is crucial. The pneumatic conveying system designed by Shandong HeadPowder Engineering Co., Ltd. offers a robust solution for transporting this caustic chemical safely and effectively. This article provides an overview of the system's structure and operational principles, highlighting its key components and benefits.
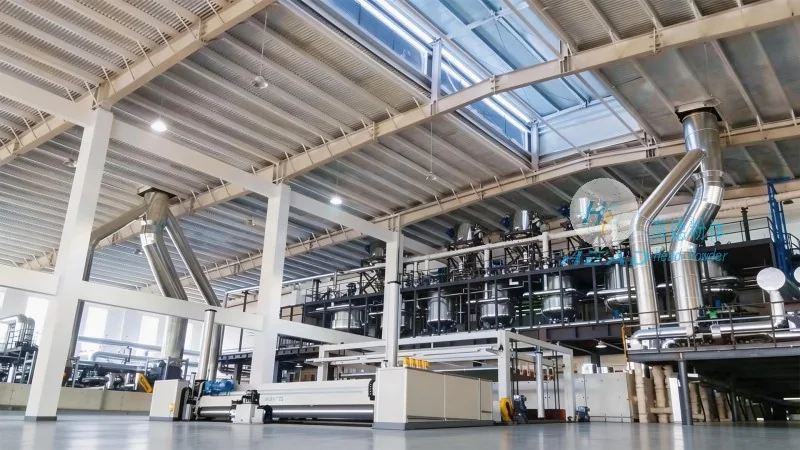
The sodium hydroxide pneumatic conveying system comprises several critical components that work in tandem to ensure smooth material transport. The primary elements include a hopper for material storage, a rotary valve for controlled discharge, a conveying pipeline, a dust collector to manage airborne particles, and a receiver for the discharged material. Each component is engineered to handle the specific properties of sodium hydroxide, such as its hygroscopic nature and potential reactivity with air.
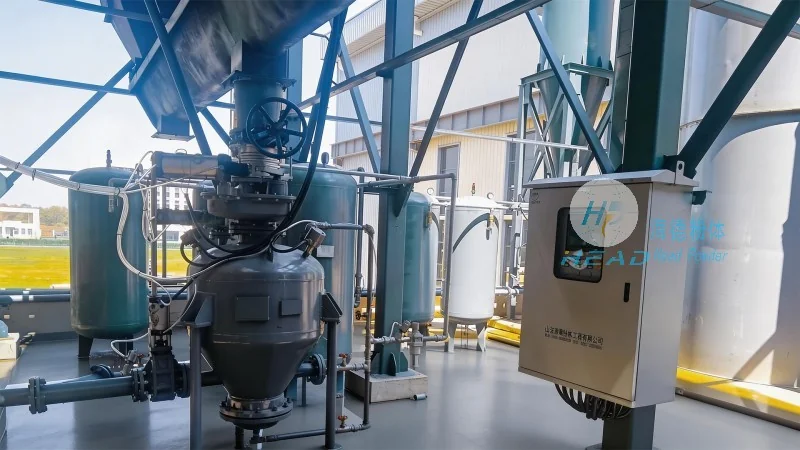
The system operates on the principle of pneumatic transport, where air or gas is used to move the material through the pipeline. In this setup, a blower or compressor generates the necessary airflow, which draws the sodium hydroxide from the hopper through the rotary valve into the conveying line. The material is then carried by the air stream to the destination point, where it is deposited into the receiver. The dust collector attached to the system captures any fine particles that may escape, ensuring compliance with environmental regulations and maintaining a clean working environment.
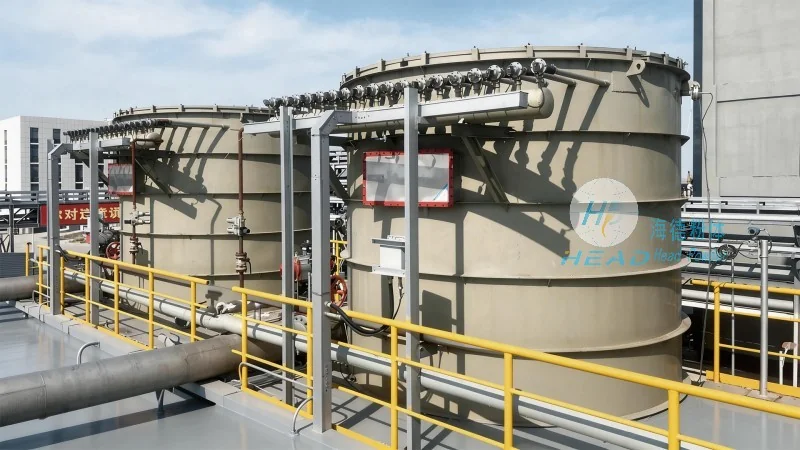
Implementing a pneumatic conveying system for sodium hydroxide offers several advantages over traditional methods like belt conveyors or manual handling. First, it minimizes the risk of exposure to the chemical, as the material is contained within the pipeline, reducing the chance of contact with personnel. Second, the system provides a continuous and consistent flow, improving production efficiency and reducing downtime. Third, it eliminates the need for manual handling, which can be hazardous due to the caustic nature of sodium hydroxide. Additionally, the system is compact and can be integrated into existing industrial setups, making it a flexible solution for various production environments.
The pneumatic conveying system is widely used in industries such as chemical manufacturing, food processing, and pharmaceuticals, where sodium hydroxide is a key raw material. Proper maintenance is essential to ensure the system's longevity and performance. Regular checks of the blower, rotary valve, and pipeline for wear and tear are recommended. Additionally, the dust collector should be cleaned periodically to prevent clogging and maintain optimal airflow. By adhering to these maintenance practices, the system can operate efficiently for extended periods, providing reliable service to the end-user.
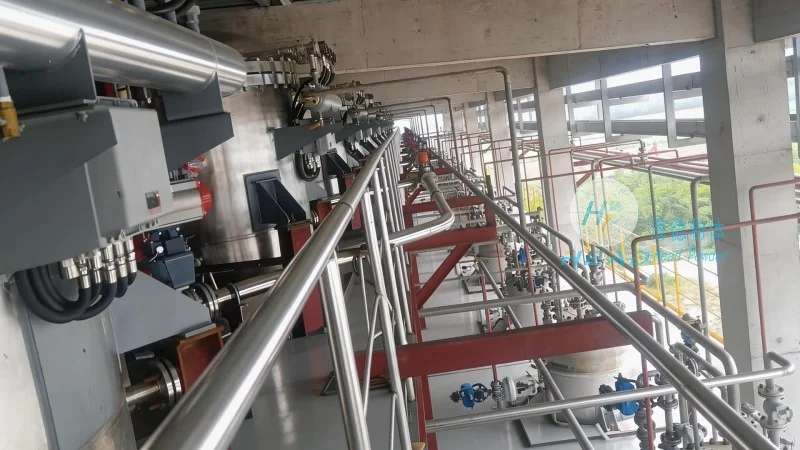
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design and manufacturing of advanced material handling systems. With a focus on innovation and quality, the company provides tailored solutions for various industrial applications, including the sodium hydroxide pneumatic conveying system. HeadPowder's commitment to safety and efficiency has made it a trusted partner for businesses seeking reliable material transport solutions. The company's headquarters is located in Shandong, China, where it continues to develop cutting-edge technologies to meet the evolving needs of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top