HeadPowder, a leading provider of industrial powder handling solutions, specializes in the design, manufacturing, and integration of advanced pneumatic conveying systems tailored for ingredient blending applications. With a strong presence in China, particularly in Shandong, the company leverages its expertise to deliver efficient and reliable systems that meet the demands of modern processing industries.
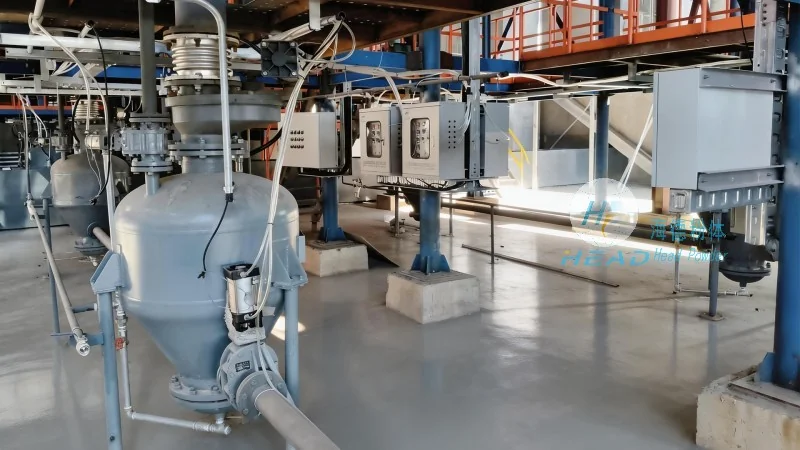
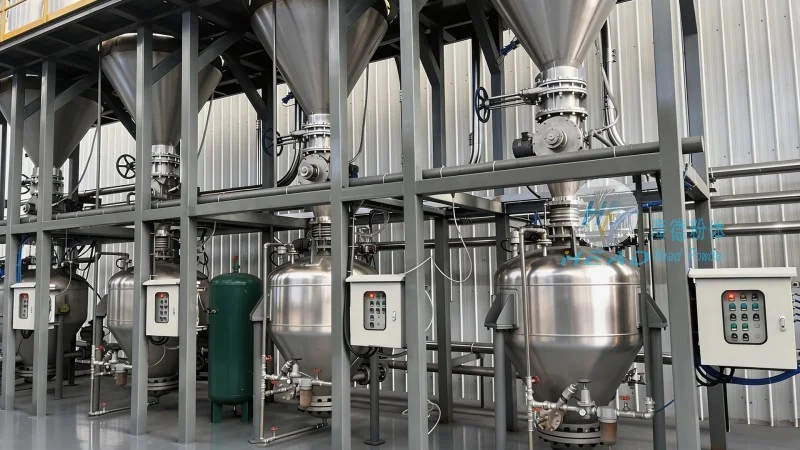
The core of a powder mixing and pneumatic conveying system lies in its ability to transport bulk powders through a pressurized or vacuum environment using air or other gases. This method, known as pneumatic conveying, offers several advantages over traditional mechanical conveying, such as reduced contamination risk, lower maintenance requirements, and enhanced process control. The system typically consists of a hopper for material storage, a conveyor line (either positive or negative pressure), and a mixing chamber where ingredients are combined. The air flow is carefully regulated to ensure uniform particle distribution and consistent blending ratios. By controlling the velocity and pressure of the air, the system can handle a wide range of powder characteristics, including fine powders, bulk materials, and those with varying moisture content. This flexibility makes it suitable for diverse applications in pharmaceuticals, food processing, chemicals, and other industries where precision and hygiene are critical.
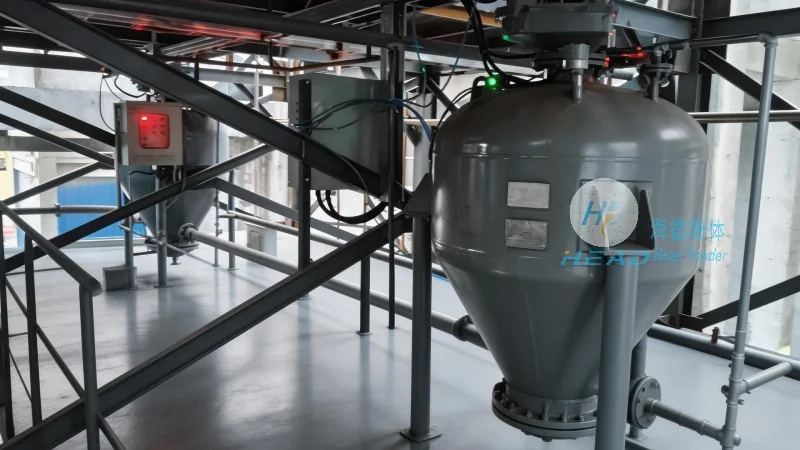
The working scene characteristics of a powder mixing and pneumatic conveying system are defined by its operational efficiency, adaptability, and integration capabilities. In industrial settings, these systems are often deployed in environments where space is optimized, and process flow is streamlined. The system's design allows for seamless integration with existing production lines, enabling continuous or batch processing of ingredients. A notable characteristic is its ability to handle multiple raw materials simultaneously, facilitating complex blending tasks that require precise proportioning. The pneumatic conveying aspect ensures that materials are transported without direct contact with machinery, minimizing the risk of cross-contamination and product degradation. Additionally, the system's modular design allows for easy scalability, enabling companies to expand their operations as production needs grow. This adaptability is crucial for businesses operating in dynamic markets where product lines may evolve or production volumes fluctuate. The working scene also emphasizes energy efficiency, with modern systems incorporating advanced control technologies to optimize air usage and reduce operational costs. By maintaining consistent air pressure and flow rates, the system ensures stable performance while minimizing energy consumption, contributing to overall cost savings and environmental sustainability.
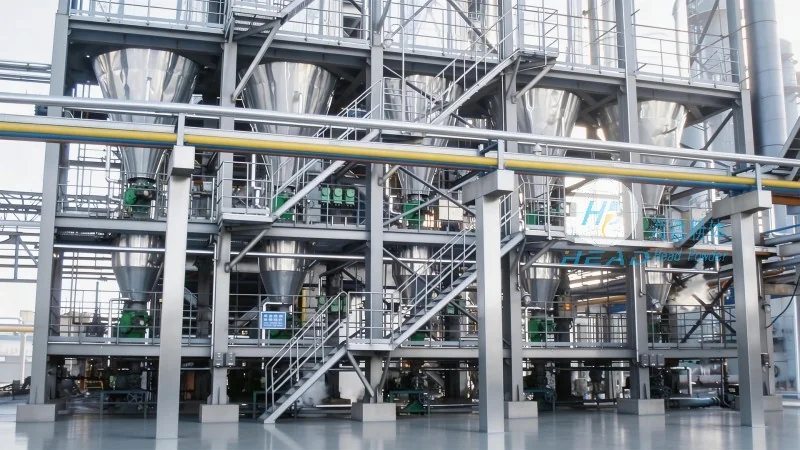
When applied in real-world scenarios, the powder mixing and pneumatic conveying system from HeadPowder delivers tangible benefits that enhance operational performance. For instance, in the food industry, the system's hygienic design and ability to handle sensitive ingredients ensure compliance with regulatory standards. The consistent blending ratios achieved through precise air control improve product quality and reduce waste. In the pharmaceutical sector, the system's contamination control features are paramount, as even minor impurities can affect product efficacy. The system's performance is often measured by key metrics such as conveying capacity, blending accuracy, and system efficiency. These metrics are critical for evaluating the system's suitability for specific applications and for making informed decisions about system upgrades or replacements. HeadPowder's commitment to quality and innovation ensures that its systems meet or exceed industry standards, providing customers with reliable and long-lasting solutions. The company's focus on customer needs and process optimization has made it a trusted partner for businesses seeking to enhance their powder handling capabilities. By understanding the unique requirements of each client, HeadPowder tailors its systems to deliver optimal performance and value.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top