HeadPowder, a leading provider in the field of powder handling technology, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems. This article delves into the fundamental principles of continuous material handling powder pneumatic conveying systems, exploring how these systems operate and the specific scenarios where they excel in industrial applications. By understanding the core mechanics and application nuances, industries can optimize their material transport processes, enhance efficiency, and ensure consistent performance in various operational environments.
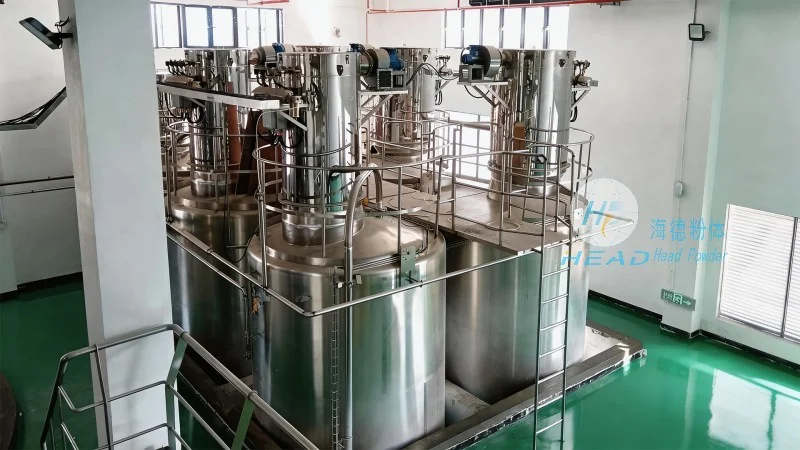
The foundation of continuous material handling powder pneumatic conveying systems lies in the use of pressurized or vacuum air to transport bulk powders through a network of pipes. The system typically comprises several key components, including a material feed hopper, a conveying line, a control valve, and a discharge unit. The process begins with the powder being fed into the system, where it is then entrained by the air flow, creating a slurry-like mixture that travels through the pipeline. This method offers several advantages over traditional mechanical conveying, such as reduced equipment wear, lower maintenance requirements, and the ability to handle a wide range of powder types, from fine to coarse particles. The continuous operation mode ensures a steady flow of material, making it ideal for high-throughput applications in sectors like pharmaceuticals, food processing, and chemical manufacturing.
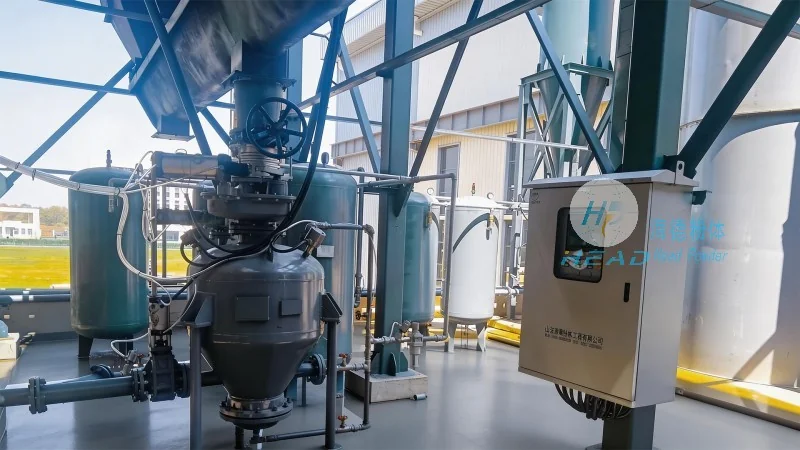
Each component within a continuous material handling powder pneumatic conveying system plays a critical role in ensuring smooth and efficient operation. The material feed hopper is responsible for storing and feeding the powder into the system, often equipped with a rotary valve or a screw feeder to control the flow rate. The conveying line, usually made of stainless steel or other corrosion-resistant materials, is designed to withstand the pressure and temperature variations of the material being transported. The control valve, which can be a venturi or a rotary valve, regulates the air flow and pressure, ensuring optimal conveying conditions. The discharge unit, typically a cyclone separator or a filter, separates the powder from the air stream, allowing the material to be collected in a storage bin or processing unit. The integration of these components ensures that the system operates with minimal downtime and maximum reliability, even under continuous operational demands.
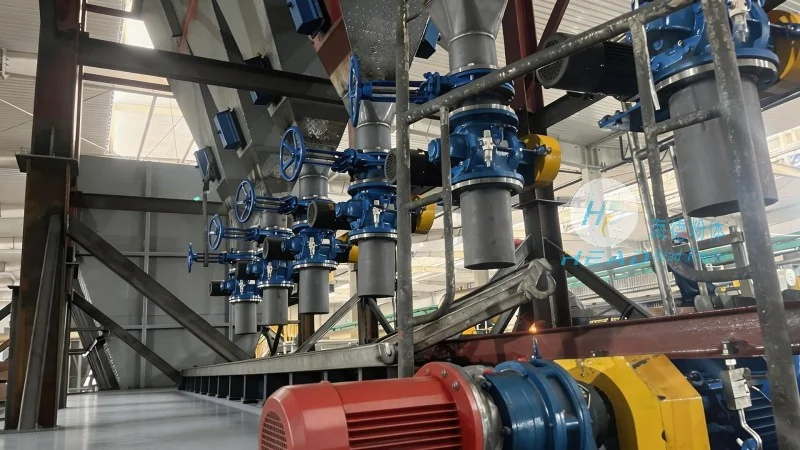
Continuous material handling powder pneumatic conveying systems are particularly well-suited for applications requiring consistent and uninterrupted material transport. In pharmaceutical manufacturing, for example, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients with high precision, ensuring that the material remains free from contamination and maintains its quality throughout the process. The systems are also widely used in food processing industries, where they handle powders like sugar, flour, and spices, maintaining hygiene standards and preventing cross-contamination. In chemical manufacturing, the systems are employed to transport reactive powders and hazardous materials, providing a safe and enclosed environment that minimizes the risk of accidents and exposure. The versatility of these systems allows them to adapt to various operational scenarios, from small-scale laboratory applications to large-scale industrial production lines, making them a preferred choice for industries seeking reliable and efficient material handling solutions.
Implementing continuous material handling powder pneumatic conveying systems offers numerous advantages for industrial operations. One of the primary benefits is the reduction in labor costs, as the system operates automatically with minimal human intervention. The enclosed nature of the system also enhances safety by preventing dust emissions and minimizing the risk of material exposure to the environment. Additionally, the systems are highly scalable, allowing businesses to expand their operations without significant changes to the existing infrastructure. The continuous flow capability ensures that production lines remain uninterrupted, leading to increased productivity and reduced downtime. Furthermore, the systems are energy-efficient, as they use compressed air only when necessary, and can be integrated with existing plant systems to optimize energy usage. These advantages make continuous material handling powder pneumatic conveying systems a cost-effective and sustainable solution for industries looking to improve their material transport processes.
Continuous material handling powder pneumatic conveying systems represent a sophisticated and efficient solution for transporting bulk powders in various industrial applications. By leveraging the principles of pneumatic transport, these systems offer reliable, safe, and scalable material handling capabilities. As industries continue to seek more efficient and sustainable operations, the demand for advanced powder handling technologies is expected to grow. HeadPowder, with its expertise in designing and implementing such systems, remains at the forefront of providing tailored solutions that meet the specific needs of its clients. The integration of continuous material handling systems into industrial processes not only enhances operational efficiency but also contributes to overall productivity and cost savings, making them an essential component in modern manufacturing and processing environments.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top