Bottom-discharge powder conveying systems represent a critical component in the industrial handling of bulk materials, particularly in sectors such as chemical, food, and pharmaceutical manufacturing. These systems are engineered to efficiently transport powders and granules from storage silos or hoppers to processing equipment, ensuring a continuous and controlled flow of material. Understanding the core components and design principles of such systems is essential for optimizing operational efficiency and maintaining product integrity.
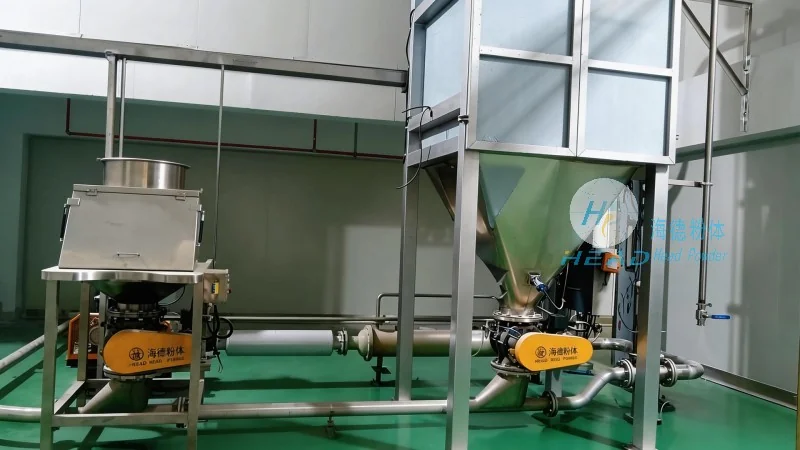
The bottom-discharge system typically consists of several interconnected parts that work in harmony to achieve reliable material transfer. The primary components include a hopper or silo for material storage, a discharge valve at the bottom of the container, a conveyor mechanism (often a screw or pneumatic system), and control systems for regulating flow rates. The hopper is designed with a conical or rectangular base to facilitate gravity-assisted discharge, while the discharge valve, such as a rotary valve or gate valve, controls the release of material into the conveyor. The conveyor system, which may be a screw conveyor or a pneumatic duct, transports the material to the next stage of processing. Control systems, including sensors and automation, monitor and adjust the flow to prevent issues like clogging or overfilling.
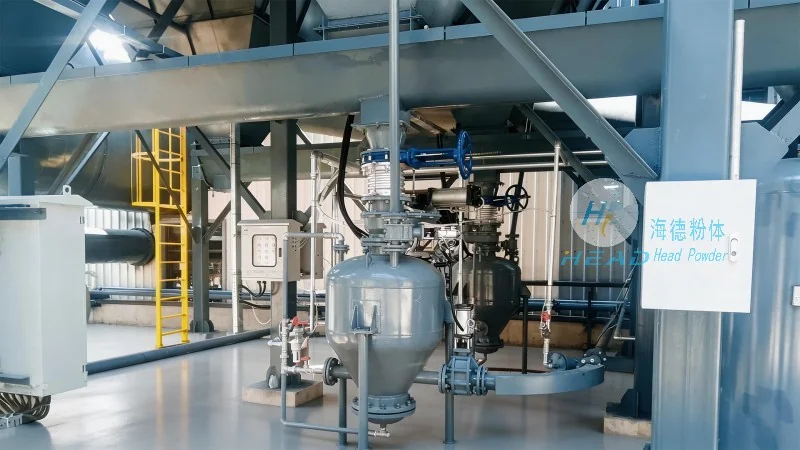
The design of a bottom-discharge powder conveying system is guided by several key principles aimed at maximizing efficiency, safety, and reliability. One of the fundamental principles is the use of gravity to assist in material flow, reducing the need for excessive mechanical energy. The system is often designed with a sloped hopper or a conical shape to allow powders to move smoothly towards the discharge point. Another critical principle is the prevention of material bridging or caking, which can occur in silos due to moisture or particle size variations. This is achieved through the use of agitators or vibrators integrated into the hopper to break up clumps and ensure uniform flow. Additionally, the system incorporates dust control measures, such as sealed enclosures and filtration systems, to maintain a safe working environment and comply with environmental regulations. The design also considers the material's properties, including particle size, density, and flowability, to select the appropriate conveyor type and discharge mechanism. For example, cohesive powders may require a screw conveyor with variable speed control to prevent blockages, while free-flowing materials might benefit from a pneumatic system for faster transport.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and integration of advanced bottom-discharge powder conveying systems. With a focus on innovation and customer-specific solutions, the company leverages decades of industry experience to develop systems tailored to the unique needs of each client. The company's engineers work closely with clients to analyze material characteristics, process requirements, and operational constraints, ensuring that the final system meets both functional and regulatory standards. HeadPowder's bottom-discharge systems are built with high-quality materials, such as stainless steel and corrosion-resistant alloys, to withstand the demands of harsh industrial environments. The company also emphasizes energy efficiency, incorporating features like variable frequency drives (VFDs) to optimize motor usage and reduce operational costs. Furthermore, the systems are equipped with advanced monitoring and diagnostic tools, allowing for real-time performance tracking and predictive maintenance. This proactive approach helps clients minimize downtime and extend the lifespan of their equipment.
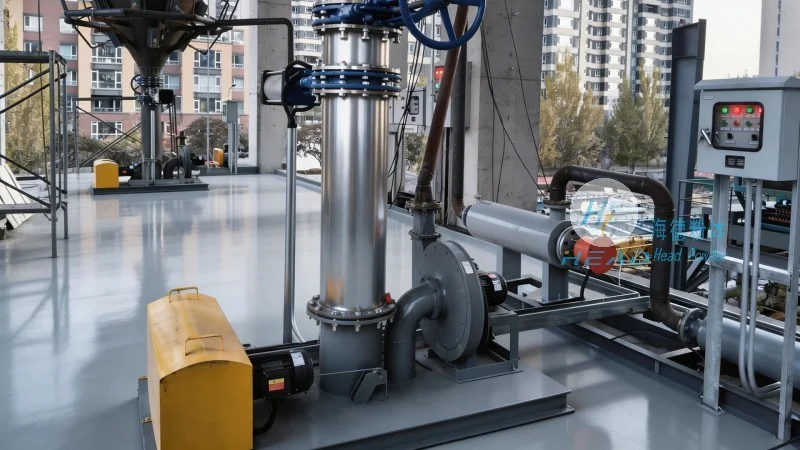
The versatility of bottom-discharge powder conveying systems makes them suitable for a wide range of applications across various industries. In the chemical industry, these systems are used to transport raw materials and finished products, ensuring a seamless transition from storage to processing. In the food and beverage sector, they are employed to handle ingredients like flour, sugar, and spices, maintaining hygiene and product quality. The pharmaceutical industry also relies on these systems for the safe and controlled transfer of active pharmaceutical ingredients (APIs) and excipients. The primary benefits of such systems include improved process reliability, reduced labor costs, and enhanced safety through automated material handling. By eliminating manual handling of powders, the risk of dust exposure and material contamination is significantly minimized. Additionally, the systems contribute to better inventory management by ensuring a consistent supply of materials to production lines, reducing the likelihood of production bottlenecks. The ability to integrate with existing facilities and adapt to changing production needs further enhances the value of bottom-discharge powder conveying systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top