HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for bulk powder handling. This article explores the fundamental principles behind sugar powder pneumatic conveying systems, along with the key working scene characteristics that define their application in industrial settings.
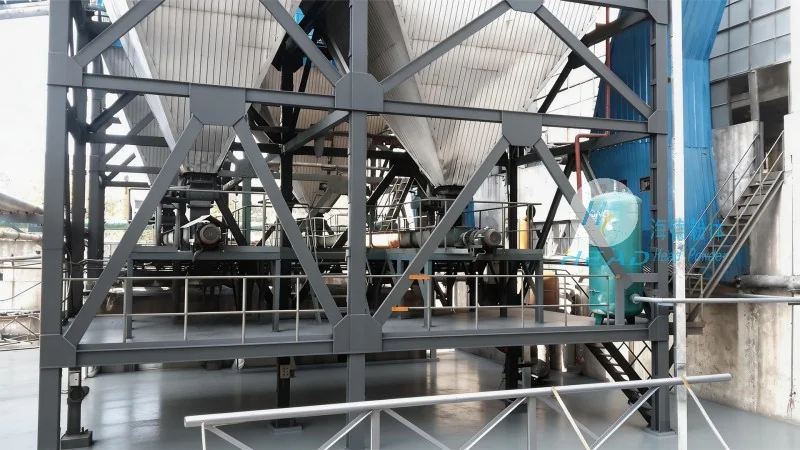
HeadPowder Engineering Co., Ltd. is a professional manufacturer and supplier of pneumatic conveying equipment. With a strong presence in the powder handling industry, the company leverages years of expertise to deliver customized solutions tailored to the unique needs of clients. HeadPowder’s headquarters is located in Shandong, China, where the company’s research and development team continuously innovates to enhance system efficiency and reliability.
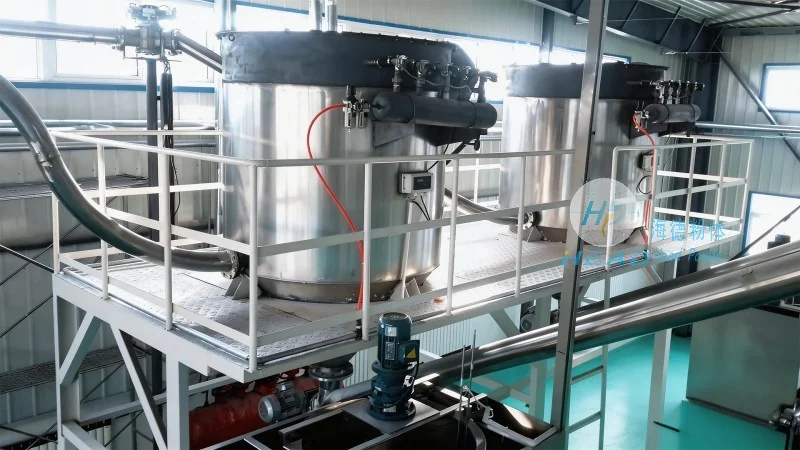
The core principle of pneumatic conveying systems involves the use of air or gas to transport bulk materials like sugar powder through a pipeline. In this process, the powder is suspended in the air stream, allowing it to be moved from one location to another without the need for mechanical components such as belts or buckets. The system typically operates by creating a pressure differential between the inlet and outlet of the pipeline, which propels the powder along the path of least resistance. For sugar powder, which is a fine, dry material, the selection of appropriate air velocity and pressure is critical to ensure efficient and low-loss transport. HeadPowder’s systems are engineered to maintain optimal air flow rates, minimizing particle degradation and ensuring consistent product quality throughout the conveying process.
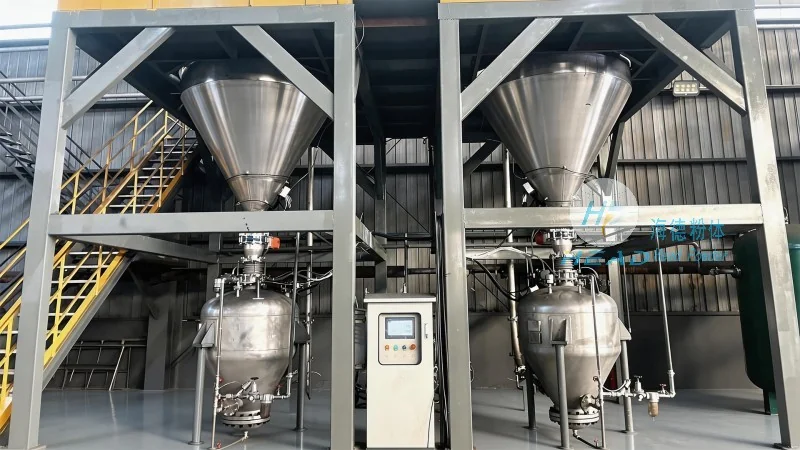
The application of sugar powder pneumatic conveying systems is characterized by several key factors that influence system design and performance. First, the system must handle the specific properties of sugar powder, including its particle size, moisture content, and flowability. Sugar powder is often used in food processing and pharmaceutical industries, where maintaining product purity and preventing contamination is paramount. HeadPowder’s systems are designed with sanitary and clean-in-place (CIP) features to meet the stringent requirements of these industries. Second, the working environment may involve multiple stages of material handling, such as from storage silos to processing equipment or packaging lines. The flexibility of pneumatic conveying allows for seamless integration into existing production lines, reducing downtime and improving operational efficiency. Third, the system’s ability to handle varying flow rates and material volumes is essential for adapting to different production demands. HeadPowder’s adjustable control systems enable precise regulation of air pressure and flow, ensuring consistent material delivery regardless of production fluctuations.
HeadPowder’s pneumatic conveying systems for sugar powder offer several advantages that make them a preferred choice in industrial applications. One of the primary benefits is the elimination of mechanical contact between the powder and system components, which reduces the risk of contamination and product degradation. The system’s enclosed design also minimizes dust emissions, improving workplace safety and compliance with environmental regulations. Additionally, pneumatic conveying systems are highly efficient in terms of energy consumption compared to traditional methods like bucket elevators or screw conveyors. By optimizing air velocity and pipeline design, HeadPowder’s systems achieve significant energy savings while maintaining high material throughput. Another advantage is the system’s adaptability to different production scales, from small-scale batch processing to large-scale continuous operations. HeadPowder’s modular design allows for easy expansion or modification of the system as production needs evolve.
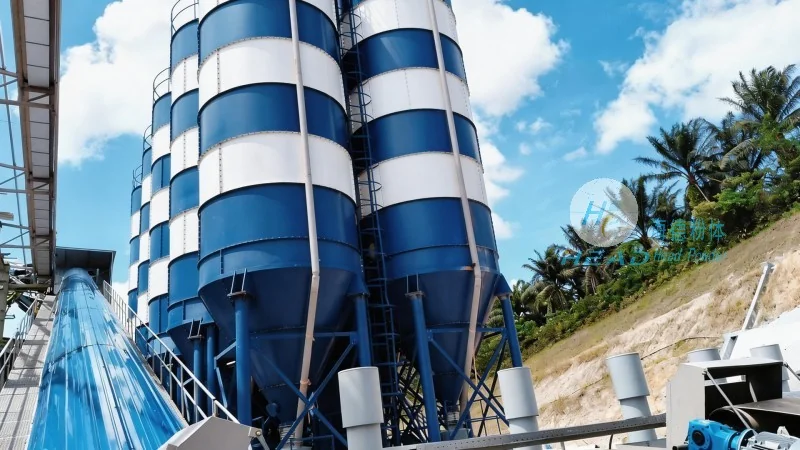
HeadPowder Engineering Co., Ltd. provides comprehensive solutions for sugar powder pneumatic conveying systems, combining advanced engineering principles with practical application expertise. By understanding the unique characteristics of sugar powder and the demands of industrial environments, HeadPowder delivers systems that enhance operational efficiency, ensure product quality, and meet regulatory standards. With a strong commitment to innovation and customer satisfaction, HeadPowder remains a trusted partner for businesses seeking reliable and efficient powder handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top