Efficient and reliable material handling is a critical aspect of modern industrial operations, particularly in processes involving fine powders like silica fume. The pneumatic conveying system for silica fume powder represents a sophisticated solution that ensures safe, efficient, and low-maintenance transport of this valuable material. This article explores the fundamental principles behind such systems and highlights the key characteristics of their operational scenarios, providing insights into how these technologies enhance industrial productivity.
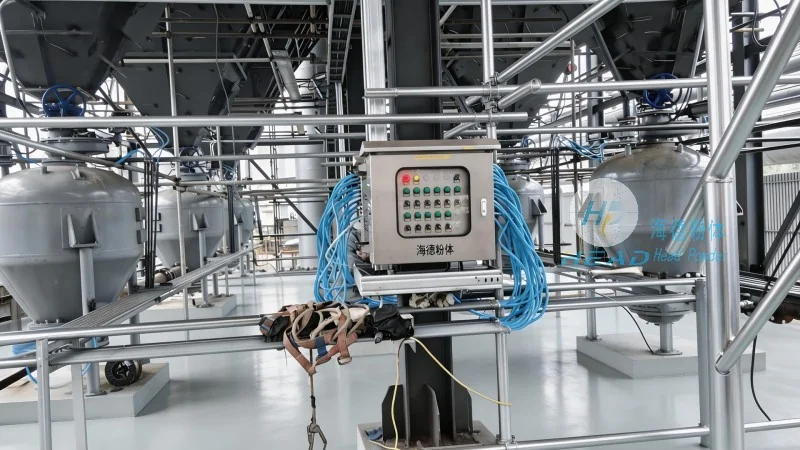
Silica fume, also known as microsilica, is a byproduct of silicon metal production or ferrosilicon alloys. It is a fine, highly reactive powder with a high surface area, making it an essential additive in concrete, mortar, and other construction materials. Handling this powder efficiently is crucial to maintain product quality and minimize operational risks. Pneumatic conveying systems offer a non-contact, closed-loop method for transporting silica fume, which is particularly advantageous in preventing dust contamination and ensuring environmental compliance.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of advanced material handling solutions. With a strong focus on innovation and customer-centric design, the company specializes in developing customized pneumatic conveying systems tailored to the unique needs of industrial applications. HeadPowder's expertise lies in integrating cutting-edge technology with robust engineering to deliver systems that meet the highest standards of performance, safety, and reliability. The company is headquartered in Shandong, China, and serves a diverse range of industries globally.
Pneumatic conveying systems operate on the principle of using air or gas to transport particulate materials through a pipeline. In the case of silica fume, the system typically employs either positive pressure (pressure conveying) or negative pressure (vacuum conveying) to move the material from the source to the destination. The choice between these methods depends on factors such as the distance of transport, the volume of material, and the required flow rate. Positive pressure systems use a blower to generate air pressure, pushing the material through the pipeline, while negative pressure systems use a vacuum pump to draw the material into the system.
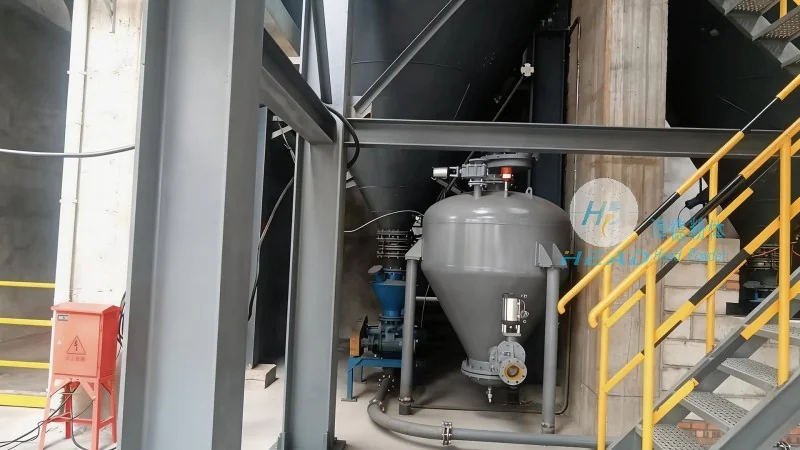
Key components of a silica fume pneumatic conveying system include the hopper (for material storage and feeding), the conveyor line (with appropriate pipe diameter and material), the air mover (blower or vacuum pump), and the control system (for regulating pressure and flow). The design of these components is critical to ensure efficient and consistent material transport. For example, the hopper is often equipped with a rotary valve or a feeder to control the flow rate, preventing blockages and maintaining a steady supply of material. The conveyor line is typically made of stainless steel or other corrosion-resistant materials to handle the abrasive nature of silica fume and to prevent material buildup.
The operational scenarios for silica fume pneumatic conveying systems vary widely based on the specific industrial application. In construction and building materials manufacturing, these systems are commonly used to transport silica fume from storage silos to batching plants or mixing stations. The systems are designed to handle high volumes of material with minimal downtime, ensuring that production lines remain operational. In the chemical and pharmaceutical industries, the systems may be used to transport silica fume for use as a filler or additive in various products, where precision and cleanliness are paramount.
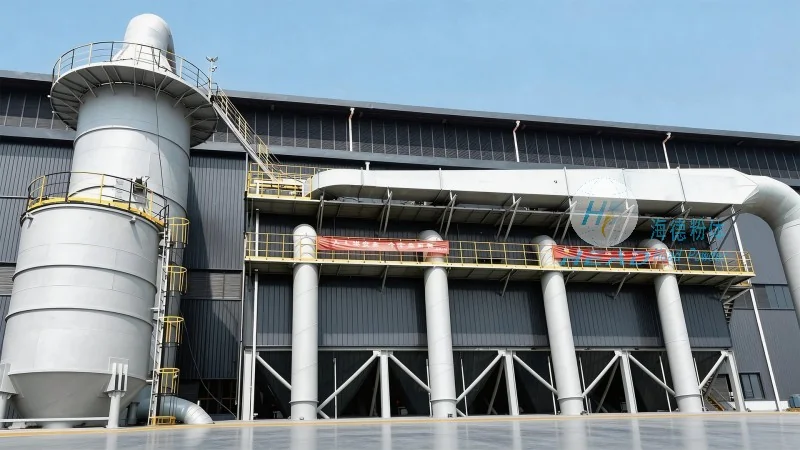
In the cement and concrete production sector, the systems play a vital role in integrating silica fume into the manufacturing process. The ability to convey the fine powder accurately and consistently is essential for maintaining the quality of the final product. Additionally, in the mining and mineral processing industries, silica fume may be used as a byproduct or a raw material, and pneumatic conveying systems help in the efficient transport of this material between processing stages. The versatility of these systems allows them to adapt to different operational environments, from indoor manufacturing facilities to outdoor storage and transfer points.
Implementing a pneumatic conveying system for silica fume offers several advantages over traditional methods like bucket elevators or belt conveyors. One of the primary benefits is the reduction in dust generation and contamination, as the material is contained within a closed system. This not only improves workplace safety but also ensures that the product remains free from external contaminants, which is critical for high-quality applications. Additionally, pneumatic conveying systems are generally more energy-efficient compared to mechanical systems, as they require less power to move the material over long distances.
However, the design and operation of these systems require careful consideration of several factors. The particle size and density of silica fume can affect the system's performance, as finer particles may require higher air velocities to maintain flow. The system must also be designed to handle the abrasive nature of the material, which can lead to wear and tear on components if not properly protected. Regular maintenance and monitoring are essential to ensure the longevity and efficiency of the system. HeadPowder's expertise in system design and engineering helps in addressing these challenges, providing customized solutions that optimize performance and minimize operational costs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top