HeadPowder, a leading engineering company based in Shandong, China, specializes in the application and optimization of pneumatic conveying technology for the efficient handling of carbon black and coal powder. This article explores the critical role of pneumatic conveying systems in modern material transport, focusing on how advanced design principles enhance performance, safety, and operational efficiency in industrial settings.
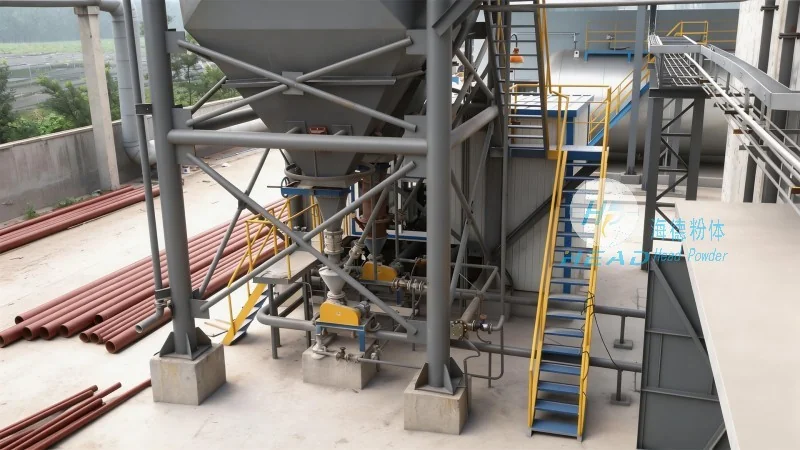
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials through a pipeline using compressed air or other gases. This technology is particularly advantageous for handling fine powders like carbon black and coal powder, which are prone to dust generation and require precise control during transport. The core components of a pneumatic conveying system typically include a material feeder, a conveying line, a separator, and a dust collection system. Each component is meticulously designed to ensure optimal flow, minimize material degradation, and maintain environmental compliance.
Carbon black and coal powder are essential raw materials in various industries, including rubber, plastics, and energy production. Their handling requires specialized equipment to prevent agglomeration, dust explosion risks, and material loss. Pneumatic conveying systems offer a solution by providing a closed-loop transport process that isolates the material from the environment, reducing exposure to contaminants and improving product quality. For instance, in rubber manufacturing, carbon black is often conveyed from storage silos to mixing equipment, where precise dosing is critical for product consistency. Similarly, coal powder is transported to power plants or industrial furnaces, where uniform distribution is vital for combustion efficiency.
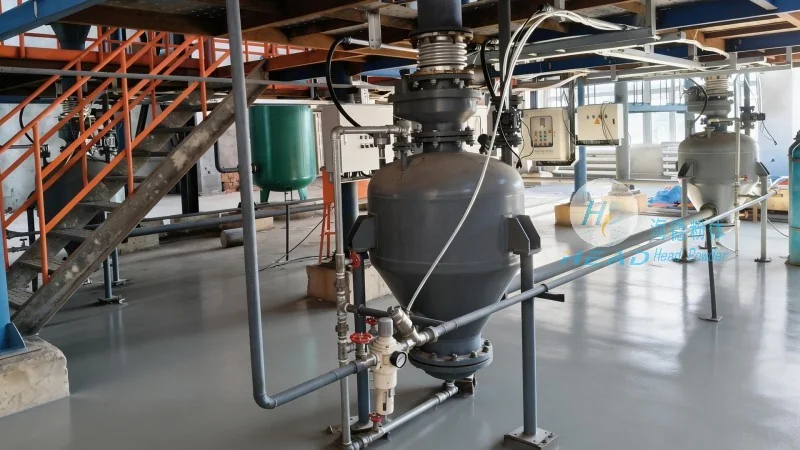
Optimizing pneumatic conveying systems involves several key strategies aimed at improving throughput, reducing energy consumption, and minimizing maintenance costs. One critical approach is the selection of appropriate air velocities and pipeline diameters. Higher air velocities can increase conveying capacity but may lead to increased energy use and higher wear on components. Conversely, lower velocities reduce energy consumption but may require larger pipelines to maintain flow. Engineers at HeadPowder conduct detailed flow calculations and material property analyses to determine the optimal air velocity and pipeline dimensions for each application.
Another optimization technique is the use of advanced material feeders, such as rotary valves or screw feeders, which ensure consistent material flow into the conveying line. These feeders help prevent blockages and maintain a steady flow rate, which is crucial for maintaining system efficiency. Additionally, the integration of dust collection systems, such as bag filters or cyclones, is essential for controlling emissions and protecting personnel from airborne particles. HeadPowder's engineers design these systems to meet stringent environmental regulations while ensuring minimal pressure drop, which helps maintain the overall efficiency of the conveying process.
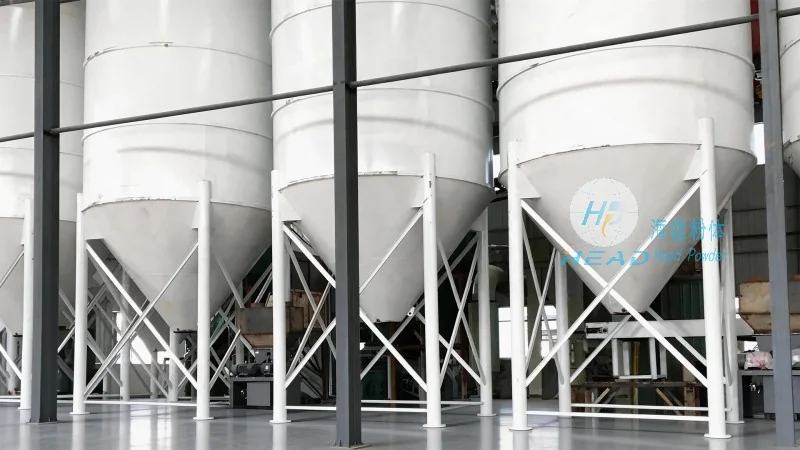
HeadPowder has successfully implemented pneumatic conveying solutions for numerous clients in the carbon black and coal powder industries. For example, a major rubber manufacturer in China relied on HeadPowder to upgrade its carbon black handling system, resulting in a 20% increase in conveying capacity and a 15% reduction in energy consumption. The system was designed with a high-efficiency rotary valve and a custom-designed pipeline layout that minimized pressure losses. Another client, a coal-fired power plant, implemented a pneumatic conveying system to transport coal from storage to the boiler, reducing material loss by 30% and improving combustion efficiency by 5%.
Pneumatic conveying technology remains a cornerstone of efficient material handling in the carbon black and coal powder industries. As industrial demands for higher productivity and lower environmental impact continue to grow, companies like HeadPowder are at the forefront of developing innovative solutions that optimize system performance. By leveraging advanced engineering principles and tailored design approaches, HeadPowder ensures that its clients achieve reliable, cost-effective, and environmentally compliant material transport solutions. The future of pneumatic conveying lies in further integration with automation and digital monitoring systems, which will enable real-time optimization and predictive maintenance, further enhancing operational efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top