HeadPowder, a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems tailored for cement tank trucks. Based in Shandong, China, the company leverages decades of industry expertise to deliver efficient and reliable solutions that meet the demanding requirements of modern construction and material transportation.
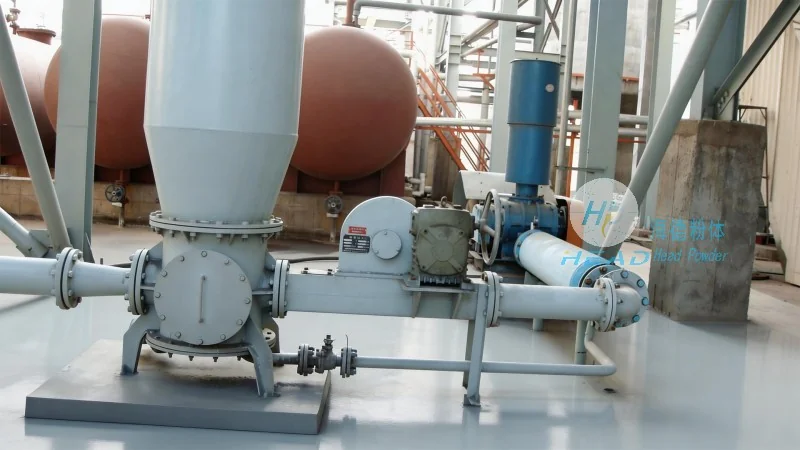
The powder pneumatic conveying system for cement tank trucks operates on the fundamental principle of using compressed air to transport bulk powders, such as cement, from a storage silo to the truck's tank. This method eliminates the need for mechanical components like conveyor belts or buckets, reducing maintenance costs and enhancing safety. The system typically consists of several key components: a silo or hopper for material storage, a rotary valve to control the flow of powder, a pipeline network, a compressor to generate the necessary air pressure, and a dust collector to capture and filter airborne particles. The rotary valve, often a star valve or slide valve, regulates the quantity of material released into the pipeline, ensuring a consistent flow rate. The compressor, usually an industrial-grade unit, supplies the high-pressure air that propels the powder through the pipeline. The pipeline itself is constructed from durable materials like stainless steel or coated steel to withstand the abrasive nature of cement and prevent leakage. The dust collector, equipped with filters and a fan, captures any fine particles that escape during the conveying process, ensuring compliance with environmental regulations and maintaining a clean working environment.
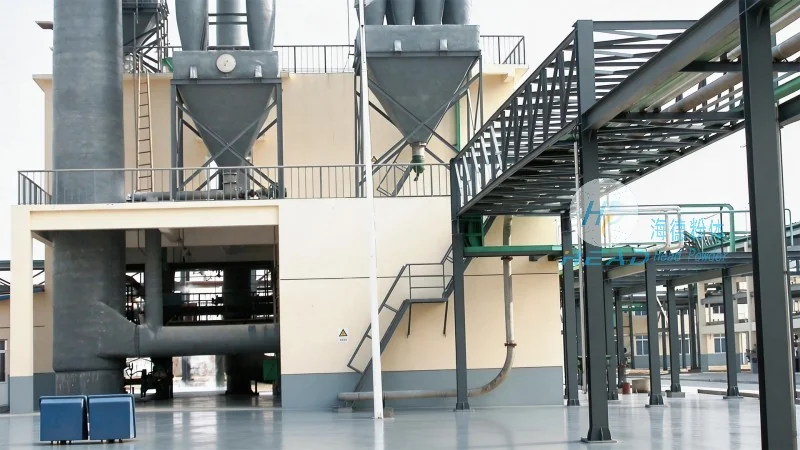
The working scene characteristics of the pneumatic conveying system for cement tank trucks are defined by its adaptability to various operational environments and its ability to enhance workflow efficiency. One of the primary advantages is the system's ability to handle long-distance transportation without the need for intermediate storage or manual handling. This is particularly beneficial in construction sites where multiple locations require cement delivery, as it allows for continuous operation and reduces downtime. The system's flexibility also enables it to operate in both indoor and outdoor settings, making it suitable for a wide range of applications, from large-scale industrial projects to smaller construction sites. Additionally, the system's low maintenance requirements contribute to its cost-effectiveness, as it minimizes the need for frequent repairs and replacements. The ability to adjust the conveying rate through the rotary valve allows operators to match the flow with the truck's loading capacity, preventing overfilling or underfilling and ensuring precise material delivery. The dust control measures, including the dust collector and sealed pipelines, also enhance safety by reducing the risk of respiratory issues and other health hazards associated with handling loose cement particles.
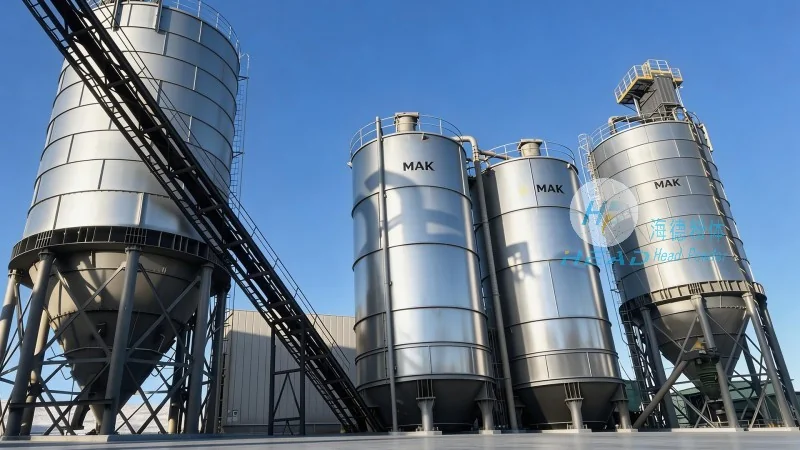
The pneumatic conveying system for cement tank trucks is widely used in scenarios where efficient and safe material handling is critical. In large construction projects, such as the development of residential complexes, commercial buildings, or infrastructure like highways and bridges, the system ensures a steady supply of cement to the job site, supporting continuous construction activities. The system's ability to handle high volumes of material in a short period makes it ideal for meeting tight project deadlines. In industrial settings, such as cement plants or concrete mixing facilities, the system facilitates the transfer of raw materials or finished products between different stages of production, improving overall operational efficiency. The system's adaptability also makes it suitable for remote or challenging locations, where traditional conveyor systems may not be feasible due to terrain or space constraints. The operational benefits of the system extend beyond efficiency, as it also contributes to environmental sustainability by reducing the amount of dust and emissions released into the air. The sealed pipelines and dust collector help minimize the environmental impact, making the system a more eco-friendly option compared to traditional methods. Furthermore, the system's reliability and low downtime contribute to cost savings for businesses, as it reduces the need for additional labor or equipment to handle material transportation.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top