HeadPowder, a leading provider of material handling solutions, specializes in the design and implementation of pneumatic conveying systems for various industrial powders, including bakelite powder. This article explores the fundamental working principle and key characteristics of pneumatic conveying systems tailored for bakelite powder material, offering insights into how these systems efficiently transport the material while maintaining operational efficiency and safety standards.
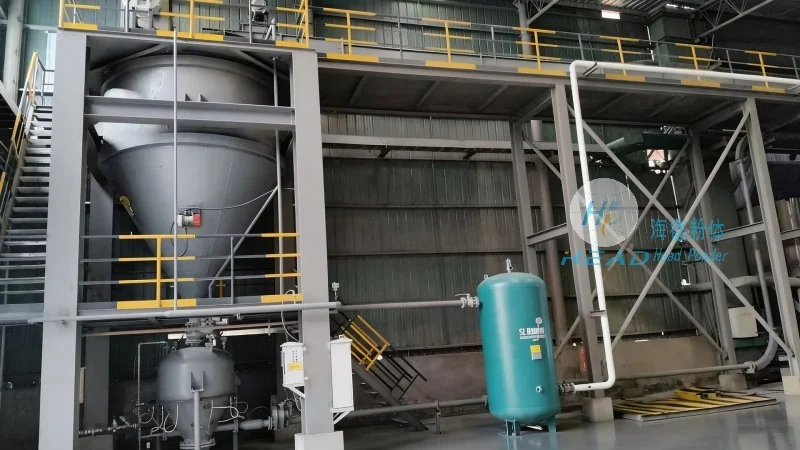
Pneumatic conveying for bakelite powder operates on the principle of using compressed air or other gases to transport the powder through a pipeline system. The process typically involves a combination of air flow and pressure differentials to move the material from the source to the destination. There are two primary types of pneumatic conveying systems: suction (or vacuum) systems and pressure systems. Suction systems use a vacuum to draw the powder from the source, while pressure systems use compressed air to push the material through the pipeline. For bakelite powder, which is often fine and abrasive, the choice of system depends on factors such as the distance of transport, the required flow rate, and the material's properties. The working principle can be broken down into several key steps. First, the bakelite powder is introduced into the conveying line, either by a hopper or a feeder. Then, the air is introduced into the line, creating a flow that entrains the powder particles. The air-powder mixture travels through the pipeline, and the powder is separated from the air at the discharge point. The air may be filtered and recycled, while the powder is collected in a receiving hopper or container. This process ensures a continuous and efficient flow of bakelite powder, minimizing the risk of material degradation or loss.
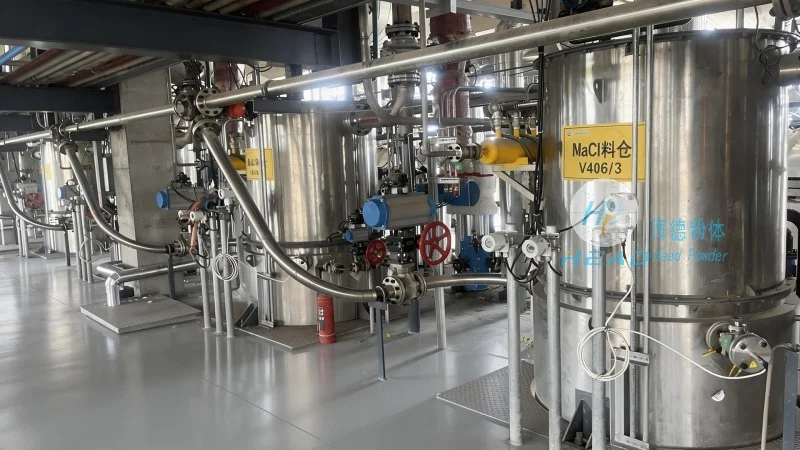
The pneumatic conveying systems designed for bakelite powder exhibit several distinct characteristics that make them suitable for industrial applications. One of the most significant advantages is the ability to achieve fully enclosed and dust-free operation. Unlike traditional bulk handling methods, such as bucket elevators or screw conveyors, pneumatic conveying systems keep the material contained within the pipeline, preventing dust emissions and protecting the environment. This is particularly important for bakelite powder, which can be fine and generate significant dust during handling. Another key characteristic is the high efficiency in material transport. Pneumatic systems can handle large volumes of bakelite powder at high flow rates, reducing the time and labor required for material transfer. The systems are also highly adaptable, as they can be configured to handle different particle sizes, moisture contents, and flow rates. This flexibility allows for customization based on specific production requirements. Additionally, pneumatic conveying systems offer improved safety and hygiene. By keeping the material enclosed, the risk of contamination from external sources is minimized, and the system reduces the need for manual handling, which can be hazardous, especially with fine powders. The systems also contribute to energy efficiency, as they can be optimized to use the minimum amount of air required for effective transport, reducing operational costs over time.
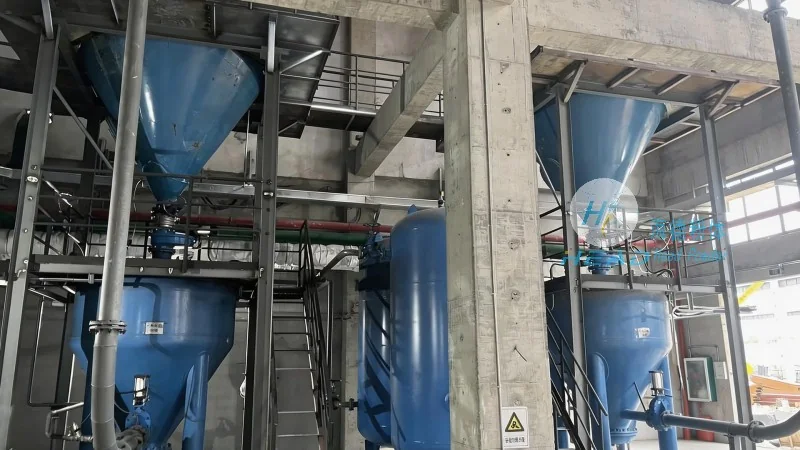
The pneumatic conveying systems for bakelite powder are widely used in various industrial sectors, including manufacturing, chemical processing, and material processing. In these applications, the systems are essential for the efficient transfer of bakelite powder from storage silos to processing equipment, such as mixers, extruders, or molding machines. The benefits of using these systems extend beyond material handling efficiency. For example, in the production of bakelite products, such as electrical components or industrial parts, the consistent and reliable supply of powder is crucial for maintaining product quality and production throughput. The enclosed nature of the system also helps in maintaining a clean and safe working environment, which is critical for compliance with occupational health and safety regulations. Furthermore, the systems contribute to cost savings by reducing material loss and minimizing the need for additional cleaning and maintenance due to dust accumulation. The adaptability of the systems allows them to be integrated into existing production lines without major modifications, making them a cost-effective solution for upgrading material handling processes.
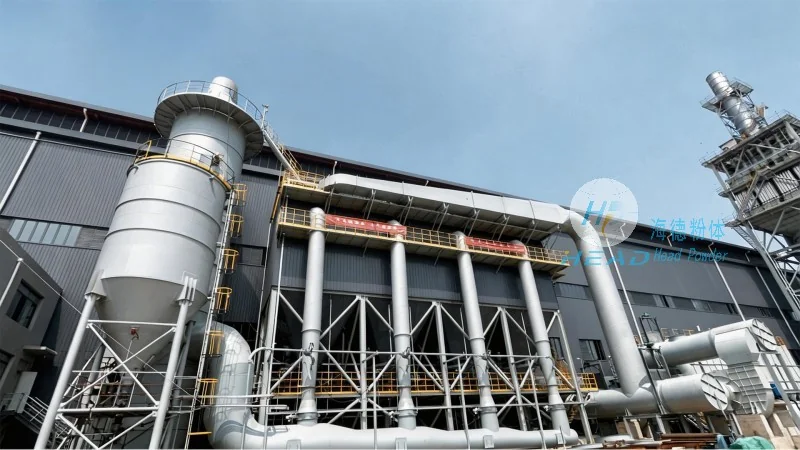
HeadPowder Engineering, based in Shandong, China, is a trusted partner in providing advanced pneumatic conveying solutions for bakelite powder and other industrial materials. With a focus on innovation and customer satisfaction, the company designs and manufactures systems that meet the specific needs of its clients. The working principle and characteristics of pneumatic conveying for bakelite powder, as outlined above, demonstrate the effectiveness of these systems in improving operational efficiency, safety, and environmental compliance. By leveraging the expertise of HeadPowder, industries can enhance their material handling processes, ensuring smooth and reliable production of bakelite products. The company's commitment to quality and customer service makes it a leading choice for businesses seeking reliable and efficient pneumatic conveying solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top