Light calcium carbonate is a widely used industrial material, and its efficient handling and transportation are crucial for production processes. The pneumatic conveying system offers a reliable solution for moving this material, ensuring safety, efficiency, and minimal environmental impact. This article explores the fundamental principles behind such a system, focusing on the technical aspects and operational considerations.
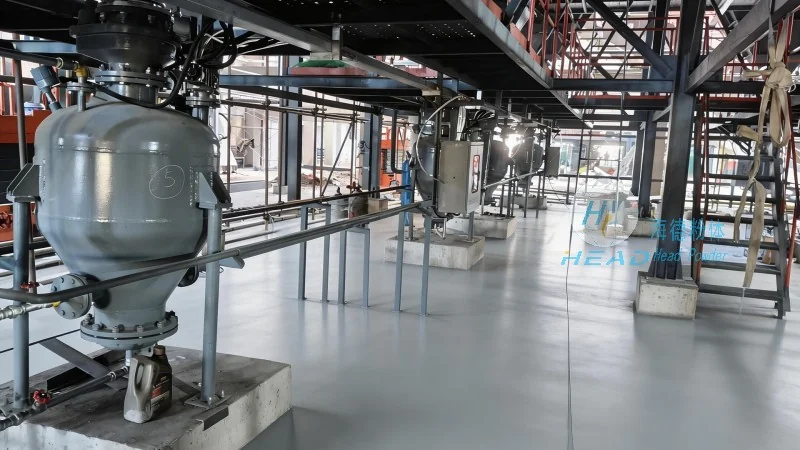
Pneumatic conveying systems utilize air or other gases to transport bulk materials like light calcium carbonate through a network of pipes. This method is preferred over traditional mechanical conveyors in many applications due to its ability to handle fine powders without the need for moving parts that might cause clogging or material degradation. The system typically consists of a material feed hopper, a conveyor line, and a receiver or discharge point. The air flow is controlled to create a pressure differential that propels the material through the system.
The effectiveness of a pneumatic conveying system for light calcium carbonate depends on several critical components. The material feed hopper is designed to store and feed the powder into the system at a controlled rate. This component often includes a feeder, such as a rotary valve or a screw feeder, to regulate the flow and prevent blockages. The conveyor line itself is made of materials resistant to the chemical properties of calcium carbonate, such as stainless steel or special coatings, to ensure durability and prevent corrosion. The air compressor or blower provides the necessary pressure and volume of air to move the material. The system may also include filters and cyclones to separate the material from the air at the discharge point, ensuring clean air release and material recovery.
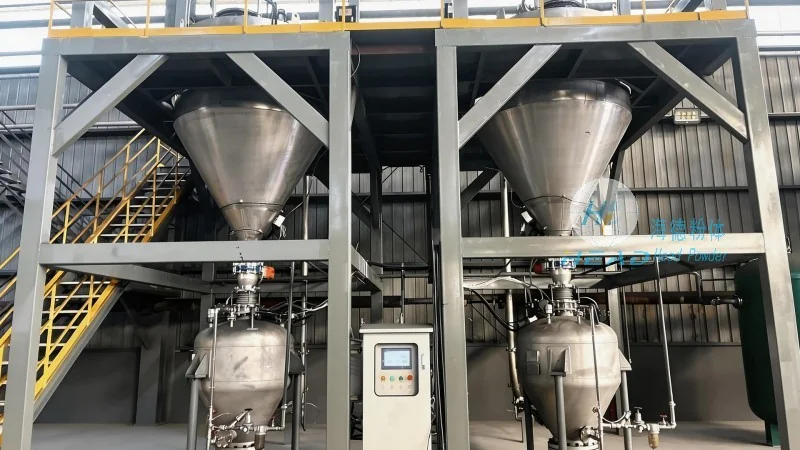
The operation of the pneumatic conveying system for light calcium carbonate involves several stages. First, the material is fed from the hopper into the conveyor line. The air compressor then generates a high-pressure air stream that flows through the line. As the air moves, it entrains the calcium carbonate particles, creating a slurry-like mixture. This mixture travels through the pipes to the discharge point. At the receiver, a cyclone or filter separates the material from the air. The air is then released, while the calcium carbonate is collected in a container. The system's efficiency depends on the air velocity, which must be sufficient to keep the particles suspended but not so high as to cause excessive wear on the equipment or energy waste.
Implementing a pneumatic conveying system for light calcium carbonate offers several advantages over traditional methods. One key benefit is the reduction in material handling time and labor costs. The system can transport large quantities of material over long distances with minimal human intervention. Additionally, it provides a cleaner and safer working environment by containing dust and preventing material spillage. The system also allows for better control over the material flow rate, ensuring consistent production rates. Furthermore, it can be integrated with other processing equipment, such as mixing or packaging systems, to create a seamless production line. The use of pneumatic conveying also minimizes product contamination, which is critical for light calcium carbonate used in food, pharmaceutical, or cosmetic applications.
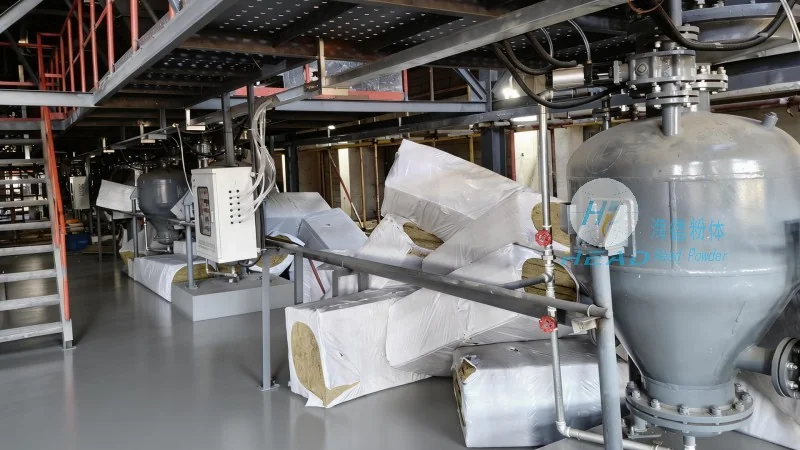
Proper operation and maintenance are essential for the longevity and efficiency of a light calcium carbonate pneumatic conveying system. Regular cleaning of the conveyor lines and filters is necessary to prevent clogging and maintain air flow. The air compressor should be checked for proper pressure and air quality to avoid contamination of the material. The feeder components should be inspected for wear and tear, and replaced as needed to ensure consistent material flow. Additionally, monitoring the system's performance, such as air pressure and material flow rate, helps identify potential issues before they lead to system failure. By following these operational guidelines, the system can operate at optimal levels, ensuring reliable and efficient transportation of light calcium carbonate.
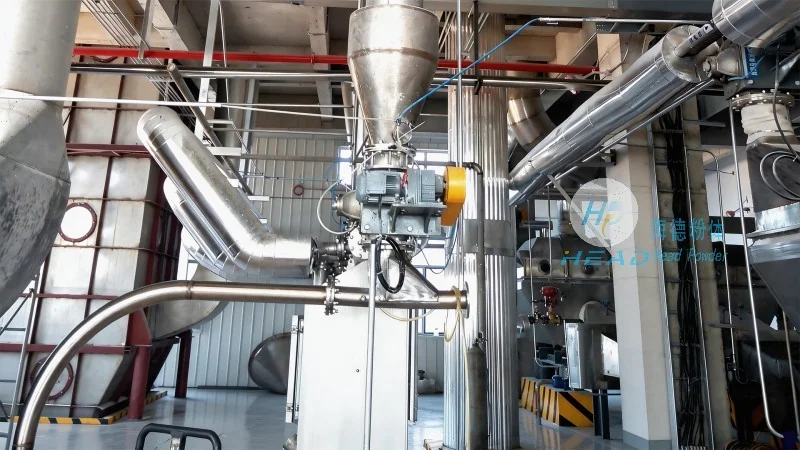
The light calcium carbonate pneumatic conveying system is widely used in various industrial applications. In the food and beverage industry, it is used to transport calcium carbonate as an anti-caking agent or filler in products like baking powder and beverages. In the pharmaceutical industry, it is used to transport the material for use in tablets and capsules, where purity and consistency are critical. In the cosmetic industry, it is used as a filler in creams and powders, requiring a clean and efficient conveying system to maintain product quality. In the construction industry, it is used as a filler in paints and coatings, where the system's ability to handle fine powders without clogging is essential. These applications highlight the versatility and importance of the pneumatic conveying system in handling light calcium carbonate efficiently and safely.
The pneumatic conveying system for light calcium carbonate is a sophisticated and effective method for material transportation. By understanding the principles and components of the system, industries can optimize their production processes, improve efficiency, and ensure the quality of their products. The system's advantages, such as reduced labor costs, improved safety, and better material control, make it a preferred choice for many applications. With proper maintenance and operation, the system can provide reliable and long-term service, contributing to the overall success of industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top