Pneumatic conveying technology plays a vital role in the efficient handling of food materials within processing facilities. This article examines the fundamental working principles of pneumatic conveying systems and highlights their key characteristics, with a focus on how these technologies optimize material transport while maintaining food safety standards. The discussion also includes practical applications and insights into the specialized solutions offered by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field.
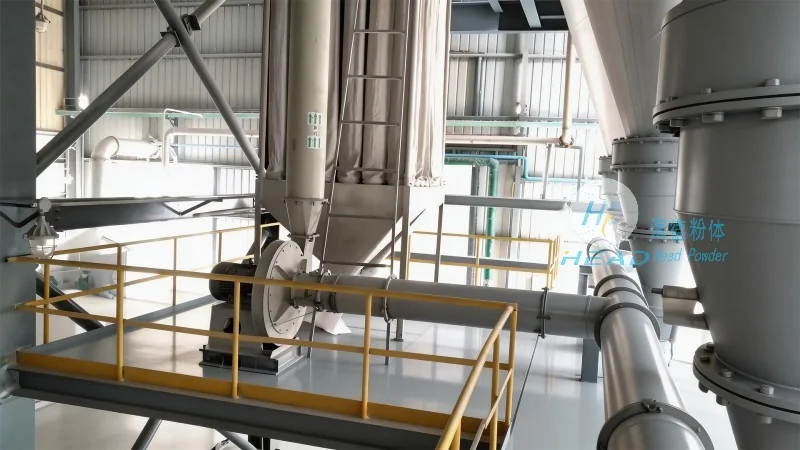
Pneumatic conveying operates by using compressed air or gas to transport bulk materials, such as powders and granules, through a sealed pipeline network. The process typically employs two primary methods: suction (vacuum) conveying and pressure conveying. In suction conveying, a vacuum is created at the material inlet to draw the product into the pipeline, while pressure conveying utilizes compressed air to push the material forward. For food materials, which often require delicate handling and strict hygiene, the system design must prioritize minimal product degradation and contamination prevention. The conveying process begins with the material being introduced into a hopper or inlet, where it is then accelerated by the airflow and transported through the pipeline to the discharge point. The velocity and pressure of the air are meticulously controlled to ensure the material moves efficiently without causing clogging or damage to the product. This mechanism allows for a continuous, enclosed transport of food items, reducing exposure to external contaminants and maintaining the integrity of the material.
Pneumatic conveying systems for food applications exhibit several defining characteristics that make them superior to traditional mechanical conveyors. Firstly, they provide a fully enclosed and sanitary design, which is critical for meeting food safety regulations. Unlike open systems that may introduce dust or contaminants, pneumatic pipelines keep the material contained, minimizing the risk of cross-contamination and ensuring compliance with industry standards. Secondly, these systems offer high flexibility in terms of layout and routing. The pipeline can be arranged in various configurations, including vertical, horizontal, or inclined paths, allowing for complex material flow patterns without the need for multiple transfer points. This flexibility is particularly valuable in food processing facilities where space is limited or where the production line requires integration with multiple processing stages. Thirdly, pneumatic conveying enables precise control over the material flow rate and pressure. By adjusting the air volume and pressure, operators can regulate the speed of material transport, ensuring consistent delivery to downstream processes. This control capability is essential for maintaining production efficiency and preventing bottlenecks in the manufacturing line. Additionally, the system's ability to handle a wide range of food materials, from fine powders like flour to larger granules like sugar or nuts, makes it a versatile solution for diverse food processing needs. The gentle handling of materials also minimizes product degradation, preserving the quality and integrity of the food items being conveyed.
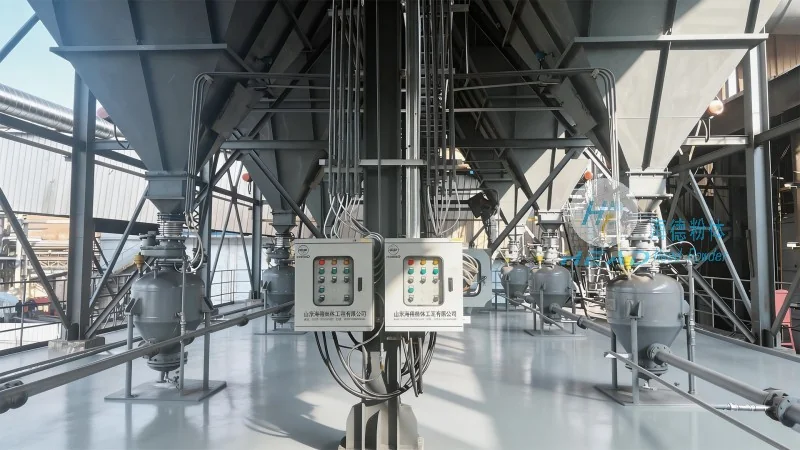
Pneumatic conveying is widely utilized across various segments of the food industry due to its adaptability and efficiency. In flour mills, for example, pneumatic systems are employed to transport raw wheat, milled flour, and other grain products between processing stages. The enclosed pipeline design prevents dust and flour from contaminating the environment, while the gentle conveying action preserves the quality of the flour. Similarly, in sugar processing plants, pneumatic conveying is used to move granulated sugar from storage silos to mixing and packaging areas. The system's ability to handle high volumes of granular materials at a controlled speed ensures smooth operation and reduces the risk of clogging. For snack food manufacturers, pneumatic conveying is essential for transporting ingredients like nuts, seeds, and dried fruits, which are often delicate and require careful handling to avoid breakage. The system's flexibility allows for integration with other processing equipment, such as mixers and ovens, enabling seamless material flow from raw ingredient to finished product. Additionally, in the production of dairy products, pneumatic conveying is used to transport powdered milk and other dairy ingredients, ensuring that the materials are handled hygienically and efficiently. The enclosed system prevents moisture and contaminants from entering the product, maintaining the quality and safety of the dairy items.
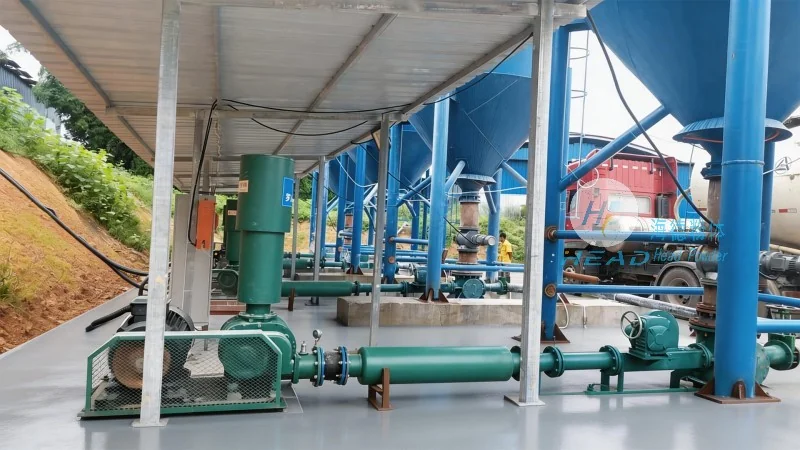
Shandong HeadPowder Engineering Co., Ltd. is a prominent provider of pneumatic conveying solutions tailored for the food processing industry. With a focus on innovation and compliance, the company specializes in designing and manufacturing systems that meet the stringent requirements of food safety regulations. HeadPowder's expertise lies in creating customized pneumatic conveying systems that address the unique challenges of food materials, such as maintaining hygiene, preventing product degradation, and ensuring efficient material flow. The company's products are engineered with high-quality materials, including stainless steel and food-grade components, to ensure durability and long-term performance. HeadPowder's team of engineers and technicians work closely with clients to understand their specific needs and develop tailored solutions that enhance productivity and reduce operational costs. The company's commitment to quality and customer satisfaction has made it a trusted partner for food processing facilities across China and beyond.
HeadPowder is located in Shandong, China, providing a strategic base for serving the domestic and international food processing markets. The company's address is in Shandong, China, and it operates with a focus on delivering reliable and efficient pneumatic conveying systems that meet the evolving needs of the food industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top