Pharmaceutical bulk material pneumatic conveying is a critical technology in the pharmaceutical industry, designed to transport powders and granules safely and efficiently. This method leverages the principles of fluid dynamics to move materials through a closed system, ensuring compliance with stringent regulatory standards. The process involves the use of air or other gases to transport bulk materials from one location to another, often within a pharmaceutical manufacturing facility. Understanding the working principle and key characteristics of such systems is essential for optimizing production processes and maintaining product quality.
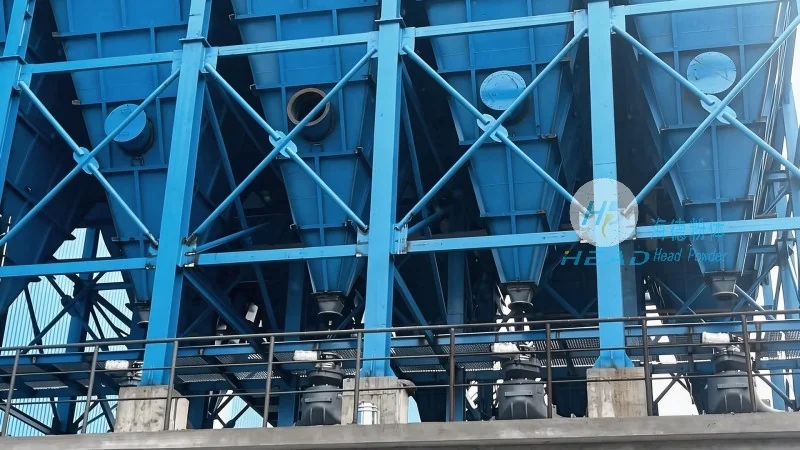
HeadPowder, a division of Shandong HeadPowder Engineering Co., Ltd., specializes in the design, manufacturing, and integration of advanced pneumatic conveying systems tailored for the pharmaceutical sector. With a focus on precision, reliability, and regulatory compliance, HeadPowder provides customized solutions that meet the unique demands of pharmaceutical production. The company is headquartered in Shandong, China, and has established itself as a leading provider of high-quality pneumatic conveying equipment for the global pharmaceutical industry.
The core working principle of pharmaceutical pneumatic conveying systems revolves around the movement of bulk materials using air or gas as the conveying medium. There are two primary types of pneumatic conveying systems: positive pressure and negative pressure. Positive pressure systems operate by blowing air into the conveying line, creating a pressure higher than the ambient environment, which propels the material forward. Negative pressure systems, on the other hand, create a vacuum in the line, drawing the material into the system. In pharmaceutical applications, both systems are used depending on the specific requirements of the material being conveyed, such as particle size, moisture content, and the need for contamination control.
During the conveying process, the bulk material is introduced into the conveying line at a controlled rate, often through a hopper or feeder. The material is then entrained by the moving air stream, which carries it through the pipeline to the destination point. The air velocity is carefully managed to ensure that the material particles are fully suspended and transported without causing blockages or degradation. This controlled environment minimizes the risk of product contamination and ensures consistent material flow. The system typically includes components such as a blower or vacuum pump, conveying lines, and a receiver or discharge unit, all of which work in tandem to achieve efficient material transport.
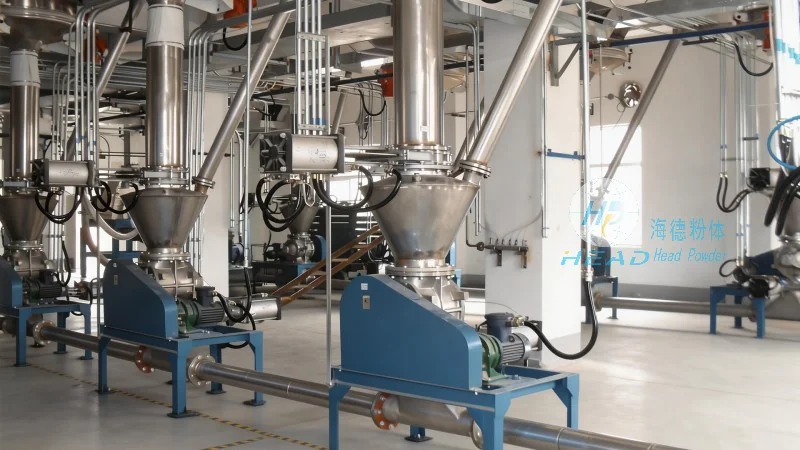
Pharmaceutical pneumatic conveying systems are characterized by several key features that make them ideal for handling sensitive and regulated materials. First, the systems are designed to be fully enclosed and airtight, preventing the release of dust or particles into the environment. This ensures compliance with environmental regulations and maintains a clean, controlled manufacturing environment. Second, the equipment is constructed from materials that are compatible with pharmaceutical products, such as stainless steel, which resists corrosion and prevents contamination. Third, the systems offer high levels of flexibility, allowing for the conveyance of various materials, including powders, granules, and even liquids, with minimal adjustments.
Another important characteristic is the ability to maintain a sterile or clean environment. Many pharmaceutical pneumatic conveying systems are equipped with filters and cleaning mechanisms that prevent the buildup of particles and ensure that the material remains free from contaminants. This is crucial for products that require strict quality control, such as active pharmaceutical ingredients (APIs) and finished dosage forms. Additionally, the systems are designed for easy maintenance and cleaning, with features like CIP (Clean-in-Place) and SIP (Sterilize-in-Place) capabilities, which help to maintain the integrity of the product and the system itself.
Pharmaceutical pneumatic conveying systems are widely used in various stages of pharmaceutical manufacturing, from raw material handling to final product packaging. They are particularly beneficial in processes where bulk materials need to be transported between different areas of a facility, such as from a warehouse to a production line or from a mixing area to a packaging station. The systems offer several advantages over traditional methods like belt conveyors or manual handling. These include improved safety, as the enclosed system prevents exposure to dust and hazardous materials, and enhanced efficiency, as the material can be transported quickly and with minimal labor.
Furthermore, the flexibility of pneumatic conveying allows for the integration of multiple materials or processes within a single system. For example, a system can be configured to transport different raw materials to a common mixing point, or to convey finished products from a production line to a storage area. This integration reduces the need for multiple handling steps and streamlines the overall production process. The systems also contribute to cost savings by minimizing material loss and reducing the need for additional equipment, such as elevators or elevators.
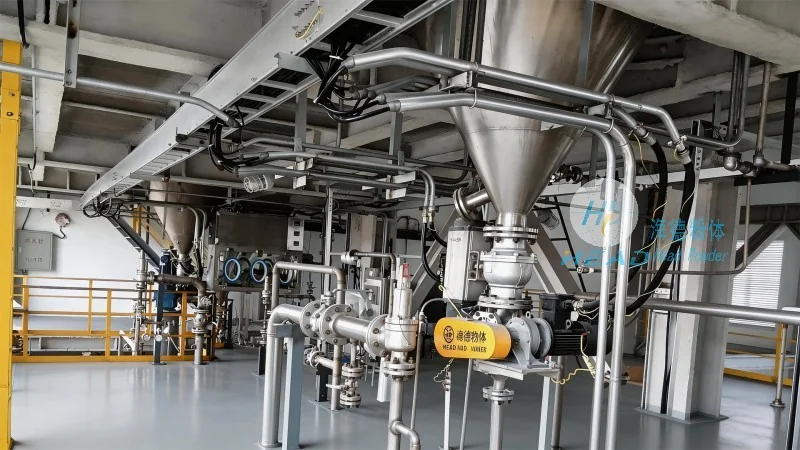
In the pharmaceutical industry, regulatory compliance is paramount, and pneumatic conveying systems must meet strict standards to ensure product safety and quality. HeadPowder's systems are designed and manufactured to comply with international regulations, including those from the FDA (U.S. Food and Drug Administration) and other regulatory bodies. The company adheres to GMP (Good Manufacturing Practice) guidelines, ensuring that all components and processes are validated and documented. This includes regular inspections, maintenance schedules, and quality control checks to ensure that the system operates within specified parameters.
The systems are also equipped with monitoring and control features that allow for real-time tracking of material flow and system performance. Sensors and indicators can detect issues such as blockages, pressure drops, or air leaks, enabling immediate intervention to prevent product contamination or system failure. This proactive approach to maintenance and monitoring helps to ensure consistent product quality and reduces downtime in the manufacturing process.
Pharmaceutical bulk material pneumatic conveying is a sophisticated and essential technology in modern pharmaceutical manufacturing. By understanding the working principle and key characteristics of these systems, pharmaceutical companies can optimize their production processes, enhance product quality, and ensure regulatory compliance. HeadPowder, with its expertise and commitment to quality, provides reliable pneumatic conveying solutions that meet the demanding requirements of the pharmaceutical industry. Whether for new installations or system upgrades, HeadPowder's systems offer a proven approach to efficient and safe material handling, supporting the continuous improvement of pharmaceutical production.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top