Multi-functional powder handling systems are advanced industrial solutions designed to efficiently transport, process, and manage various types of powders in different applications. These systems are engineered to meet the diverse needs of industries such as pharmaceuticals, food processing, chemicals, and manufacturing, ensuring reliable and safe material handling operations.
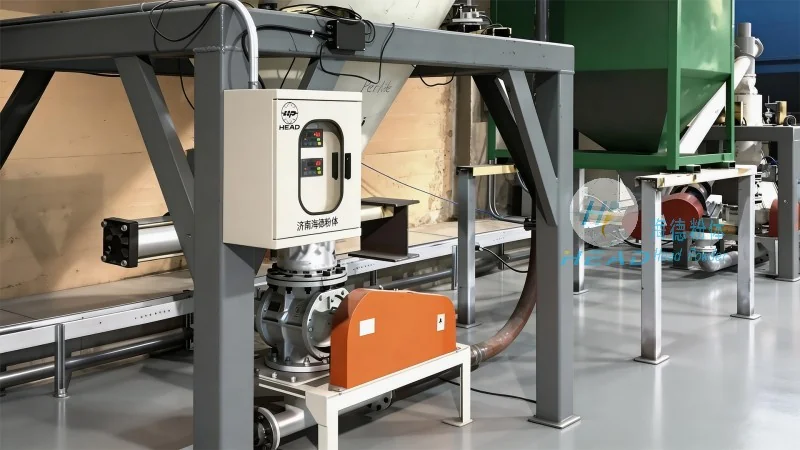
At the core of these systems lies a sophisticated combination of mechanical and pneumatic components that work in tandem to achieve seamless powder transport. The primary working principle involves the use of pressure differentials and controlled airflow to move powders through pipelines or containers. Key components typically include dust collectors, conveyors, and control valves that regulate the flow of material. The system operates by creating a vacuum or pressure gradient, which draws or pushes the powder along designated pathways. This method ensures minimal product degradation and maintains consistent flow rates, even for delicate or sensitive powders.
One of the critical aspects of the working principle is the integration of dust control mechanisms. Many multi-functional systems incorporate advanced filtration and dust extraction technologies to prevent particle dispersion and maintain a clean working environment. This is particularly important in industries where air quality and product purity are paramount, such as pharmaceuticals and food processing. The systems often utilize cyclone separators, bag filters, or electrostatic precipitators to capture fine particles, ensuring compliance with environmental and safety regulations.
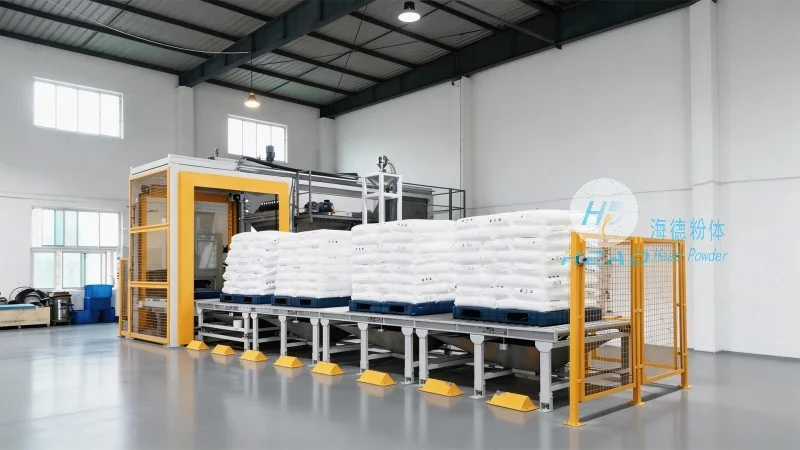
Multi-functional powder handling systems are characterized by several distinct features that enhance their performance and adaptability. One of the most notable features is their versatility, allowing them to handle a wide range of powder types, including fine powders, granules, and bulk materials. This adaptability is achieved through modular design, where components can be easily adjusted or replaced to suit different material characteristics and processing requirements.
Another significant feature is the system's efficiency in terms of energy consumption and operational costs. Advanced control systems and energy-saving technologies, such as variable frequency drives (VFDs), optimize the power usage based on the volume and type of material being transported. This not only reduces operational expenses but also contributes to environmental sustainability by minimizing energy waste.
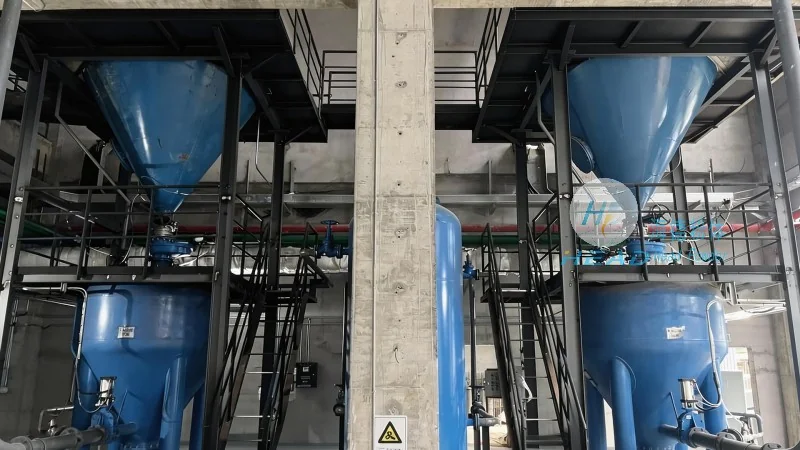
Reliability and durability are also key features of these systems. High-quality materials, such as stainless steel and corrosion-resistant alloys, are used in the construction of components to withstand harsh operating conditions and prolonged use. Additionally, the systems are equipped with monitoring and diagnostic tools that allow for real-time performance tracking and predictive maintenance. This proactive approach helps to minimize downtime and ensures consistent operational performance over extended periods.
The multi-functional powder handling systems offered by Shandong HeadPowder Engineering Co., Ltd. are widely used across various industrial sectors due to their comprehensive capabilities. In the pharmaceutical industry, these systems ensure the safe and hygienic transport of active pharmaceutical ingredients (APIs) and excipients, maintaining product integrity and regulatory compliance. In food processing, they facilitate the handling of ingredients like flour, sugar, and spices, ensuring consistent quality and preventing contamination.
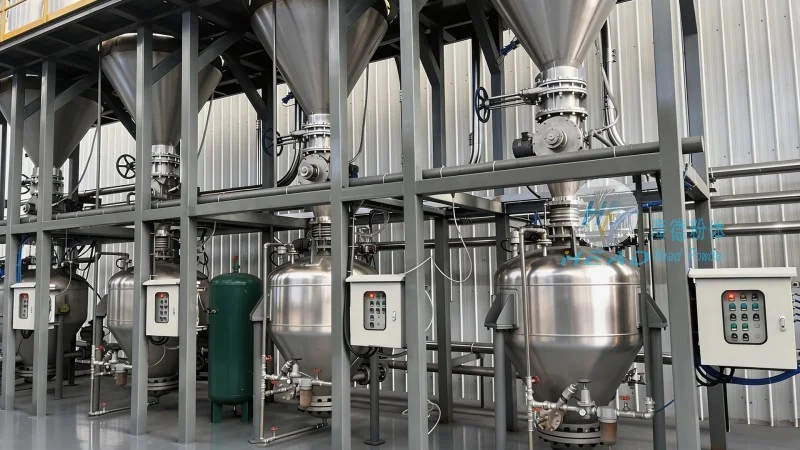
In the chemical industry, the systems are employed to handle reactive or hazardous powders, providing secure and controlled transport while minimizing the risk of accidents. The ability to handle diverse materials and maintain strict contamination control makes these systems indispensable in modern manufacturing environments.
Multi-functional powder handling systems represent a sophisticated solution for efficient and reliable powder transport in industrial applications. By integrating advanced mechanical and pneumatic technologies with robust control and dust management features, these systems offer significant advantages in terms of performance, safety, and cost-effectiveness. The expertise and commitment of Shandong HeadPowder Engineering Co., Ltd. in designing and manufacturing such systems ensure that clients receive tailored solutions that meet their specific operational needs and industry standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top