For industrial applications requiring the efficient and reliable transport of catalyst powders, pneumatic conveying systems offer a sophisticated solution. This article explores the working principle and key features of catalyst powder pneumatic conveying systems, highlighting how they enhance operational efficiency and safety in processing environments.
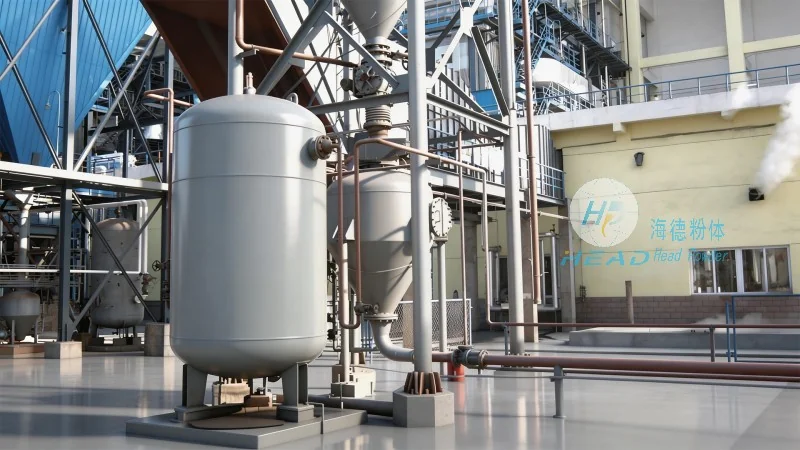
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and supplying advanced pneumatic conveying equipment tailored for catalyst powder handling. The company, known in the industry as HeadPowder, is headquartered in Shandong, China, and has established a reputation for delivering high-performance solutions that meet the stringent demands of modern chemical and petrochemical industries.
The core mechanism of a catalyst powder pneumatic conveying system involves the use of compressed air or other gases to transport particulate materials through a pipeline. The process typically begins with the catalyst powder being fed into a hopper or feeder, where it is then introduced into the conveying line. As the gas is introduced, it creates a flow that lifts and transports the powder particles through the system. This method relies on the principle of fluidization, where the gas flow overcomes the gravitational force acting on the powder particles, enabling them to move through the pipeline with minimal resistance.
Key components of the system include the feeding device, which ensures a consistent and controlled flow of catalyst powder into the conveying line; the conveying line itself, which is designed to withstand the pressure and temperature conditions of the process; and the control valves and regulators that manage the air flow and pressure. The system may also incorporate features such as pulse-jet cleaning mechanisms to prevent clogging and maintain consistent performance over time.
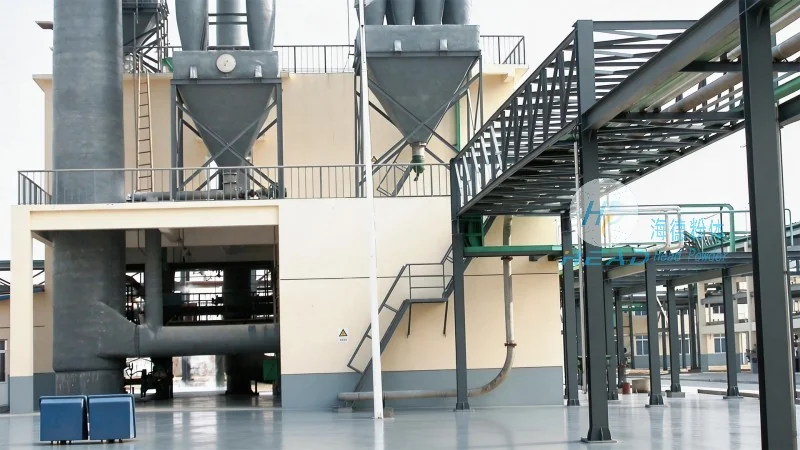
HeadPowder's catalyst powder pneumatic conveying systems are characterized by several notable features that enhance their functionality and reliability. One of the primary advantages is the ability to transport powders over long distances with minimal degradation of the material. The systems are designed to maintain the integrity of the catalyst particles, which is critical for their effectiveness in chemical reactions. Additionally, the systems offer high efficiency in terms of energy consumption, as they utilize compressed air more effectively than traditional mechanical conveying methods.
Another significant feature is the system's adaptability to various particle sizes and shapes. Catalyst powders can vary widely in their physical properties, and the conveying system is engineered to handle these variations without compromising performance. The design also incorporates safety features, such as pressure relief valves and explosion-proof components, to ensure safe operation in environments where flammable or hazardous materials are present.
Implementing a catalyst powder pneumatic conveying system from HeadPowder brings several benefits to industrial operations. The most obvious advantage is the improvement in process efficiency, as the system reduces the time and labor required for material handling. By automating the transport of catalyst powders, the system minimizes the risk of human error and ensures consistent material flow. This, in turn, enhances the overall productivity of the production line.
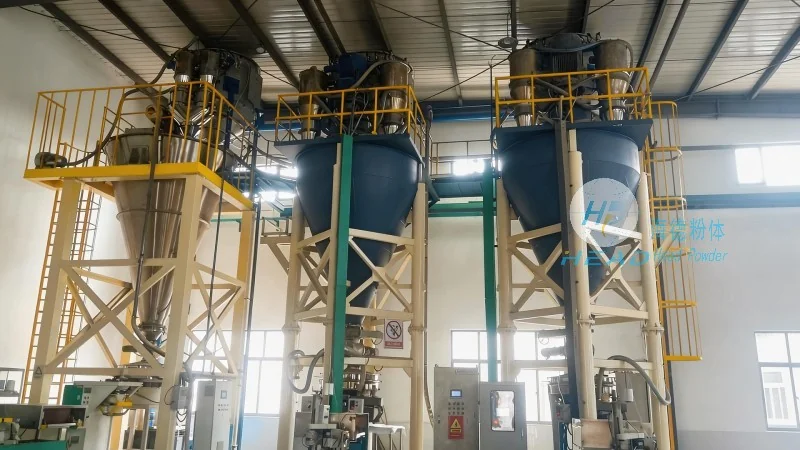
Furthermore, the system contributes to cost savings by reducing material loss and minimizing the need for manual handling. The consistent and controlled flow of powder also improves the quality of the final product, as it ensures that the catalyst is evenly distributed throughout the process. The reliability of the system, with its built-in maintenance features and long service life, further reduces downtime and maintenance costs.
Catalyst powder pneumatic conveying systems are widely used in various industrial applications, particularly in the chemical and petrochemical sectors. These systems are essential for transporting catalyst powders to reactors, storage tanks, and other processing equipment. The systems are also used in pharmaceutical manufacturing, where the handling of fine powders requires precision and control. In addition, the systems are applicable in environmental applications, such as the transport of catalysts used in waste treatment processes.
In summary, catalyst powder pneumatic conveying systems represent a sophisticated and efficient solution for the transport of catalyst powders in industrial settings. The working principle, which relies on the fluidization of particles using compressed air, combined with the key features offered by manufacturers like HeadPowder, ensures high performance, reliability, and safety. By investing in such systems, industrial operations can enhance their productivity, reduce costs, and maintain the quality of their products. Shandong HeadPowder Engineering Co., Ltd. continues to lead in the development of advanced pneumatic conveying solutions, providing customers with the tools needed to optimize their material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top