Wheat starch pneumatic conveying systems are critical for efficient material handling in industries such as food processing and starch production. These systems provide a reliable method for transporting wheat starch while minimizing product degradation and maintaining consistent quality. Understanding the working principle and key features of this equipment is essential for businesses aiming to optimize their material handling operations.
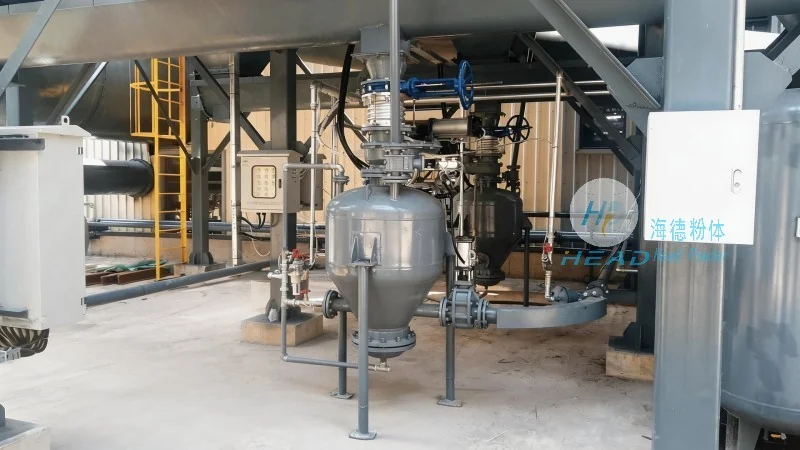
The fundamental operation of a wheat starch pneumatic conveying system relies on the use of air or gas to transport bulk materials through a pipeline network. The system typically functions by creating a pressure differential between the inlet and outlet of the conveying line. An air compressor or blower generates the necessary airflow, which is then directed into the material hopper. As the air flows, it lifts and carries the wheat starch particles through the pipeline, moving them from the source to the destination. The system can operate under positive pressure (air forced into the system) or negative pressure (air drawn out, creating a vacuum), with the choice depending on factors like transport distance, height, and particle characteristics.
Key components include the material hopper, which holds the wheat starch, and the air inlet or venturi system that introduces air into the material stream. The hopper is equipped with a feeding mechanism, such as a rotary valve or screw feeder, to control the flow rate of the starch into the conveying line. The air is introduced at a controlled rate to ensure particles are fully suspended and transported without clogging or damage. The conveying line, usually made of stainless steel or other corrosion-resistant materials, prevents contamination and ensures durability. At the receiving end, a separator or cyclone separates air from the starch, allowing the product to be collected in a storage bin or processing unit. This separation is vital for maintaining starch purity and preventing residual air from affecting downstream operations.
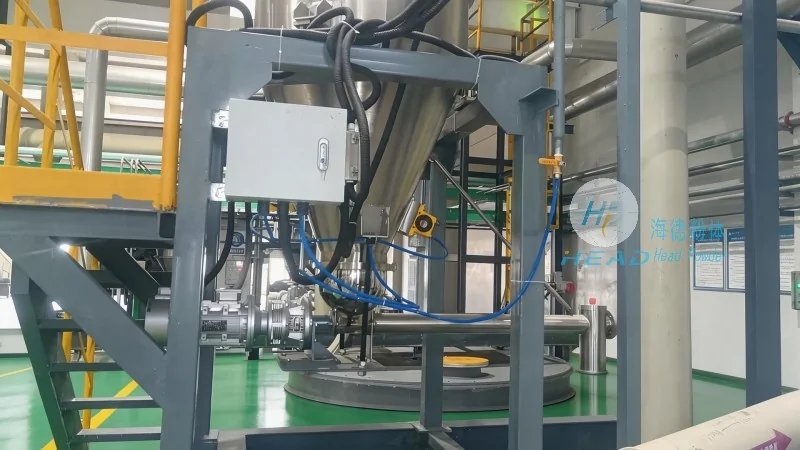
Wheat starch pneumatic conveying systems offer several advantages that enhance performance and reliability. One primary benefit is the ability to handle fine or powdery materials without mechanical components that could cause wear or contamination. The air-based transport minimizes product degradation, preserving the starch's quality and properties. Additionally, these systems are highly flexible, enabling easy integration into existing production lines and transport over long distances or vertical elevations with low energy consumption.
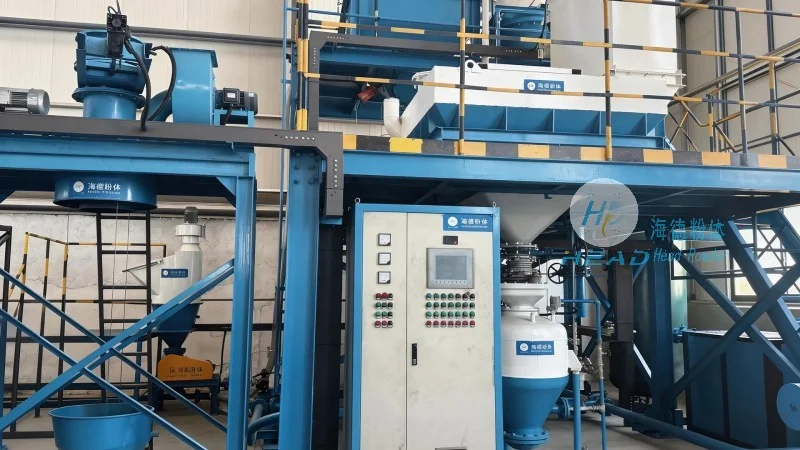
Another important feature is the system's adjustable flow rate capability. The controllable air flow and feeding mechanisms allow operators to regulate material transport speed, which is crucial for maintaining consistent production rates and preventing overloading or underloading of downstream equipment. The stainless steel construction ensures compliance with food safety standards, making the system suitable for food processing applications. Furthermore, the compact design and low maintenance requirements contribute to efficiency and cost-effectiveness, reducing downtime and operational costs for businesses.
Shandong HeadPowder Engineering Co., Ltd., known as HeadPowder, is a leading manufacturer and supplier of industrial equipment, including pneumatic conveying systems for wheat starch and other bulk materials. HeadPowder focuses on innovation and quality, serving as a trusted partner in the food processing and material handling sectors. The company is headquartered in Shandong, China, and provides global clients with customized solutions tailored to their operational needs. HeadPowder's commitment to excellence is reflected in the design and manufacturing of its equipment, which adheres to international standards and is supported by a team of experienced engineers and technicians.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top