Organic salt materials are widely used in various industrial sectors, including chemical manufacturing, food processing, and pharmaceutical production. The efficient and reliable transportation of these materials is crucial for maintaining production efficiency and ensuring product quality. Pneumatic conveying systems have emerged as a preferred method for handling organic salt materials due to their ability to transport materials in a dust-free environment, reducing contamination risks and improving operational safety. This article explores the working principle and key characteristics of pneumatic conveying for organic salt materials, highlighting the technological advancements and practical applications in the industry.
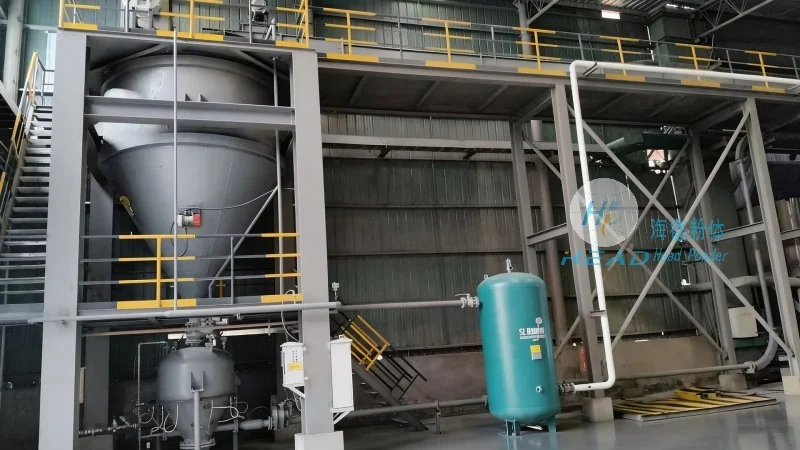
Pneumatic conveying utilizes air as the primary medium to transport solid materials, such as organic salts, through a pipeline system. The process typically involves two main types: aspiration (or suction) conveying and pressure (or blow) conveying. In aspiration systems, a vacuum is created at the material inlet to draw the organic salt particles into the pipeline along with the air stream. This method is ideal for handling materials that are light in weight and have a relatively low bulk density. Conversely, pressure conveying systems use compressed air to push the material through the pipeline, which is more suitable for materials with higher bulk density or those requiring higher pressure to overcome pipeline resistance.
The core components of a pneumatic conveying system for organic salt materials include a material hopper, a conveyor line, a control valve, and a dust collection system. The material is fed from the hopper into the pipeline, where it is mixed with the air stream. The air velocity within the pipeline must be maintained at a level sufficient to keep the organic salt particles suspended, preventing blockages and ensuring smooth flow. The system also incorporates a filter or dust collector at the discharge end to capture any fine particles, ensuring that the material is delivered in a clean and controlled manner. This mechanism allows for the continuous and automated transport of organic salt materials from the source to the destination, minimizing manual handling and associated risks.
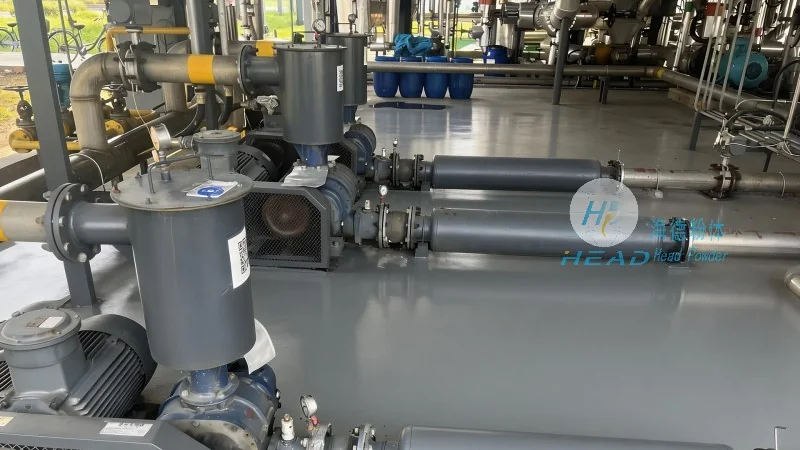
The application of pneumatic conveying for organic salt materials offers several distinct advantages that make it a preferred choice over traditional methods like belt conveyors or bucket elevators. Firstly, high efficiency and speed are significant benefits. Pneumatic systems can transport organic salt materials at much higher velocities, reducing the overall time required for material movement and increasing production throughput. This is particularly advantageous in high-demand industrial settings where rapid material turnover is essential.
Secondly, pneumatic conveying provides a dust-free and hygienic environment. Unlike mechanical conveyors, which can generate dust and cause contamination, pneumatic systems operate in enclosed pipelines, minimizing the risk of particle dispersion and ensuring that the organic salt materials remain clean and free from external contaminants. This is critical for industries such as food and pharmaceuticals, where product purity and safety are paramount. The enclosed system also helps in maintaining compliance with environmental regulations by reducing airborne particulate emissions.
Thirdly, the flexibility and adaptability of pneumatic conveying systems are notable characteristics. Organic salt materials often require transportation over varying distances and through complex layouts, including vertical and horizontal changes. Pneumatic systems can easily accommodate these variations by adjusting the air pressure and velocity, ensuring that the material is transported smoothly without the need for additional equipment like transfer chutes or elevators. This flexibility allows for the integration of the conveying system into existing production lines, reducing installation costs and minimizing downtime during setup.
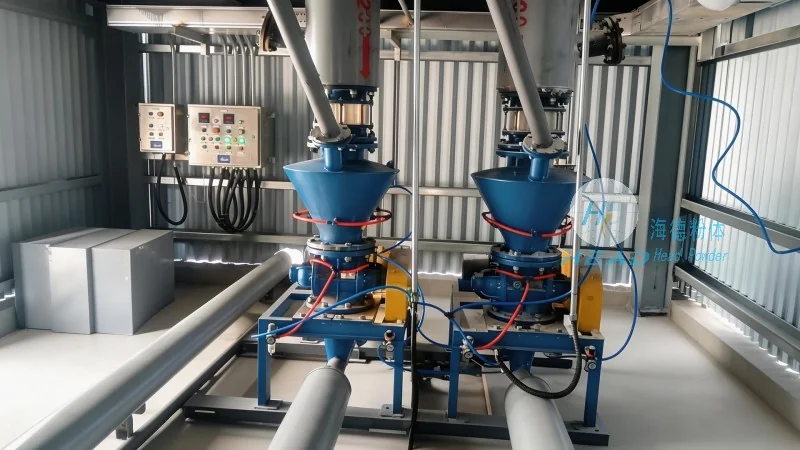
Additionally, pneumatic conveying offers energy efficiency and cost-effectiveness. While the initial investment in a pneumatic system may be higher than traditional conveyors, the long-term operational costs are lower due to reduced maintenance requirements and lower energy consumption. The system's ability to handle organic salt materials in a continuous flow also reduces the need for intermediate storage, further optimizing operational efficiency. Moreover, the absence of moving parts in the pipeline (except for the air flow) minimizes wear and tear, extending the lifespan of the equipment and reducing the frequency of repairs.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of organic salt materials. With years of experience in the industry, HeadPowder has developed advanced technologies and innovative solutions that address the unique challenges associated with handling organic salts, such as their varying particle sizes, moisture content, and chemical properties. The company's team of engineers and technicians works closely with clients to understand their production requirements and provide tailored solutions that enhance operational efficiency and product quality.
HeadPowder's pneumatic conveying systems are designed with high-quality materials and advanced control systems to ensure reliable and consistent performance. The company utilizes state-of-the-art design software to simulate and optimize the conveying process, ensuring that the system operates at peak efficiency under various conditions. This approach allows for the precise control of air pressure, velocity, and material flow, minimizing the risk of blockages and ensuring that the organic salt materials are transported safely and effectively. The systems are also equipped with safety features, such as pressure relief valves and emergency shut-off mechanisms, to protect both the equipment and personnel from potential hazards.
HeadPowder Engineering's commitment to quality and customer satisfaction is evident in its comprehensive after-sales service. The company provides regular maintenance and technical support to ensure that the pneumatic conveying systems continue to operate at optimal levels. This includes routine inspections, component replacement, and troubleshooting services to address any issues that may arise. By partnering with HeadPowder, clients can benefit from a reliable and efficient material handling solution that meets their specific requirements and enhances their overall production capabilities.
In conclusion, pneumatic conveying for organic salt materials offers significant advantages in terms of efficiency, safety, and flexibility. The working principle, which involves the use of air as a carrier to transport materials through a pipeline system, is well-suited for handling organic salts due to their physical properties. The key characteristics of these systems, including high speed, dust-free operation, and adaptability, make them an ideal choice for various industrial applications. With the expertise and experience of companies like Shandong HeadPowder Engineering Co., Ltd., the implementation of pneumatic conveying systems has become more accessible and effective, enabling industries to improve their production processes and maintain high standards of product quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top