Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems tailored for coal ash material handling. This article delves into the fundamental working principles and distinctive features of such systems, offering a comprehensive understanding for potential clients and industry professionals.
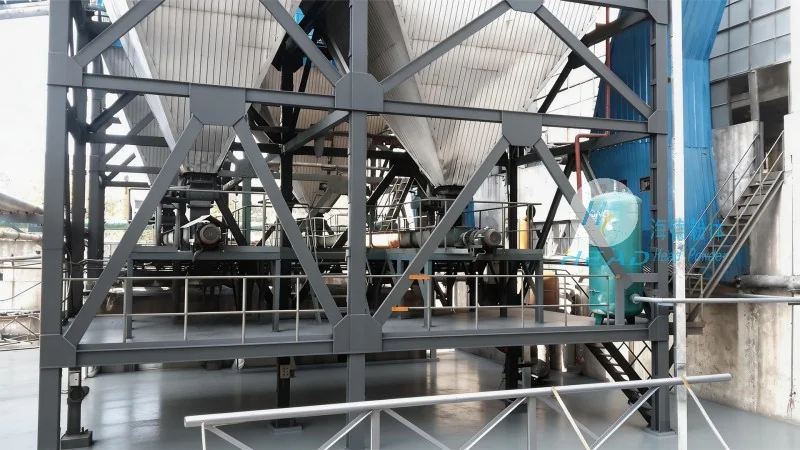
The core mechanism of a coal ash pneumatic conveying system involves the transportation of solid particles, in this case, coal ash, through a pipeline using a gas stream, typically air. There are two primary types of pneumatic conveying systems: suction (or aspirating) and pressure (or blow) systems, each with distinct operational characteristics.
In a suction system, the conveying air is drawn from the material source, creating a negative pressure that pulls the coal ash particles into the pipeline. This method is ideal for applications where the material is located at a higher elevation or needs to be collected from multiple points. The system typically includes a vacuum pump, a hopper for material storage, and a filter to capture fine particles before releasing the air back into the environment.
Conversely, a pressure system utilizes a positive pressure generated by a blower or compressor to push the coal ash material through the pipeline. This approach is suitable for transporting materials over longer distances or when the material source is at a lower elevation. The pressure system often features a hopper with a valve to control material discharge and a pressure regulator to maintain consistent airflow.
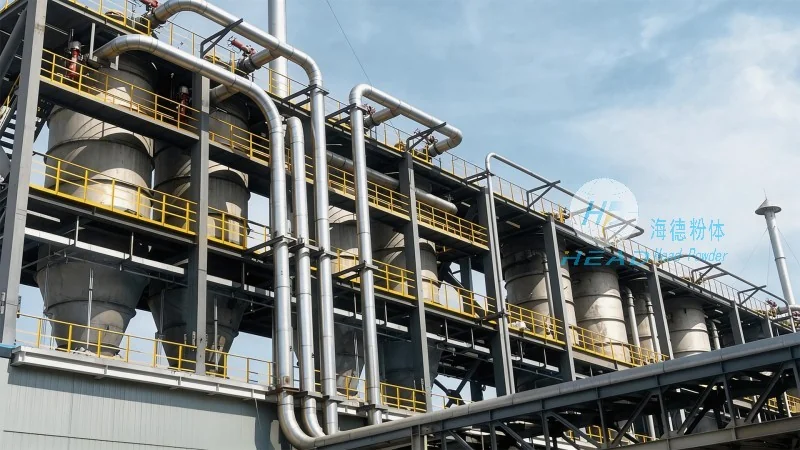
Both systems rely on the principle of fluidization, where the gas stream creates a turbulent flow that suspends the coal ash particles, allowing them to be carried along the pipeline. The velocity of the gas and the size of the particles are critical factors in determining the efficiency of the conveying process. Proper design ensures that the gas velocity is sufficient to keep the particles suspended without causing excessive wear on the pipeline or equipment.
Coal ash pneumatic conveying systems offer several advantages that make them a preferred choice for industrial applications. One of the most significant benefits is their ability to handle fine and abrasive materials like coal ash without the need for mechanical components that could be prone to wear and tear. The absence of moving parts reduces maintenance requirements and extends the operational lifespan of the system.
Environmental considerations are another critical aspect. Pneumatic conveying systems are generally considered more environmentally friendly compared to traditional methods such as belt conveyors or bucket elevators. They minimize dust emissions by enclosing the material in a sealed pipeline, reducing the risk of airborne particulate matter and improving workplace safety. Additionally, the system can be equipped with filtration and air purification units to further minimize environmental impact.
Efficiency and flexibility are also key characteristics. These systems can transport coal ash over long distances with minimal energy consumption, making them cost-effective for large-scale operations. The modular design allows for easy integration with existing infrastructure and can be scaled up or down to accommodate varying production needs. Furthermore, the ability to convey materials from multiple sources to a single destination or vice versa enhances operational flexibility.
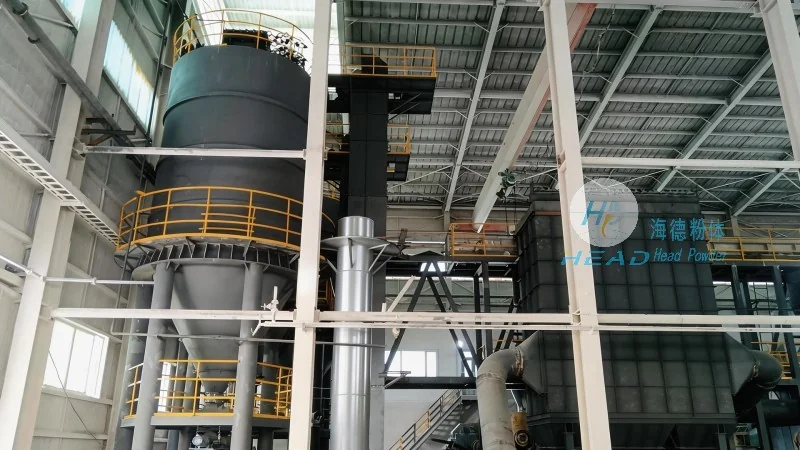
Another notable feature is the system's ability to handle a wide range of particle sizes and moisture content. Coal ash particles can vary significantly in size and can be wet or dry, and pneumatic conveying systems are designed to accommodate these variations without compromising performance. The use of appropriate air velocities and pipeline diameters ensures that the material is conveyed smoothly and without blockages.
The application of coal ash pneumatic conveying systems spans various industries, including power generation, cement production, and waste management. In power plants, these systems are used to transport coal ash from the boiler to storage facilities or for further processing. In cement plants, coal ash is often used as a supplementary cementitious material, and pneumatic conveying facilitates its efficient transfer from storage to the production line.
The impact of these systems extends beyond material handling, contributing to overall operational efficiency and sustainability. By reducing the reliance on traditional, high-maintenance equipment, companies can lower their operational costs and improve their environmental footprint. The flexibility and adaptability of the systems also enable them to meet the evolving demands of industrial processes, ensuring long-term viability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top