Bulk bag breakage pneumatic conveying systems represent a sophisticated solution for handling and transporting bulk materials from large capacity bags. These systems are engineered to efficiently break open bulk bags, transfer the contained material into a processing or storage system, and manage the entire material flow with precision. The core of such a system lies in its ability to integrate mechanical and pneumatic components to achieve seamless material handling, ensuring minimal loss and optimal operational efficiency.
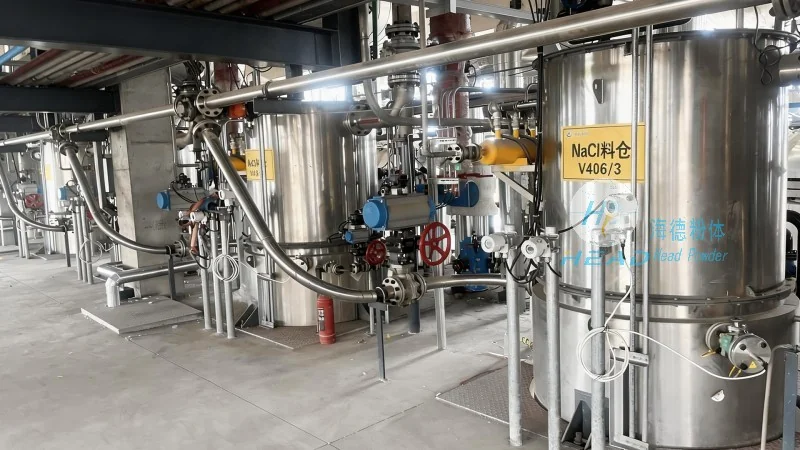
The operation of a bulk bag breakage pneumatic conveying system typically involves several key stages. Initially, the bulk bag is positioned over a receiving hopper or a dedicated breakage chamber. Mechanical components, such as a bag opener or a cutting device, are activated to rupture the bag's top, allowing the material to fall into the chamber. Simultaneously, a pneumatic conveying unit, often equipped with a positive displacement blower or a rotary airlock, generates the necessary air pressure to draw the material from the chamber and transport it through a pipeline network. The system may include a filter or a dust collection unit to manage any airborne particles, ensuring compliance with environmental standards and maintaining air quality. The entire process is controlled by a programmable logic controller (PLC) or a similar automation system, which coordinates the operation of the bag opener, the air compressor, and the conveying equipment to ensure smooth and continuous material transfer.
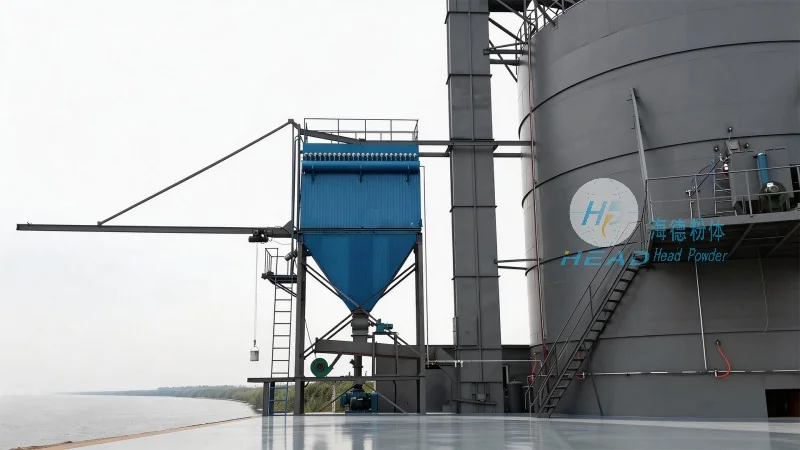
Bulk bag breakage pneumatic conveying systems offer several distinct features that enhance their utility in industrial applications. One of the primary advantages is the ability to handle large quantities of material from single bulk bags, reducing the need for manual handling and minimizing material loss during transfer. The pneumatic conveying method ensures that the material is transported without direct contact with the conveying equipment, which is particularly beneficial for handling sensitive or abrasive materials that could cause wear or contamination. Additionally, these systems are designed for high efficiency and low maintenance, with components like the airlock and the blower being robust and durable to withstand continuous operation. The integration of dust collection and filtration systems not only improves air quality but also protects the equipment from dust accumulation, extending its operational lifespan. Furthermore, the modular design of such systems allows for easy installation and integration into existing production lines, providing flexibility in adapting to different material handling requirements.
Bulk bag breakage pneumatic conveying systems are widely used across various industries that rely on bulk material handling. In the chemical industry, these systems are essential for transporting powders and granules, such as fertilizers, pigments, and pharmaceuticals, where maintaining material purity and preventing contamination is critical. The food and beverage industry also benefits from these systems, as they can handle dry ingredients like flour, sugar, and spices while ensuring hygiene and compliance with food safety regulations. In the mining and mineral processing sector, bulk bag breakage systems are used to transport raw ores and concentrates, enabling efficient material transfer from storage to processing equipment. The construction industry utilizes these systems for handling bulk materials like cement, sand, and gravel, improving material flow in construction sites and reducing labor costs. Overall, the versatility and efficiency of bulk bag breakage pneumatic conveying systems make them a preferred choice for industries that require reliable and cost-effective bulk material handling solutions.
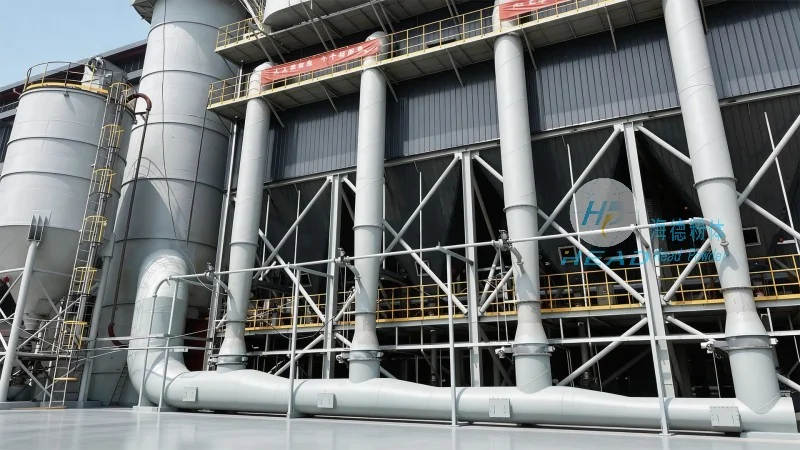
Bulk bag breakage pneumatic conveying systems are advanced industrial solutions that combine mechanical and pneumatic technologies to efficiently handle and transport bulk materials from large bags. By integrating features such as automated bag opening, efficient pneumatic conveying, and dust control, these systems offer significant advantages in terms of operational efficiency, material integrity, and environmental compliance. The systems are designed to meet the diverse needs of various industries, from chemical and food processing to mining and construction, providing reliable and cost-effective material handling solutions. HeadPowder, a leading manufacturer in this field, specializes in developing and supplying high-quality bulk bag breakage pneumatic conveying systems. With a strong commitment to innovation and customer satisfaction, HeadPowder ensures that its systems are tailored to meet the specific requirements of each client, delivering robust and efficient solutions for bulk material handling. Based in Shandong, China, HeadPowder leverages its expertise and local manufacturing capabilities to provide comprehensive support and reliable products to its global clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top