Efficient material handling is a critical component in the operation of industrial facilities, particularly in the power generation sector where fly ash management plays a pivotal role. The pneumatic conveying system for fly ash silos is a sophisticated solution designed to transport bulk materials like fly ash from storage silos to processing or disposal sites. This article delves into the working principle and key features of such systems, highlighting their importance in optimizing operational efficiency and safety.
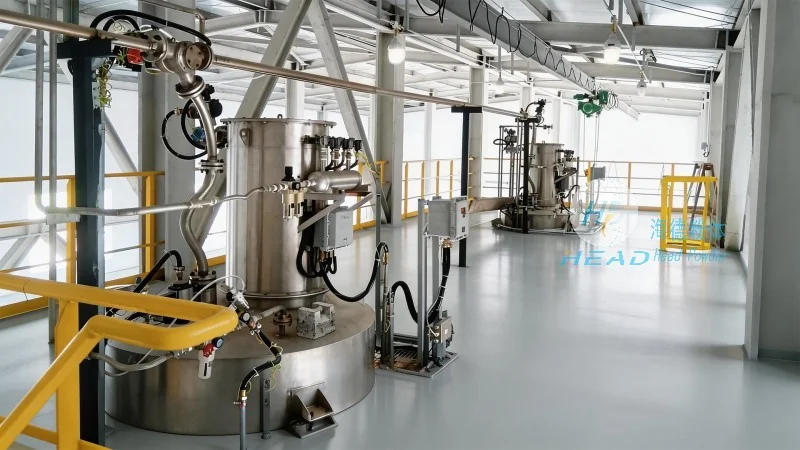
The core of a fly ash silo material pneumatic conveying system lies in its ability to use air pressure to move solid particles through a pipeline. The system typically comprises a silo, a conveying line, a blower or compressor, and a control system. The process begins when the fly ash is discharged from the silo into the conveying line. A fan or compressor generates a high-pressure air stream that propels the fly ash particles through the pipeline. The air velocity is carefully controlled to ensure that the particles remain suspended and are transported without clogging or damage. The system may include components like cyclones or filters to separate the fly ash from the air at the receiving end, ensuring that the material is delivered in a dry and clean state. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and operational costs.
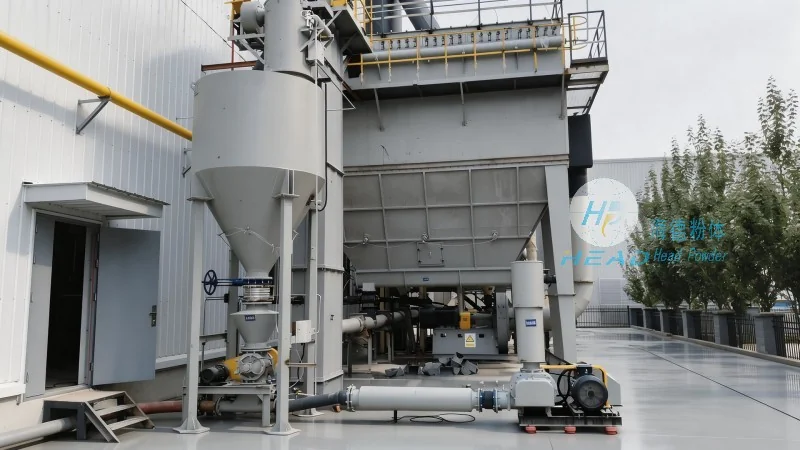
Several distinct features make pneumatic conveying systems ideal for fly ash handling applications. Firstly, the system offers a high degree of flexibility in terms of layout and routing. The conveying lines can be installed in various configurations, allowing for the integration of multiple silos or processing units. This adaptability is crucial for facilities with complex material flow requirements. Secondly, the system provides excellent material containment and dust control. The sealed pipeline design prevents dust emissions, ensuring compliance with environmental regulations and maintaining a safe working environment. Thirdly, the system is highly efficient in terms of energy consumption. Compared to other material handling methods, such as bucket elevators or belt conveyors, pneumatic conveying systems can achieve higher material throughput with lower energy input. This efficiency translates into cost savings over the system's operational life. Additionally, the system is relatively low in maintenance requirements. The absence of moving parts in the conveying line reduces wear and tear, leading to longer service intervals and lower maintenance costs. Finally, the system offers a high level of safety. The sealed design minimizes the risk of material spillage or dust explosions, which are common hazards in traditional material handling methods.
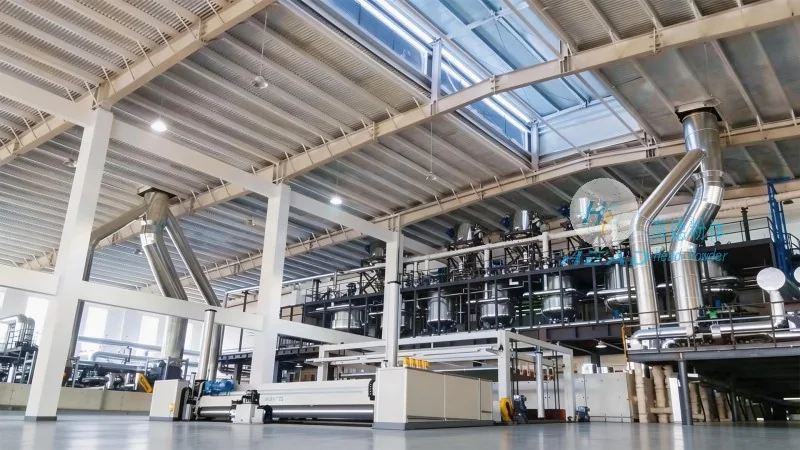
As a leading provider of industrial engineering solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of pneumatic conveying systems for various bulk material applications. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the power generation and environmental sectors. HeadPowder's expertise lies in developing customized solutions that meet the specific needs of clients, ensuring optimal performance and reliability. The company's commitment to quality is evident in its adherence to international standards and rigorous testing protocols. By leveraging advanced technology and a team of experienced engineers, HeadPowder delivers systems that enhance operational efficiency, reduce costs, and improve safety for its clients. The company's headquarters is located in Shandong, China, where it maintains a state-of-the-art manufacturing facility and a dedicated customer support team.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top