Nickel powder is a critical material in various industrial applications, including chemical processing, metallurgy, and manufacturing. The efficient and safe transportation of nickel powder from one location to another is essential for maintaining production efficiency and ensuring product quality. Pneumatic conveying systems have emerged as a preferred solution for handling nickel powder due to their ability to transport powders in a controlled, dust-free environment. This article explores the working principle and key features of a nickel powder material pneumatic conveying system, highlighting how such systems enhance operational performance in industrial settings.
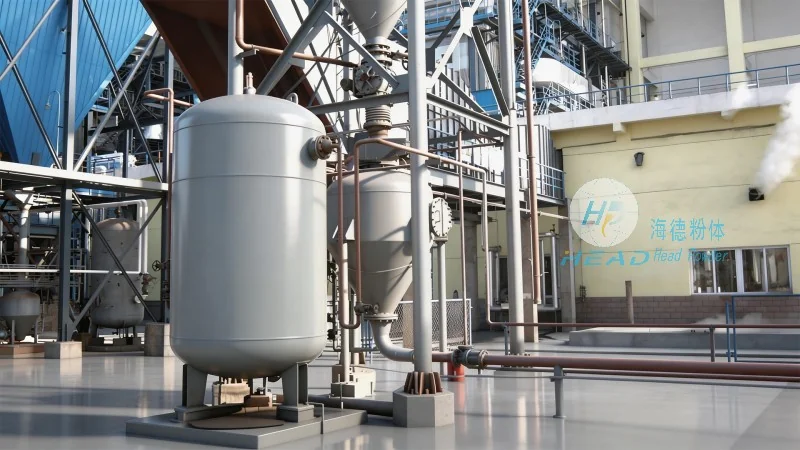
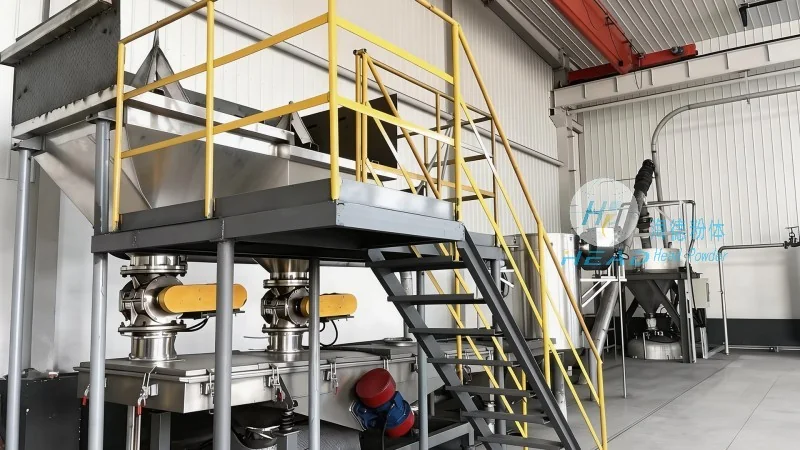
A nickel powder pneumatic conveying system operates on the fundamental principle of using air or gas to transport solid particles. The system typically consists of several key components, including a material feeder, a conveying line, a separation unit, and a dust collection system. The process begins with the nickel powder being fed into the system, often through a rotary valve or a pressure feeder, which ensures a consistent and controlled flow of material. The feeder then introduces the powder into a pipeline where a high-velocity air stream is present. This air stream, generated by a blower or a fan, propels the nickel powder particles through the pipeline. The velocity of the air is carefully controlled to maintain the powder in a suspended state, preventing it from settling or clogging the system. The conveying line may include bends, expansions, or other components that guide the material to its destination. Upon reaching the end of the pipeline, the air and powder mixture enters a separation unit, such as a cyclone or a bag filter, where the air is separated from the powder. The separated nickel powder is then collected in a hopper or a storage bin, while the air is either vented to the atmosphere or filtered to remove any residual dust. The entire process is driven by the pressure and flow characteristics of the air system, which are optimized to match the properties of the nickel powder, such as its density, particle size, and moisture content. By understanding and controlling these parameters, the system ensures reliable and efficient transportation of nickel powder without compromising safety or product integrity.
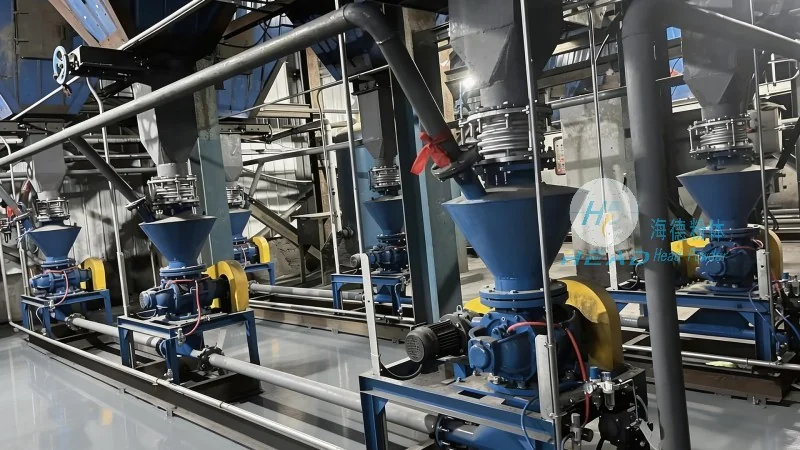
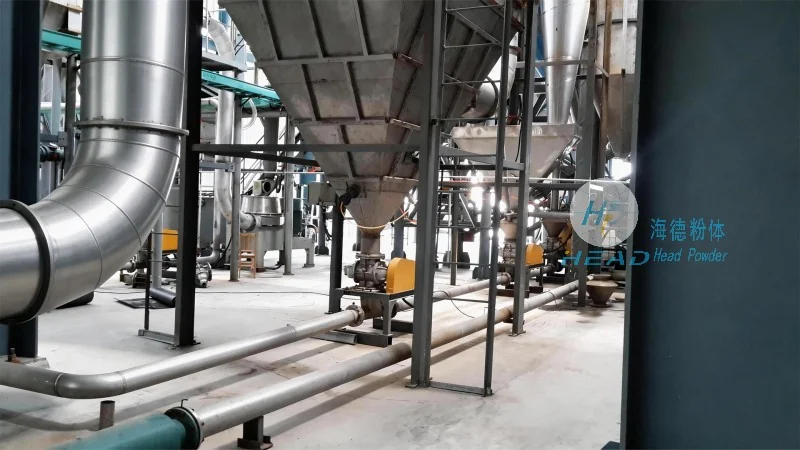
The nickel powder pneumatic conveying system offers several distinct advantages that make it an ideal choice for industrial applications. Firstly, it provides a dust-free and enclosed environment, which is crucial for handling nickel powder, as it can be hazardous if released into the air. The system prevents dust exposure, reducing the risk of respiratory issues and environmental contamination. Secondly, it offers high efficiency and flexibility in material handling. The system can transport nickel powder over long distances and through complex layouts, adapting to various production requirements. The adjustable air velocity and pressure allow for precise control over the flow rate, ensuring that the material is conveyed at the optimal speed without causing excessive wear on the equipment. Thirdly, the system enhances safety by minimizing the risk of dust explosions. Unlike traditional bulk handling methods, which may involve open hoppers or chutes, the pneumatic system keeps the powder contained within the pipeline, reducing the likelihood of ignition sources. Additionally, the system is designed to handle the specific properties of nickel powder, such as its tendency to agglomerate or clog. Advanced features, such as in-line mixers or vibrators, can be integrated to break up agglomerates and maintain a consistent flow. Fourthly, the system contributes to operational cost savings by reducing material loss and maintenance costs. By preventing product degradation and minimizing the need for manual handling, the system improves overall productivity. The use of high-quality materials and robust construction ensures long-term reliability, reducing downtime and maintenance expenses. Overall, the nickel powder pneumatic conveying system combines efficiency, safety, and flexibility, making it a superior solution for transporting nickel powder in industrial settings.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized engineering solutions for powder handling and material transportation. With a focus on innovation and customer-centric approaches, the company has established itself as a trusted partner in the industry. HeadPowder specializes in designing, manufacturing, and installing pneumatic conveying systems tailored to the unique needs of clients, including those handling nickel powder and other challenging materials. The company's team of experienced engineers and technicians leverages advanced technology and industry best practices to develop customized solutions that enhance operational efficiency and safety. HeadPowder's commitment to quality is reflected in its adherence to international standards and rigorous testing protocols. The company's facilities, located in Shandong, China, are equipped with state-of-the-art equipment and a skilled workforce dedicated to delivering high-performance systems. By combining technical expertise with practical experience, HeadPowder ensures that its pneumatic conveying systems meet the highest standards of performance and reliability. The company's dedication to customer satisfaction and continuous improvement has earned it a reputation for excellence in the market. Whether for new installations or system upgrades, HeadPowder provides comprehensive support, from initial consultation to long-term maintenance, ensuring that clients achieve optimal results in their powder handling operations. With a strong presence in the industry and a focus on sustainable solutions, Shandong HeadPowder Engineering Co., Ltd. continues to be a key player in the development of advanced material transportation technologies.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top