Understanding the working principle and key features of lithium hydroxide pneumatic conveying systems is crucial for industries that handle this specialized chemical. These systems are designed to efficiently transport lithium hydroxide, a critical material in various applications such as battery production and chemical synthesis. The technology behind these systems leverages pneumatic principles to move the material through pipelines, ensuring safety, efficiency, and reliability in material handling processes.
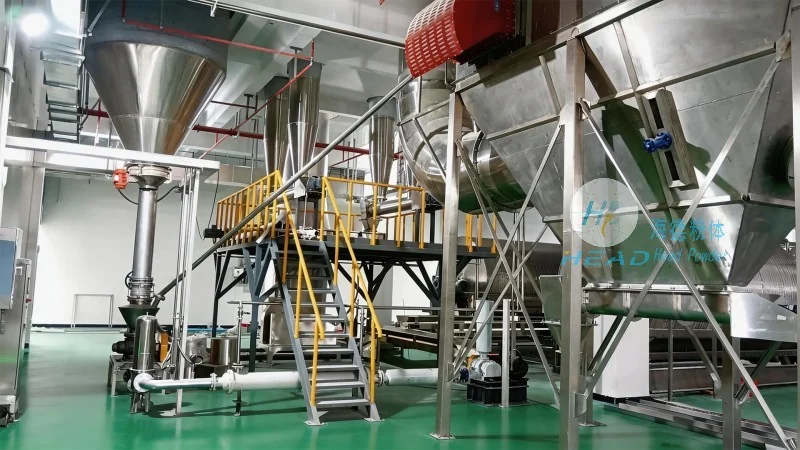
The core working principle of lithium hydroxide pneumatic conveying systems revolves around the use of compressed air or gas to transport the material. In this system, the lithium hydroxide is introduced into a hopper or feeder, where it is then drawn into a pipeline by the airflow. The air velocity is carefully controlled to maintain a consistent flow rate, preventing material degradation or blockages. The system typically operates under negative pressure, which helps in containing dust and ensuring a clean transfer process. The conveying process involves several key components, including the feeder, the conveying line, and the receiver, all working in tandem to achieve seamless material transport.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, offers advanced lithium hydroxide pneumatic conveying systems with several distinctive features. One of the primary features is the robust design that ensures durability and long-term performance, even under demanding operational conditions. The systems are equipped with advanced control mechanisms that allow for precise regulation of air pressure and flow, optimizing the conveying efficiency and minimizing energy consumption. Additionally, the systems incorporate dust collection and filtration components to maintain a clean environment and comply with environmental regulations. The modular design of these systems enables easy integration into existing production lines, providing flexibility and adaptability for different industrial applications. Furthermore, the use of high-quality materials in the construction of the conveying components ensures resistance to corrosion and chemical reactions, which is essential when handling lithium hydroxide.
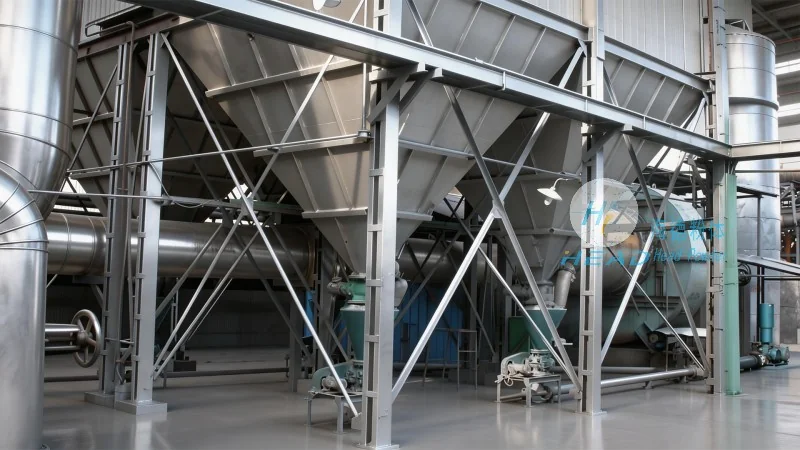
Implementing lithium hydroxide pneumatic conveying systems brings numerous benefits to industrial operations. The primary advantage is the significant improvement in material handling efficiency, as the systems can transport large quantities of lithium hydroxide over long distances with minimal downtime. The automated control systems reduce the need for manual intervention, enhancing safety and reducing labor costs. The systems also contribute to a cleaner working environment by minimizing dust and particle emissions, which is crucial for maintaining workplace safety and compliance with environmental standards. Moreover, the energy-efficient design of these systems helps in reducing operational costs, making them a cost-effective solution for long-term material transport needs. The reliability of the pneumatic conveying systems ensures consistent performance, which is vital for maintaining production schedules and meeting quality standards in lithium hydroxide processing.
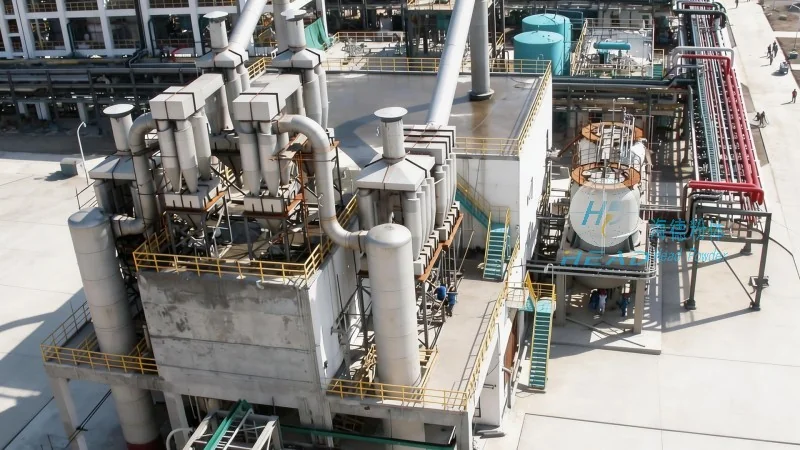
Lithium hydroxide pneumatic conveying systems are widely used in various industrial applications, particularly in the battery manufacturing industry. These systems are essential for transporting lithium hydroxide from storage facilities to production lines, where it is used as a key component in lithium-ion batteries. The systems are also utilized in chemical plants that produce lithium-based compounds, ensuring the safe and efficient transfer of the material during the synthesis process. Additionally, the systems find applications in research and development facilities that require precise handling of lithium hydroxide for experimental purposes. The versatility of the systems allows them to be adapted to different production scales, from small-scale laboratory operations to large-scale industrial manufacturing. The ability to handle varying material flow rates and distances makes these systems suitable for a wide range of industrial needs.
In conclusion, lithium hydroxide pneumatic conveying systems are sophisticated equipment that combines advanced technology with robust design to ensure efficient and safe material transport. The working principle, which relies on pneumatic pressure and controlled airflow, along with the key features such as durability, precision control, and environmental compliance, make these systems an ideal choice for industries handling lithium hydroxide. Shandong HeadPowder Engineering Co., Ltd., based in China, is a reputable manufacturer that specializes in developing and supplying high-quality pneumatic conveying systems tailored to the specific needs of lithium hydroxide applications. With a commitment to innovation and quality, the company provides reliable solutions that enhance operational efficiency and safety in material handling processes. The systems manufactured by HeadPowder are designed to meet the stringent requirements of modern industrial applications, ensuring long-term performance and customer satisfaction.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top