The corn kernels pneumatic conveying system is a specialized industrial solution designed for the efficient and reliable transport of corn kernels and similar granular materials. As a key component in agricultural processing and food production industries, this system leverages the principles of pneumatic transport to move bulk materials over short to medium distances with minimal mechanical contact and reduced product degradation. The system is engineered to handle the unique characteristics of corn kernels, such as their size, density, and susceptibility to breakage, ensuring optimal performance and product integrity throughout the conveying process.
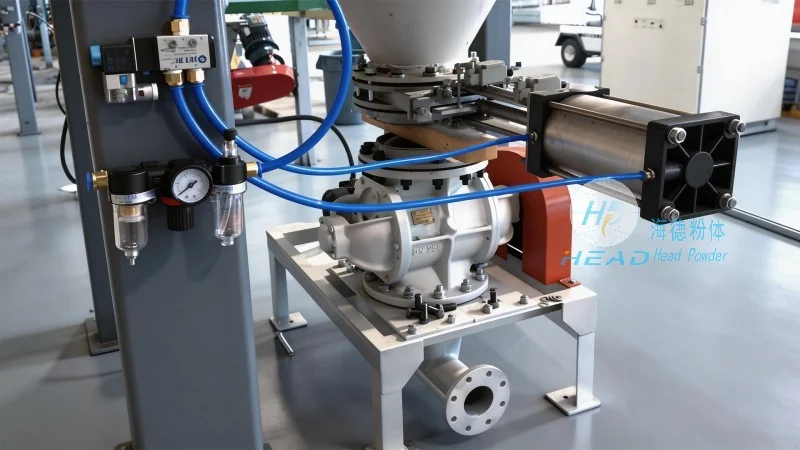
The corn kernels pneumatic conveying system typically consists of several critical components that work in tandem to achieve effective material transport. The primary elements include a material hopper or feed bin, a rotary airlock or feeder to control the flow of corn kernels into the system, a conveying pipeline (often equipped with bends and straight sections), a fan or blower to generate the necessary air pressure, and a discharge hopper or collection bin at the receiving end. The rotary airlock feeder is particularly important as it prevents the backflow of air while allowing a controlled, steady flow of corn kernels into the pipeline, maintaining system efficiency and preventing material buildup.
The fan or blower serves as the power source, creating a pressure differential that propels the corn kernels through the pipeline. The air velocity within the pipeline is carefully managed to ensure that the corn kernels are carried by the air stream without excessive abrasion or breakage. The conveying pipeline is usually made of durable materials like stainless steel or high-density polyethylene to withstand the abrasive nature of corn kernels and the internal pressure generated by the system. The system may also include additional components such as filters to remove dust and debris from the air stream, and pressure relief valves to maintain safe operating conditions.
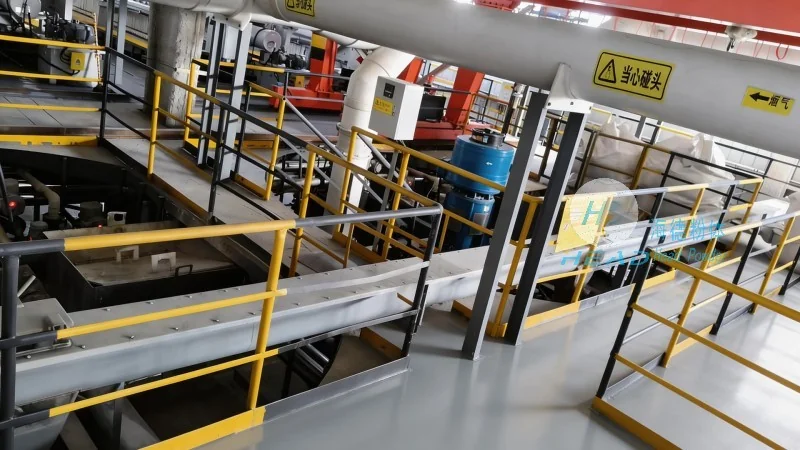
The fundamental principle behind the corn kernels pneumatic conveying system is the use of air as a medium to transport solid particles. In a typical operation, corn kernels are fed into the system via the rotary airlock feeder. The fan then generates a high-velocity air stream that draws the corn kernels into the pipeline. As the air and corn kernels move through the pipeline, the corn kernels are suspended and carried by the air flow. The air velocity is maintained at a level that ensures the corn kernels remain in suspension without settling or clogging the pipeline. At the receiving end, the air is separated from the corn kernels, often through a cyclone separator or a filter, and the corn kernels are collected in the discharge hopper. The separated air is then either recirculated back into the system or exhausted to the atmosphere, depending on the system design.
This pneumatic transport method offers several advantages over traditional mechanical conveying systems, such as belt conveyors or screw conveyors. For instance, it eliminates the need for moving parts in contact with the corn kernels, reducing the risk of product contamination and mechanical wear. Additionally, the system can handle materials that are difficult to convey mechanically, such as those with high moisture content or irregular shapes. The pneumatic conveying system also allows for flexible layout designs, as the pipeline can be routed around obstacles and changes in elevation with minimal modifications.
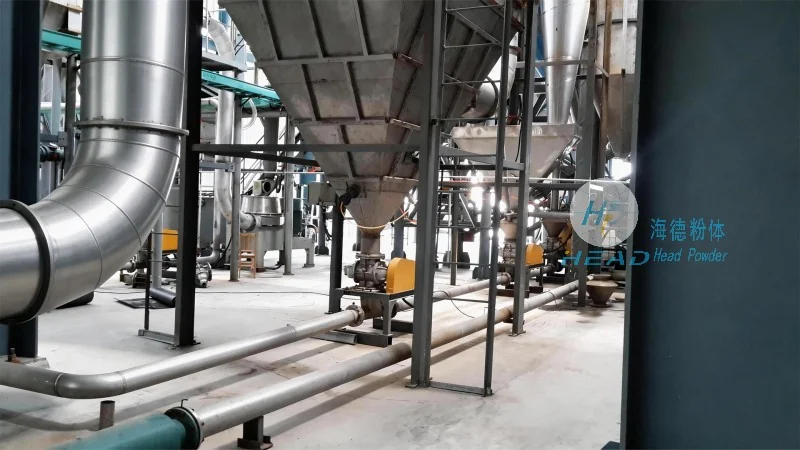
The corn kernels pneumatic conveying system offers numerous benefits that make it an ideal choice for various industrial applications. One of the key advantages is its ability to maintain product integrity. By minimizing mechanical contact and reducing the risk of breakage, the system ensures that the corn kernels retain their quality and nutritional value. This is particularly important in food processing applications where product quality is critical. Another advantage is the system's efficiency in terms of energy consumption and operational costs. The use of air as a transport medium is generally more energy-efficient than mechanical conveying methods, especially for short to medium distance transports. The system also provides a hygienic and clean operation, as the pipeline is enclosed and the air stream can be filtered to remove contaminants.
The applications of the corn kernels pneumatic conveying system are widespread across the agricultural and food processing industries. It is commonly used in corn processing plants for transporting corn kernels from storage bins to processing equipment, such as dehullers, cleaners, and grinders. The system is also used in feed mills to convey corn kernels to mixing and extrusion equipment. Additionally, it is employed in food processing facilities for transporting corn kernels to packaging lines or storage areas. The system's flexibility and adaptability make it suitable for various production scales, from small-scale operations to large industrial plants.
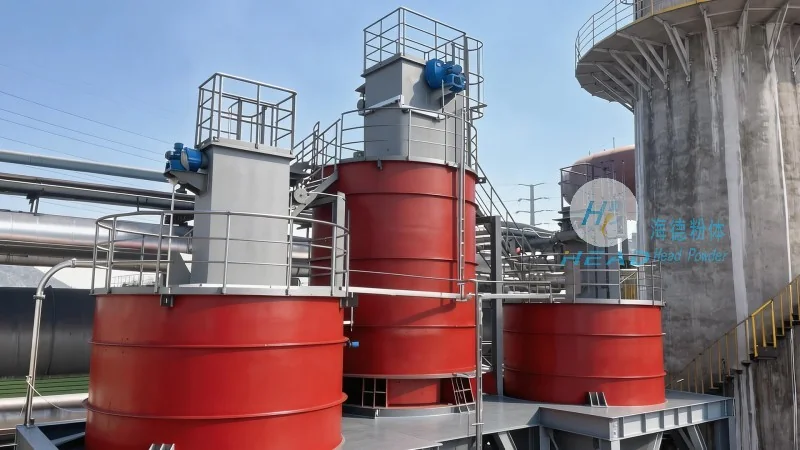
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of specialized pneumatic conveying systems, including those designed for corn kernels and other granular materials. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the agricultural processing and food production industries. HeadPowder's expertise lies in designing and manufacturing custom pneumatic conveying systems that meet the specific requirements of its clients, ensuring optimal performance and reliability. The company's products are known for their durability, efficiency, and adherence to industry standards, making them a preferred choice for businesses seeking reliable material handling solutions.
HeadPowder is committed to providing comprehensive solutions that address the unique challenges of material transport in the agricultural and food sectors. The company's team of engineers and technicians work closely with clients to understand their operational needs and design systems that enhance productivity and product quality. With a manufacturing facility located in Shandong, China, HeadPowder leverages advanced technology and rigorous quality control processes to ensure that its products meet the highest standards. The company's dedication to customer satisfaction and continuous improvement has earned it a reputation for excellence in the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top