Urea granule pneumatic conveyors are specialized equipment used in industrial settings to transport urea granules efficiently and safely. These systems utilize air or gas as the medium to move the material from one location to another, offering advantages such as reduced labor costs, minimized material handling risks, and improved process control. As a key component in fertilizer production and distribution, understanding the functionality and design principles of these conveyors is crucial for optimizing operational efficiency.
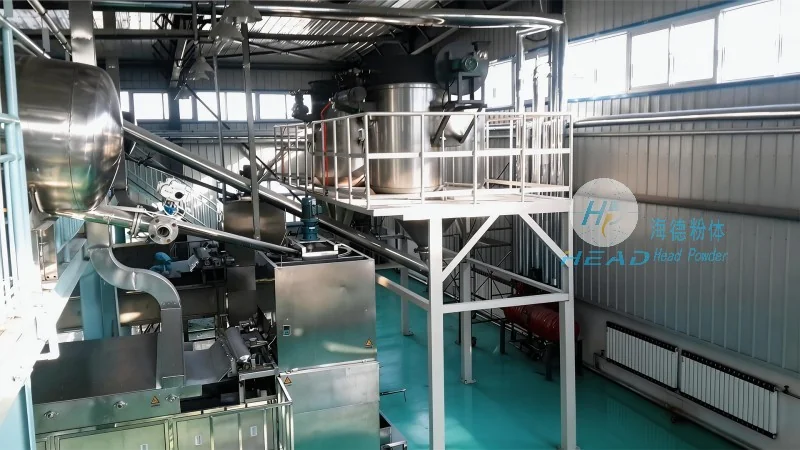
A typical urea granule pneumatic conveyor consists of several core components that work in tandem to facilitate material transport. The primary elements include a hopper for material storage, a conveyor line (either a pipe or a duct), a blower or air compressor to generate the airflow, and a discharge point where the material is released. The hopper is designed to hold a sufficient quantity of urea granules, ensuring a steady supply to the conveyor system. The conveyor line, often made of stainless steel or other corrosion-resistant materials, is engineered to withstand the abrasive nature of urea granules and the effects of air pressure. The blower or air compressor provides the necessary pressure and volume of air to create a consistent flow of material through the system. As the urea granules are introduced into the conveyor line, they are entrained by the airflow and transported to the discharge point. This process can be either positive pressure (where air is pushed through the system) or negative pressure (where air is drawn out, creating a vacuum). The choice of system type depends on factors such as the distance to be covered, the volume of material to be moved, and the specific requirements of the application.
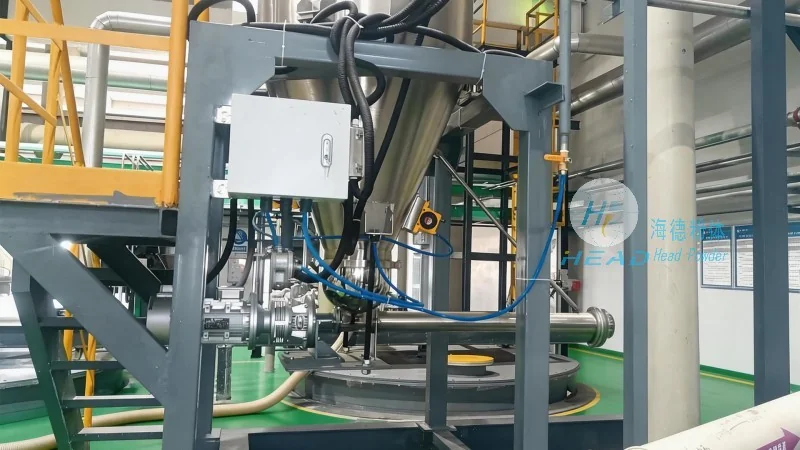
The design of a urea granule pneumatic conveyor involves careful consideration of several engineering principles to ensure optimal performance and durability. One of the most critical aspects is the selection of appropriate materials for the conveyor components. Urea granules are known to be abrasive, and thus, the conveyor line, hopper, and other parts must be constructed from materials that can withstand wear and tear over time. Stainless steel is commonly used due to its corrosion resistance and strength, while other materials like polyethylene or special alloys may be employed in specific applications. Another key design principle is the optimization of airflow. The velocity and pressure of the air must be carefully controlled to prevent material degradation, blockages, or excessive energy consumption. Engineers typically use computational fluid dynamics (CFD) simulations to model the airflow and determine the optimal parameters for the system. Additionally, the system's capacity and efficiency are influenced by the size and shape of the urea granules. Larger or irregularly shaped granules may require higher airflow rates or different conveyor line diameters to ensure smooth transport. The design also considers the need for cleaning and maintenance, with features such as access panels, cleaning ports, and easy-to-remove components to facilitate regular upkeep. Proper sealing and air tightness are essential to prevent leaks and maintain the desired pressure levels within the system.
Urea granule pneumatic conveyors offer several advantages over traditional mechanical conveying methods, making them a preferred choice in many industrial applications. One of the primary benefits is the ability to transport materials over long distances without the need for multiple transfer points or intermediate storage. This reduces the risk of material loss and contamination, as the entire process is contained within the conveyor system. Additionally, pneumatic conveyors can handle materials that are difficult to move using conventional methods, such as those with high moisture content or those that are prone to clumping. The system also provides better control over the material flow rate, allowing for precise dosing and batching. In the fertilizer industry, urea granule pneumatic conveyors are widely used in the production and packaging of urea-based fertilizers. They are employed to transport urea granules from storage silos to processing units, from mixing and granulation stages to packaging lines. The efficiency and reliability of these systems contribute to higher production throughput and lower operational costs. Furthermore, the use of pneumatic conveyors in urea handling reduces the risk of dust explosions, as the material is contained within the system and the air is filtered to remove any particulate matter. This enhances workplace safety and compliance with regulatory standards. The versatility of urea granule pneumatic conveyors also makes them suitable for other industries, such as chemical processing, where similar granular materials need to be transported. Overall, the design and operation of these conveyors play a vital role in improving the efficiency and safety of material handling processes in various industrial sectors.
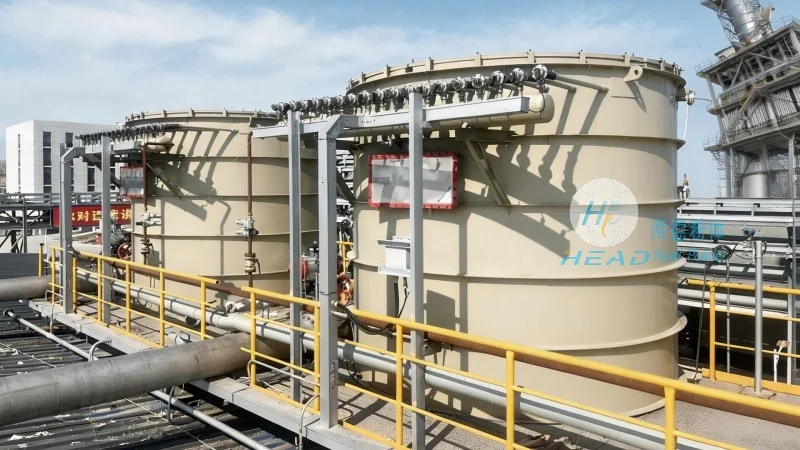
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial conveying equipment, including urea granule pneumatic conveyors. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner in the fertilizer and chemical industries. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel. HeadPowder specializes in designing and producing customized pneumatic conveyor systems tailored to the specific needs of its clients. The company's engineers work closely with customers to understand their operational requirements and provide solutions that enhance productivity and safety. HeadPowder's products are known for their durability, efficiency, and reliability, which are essential for demanding industrial applications. The company adheres to international quality standards and employs rigorous testing procedures to ensure that each conveyor system meets the highest performance criteria. HeadPowder also offers comprehensive after-sales support, including installation, maintenance, and technical assistance, to ensure that its customers can maximize the lifespan and performance of their equipment. By combining expertise in engineering, manufacturing, and customer service, HeadPowder has become a key player in the global market for industrial conveying solutions. The company's commitment to excellence and customer satisfaction has earned it a reputation for delivering reliable and effective urea granule pneumatic conveyors that meet the evolving needs of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top