High-temperature fly ash powder pneumatic conveying systems represent a sophisticated solution for the efficient handling and transportation of high-temperature, fine particulate materials. This technology is crucial in industrial settings where the safe and reliable movement of fly ash, a byproduct of coal combustion, is essential for environmental compliance and operational efficiency. The system operates on the principle of using compressed air or other gas to transport the powder through a network of pipes, ensuring minimal material loss and reduced exposure to contaminants.
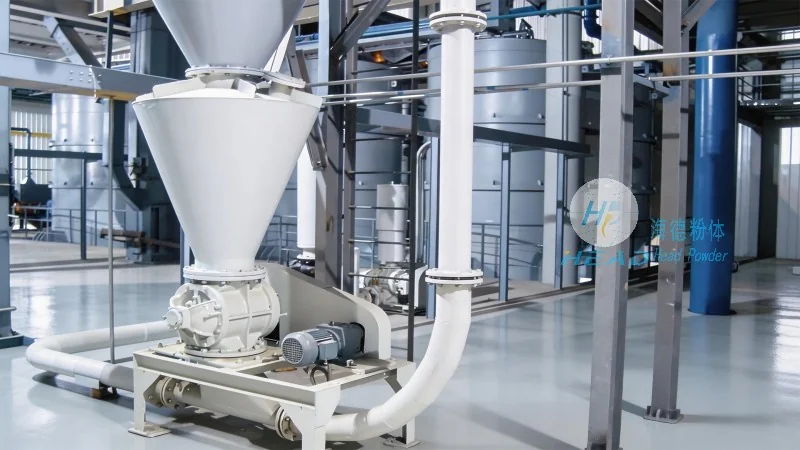
The core of a high-temperature fly ash powder pneumatic conveying system lies in its ability to handle materials at elevated temperatures while maintaining the integrity of the conveying process. The system typically consists of a hopper for material storage, a blower or compressor to generate the necessary air pressure, and a pipeline network that transports the ash from the source to the destination. The key components include a feeder that controls the flow rate of the fly ash into the pipeline, a filter system to capture any fine particles that may escape, and a discharge unit at the receiving end. The operation involves the feeder releasing the fly ash into the pipeline, where it is entrained by the high-velocity air stream. This air-fuel mixture travels through the pipes, with the air providing the kinetic energy needed to move the powder. The system is designed to handle temperatures up to several hundred degrees Celsius, making it suitable for applications where the ash is still hot from the combustion process.
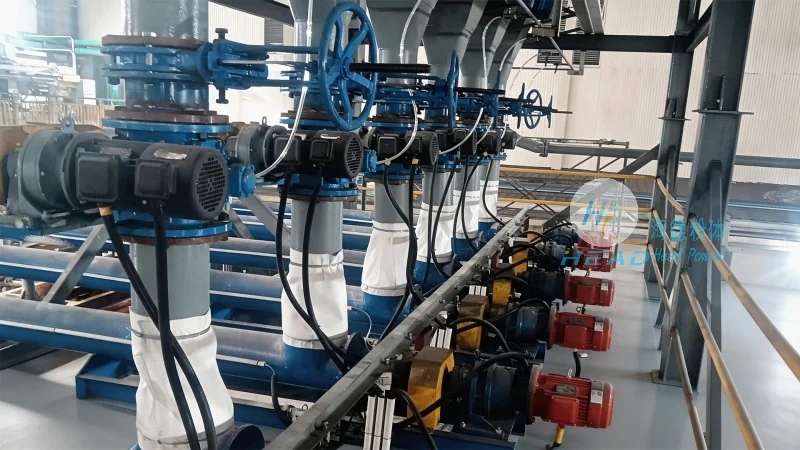
High-temperature fly ash powder pneumatic conveying systems are characterized by their flexibility and adaptability to various industrial environments. They are commonly used in power plants, cement factories, and other facilities that generate large quantities of fly ash. The systems are particularly effective in scenarios where the ash needs to be transported over long distances or to multiple destinations. For instance, in a thermal power plant, the system can transport hot ash from the boiler to a storage silo or to a landfill site. The operational characteristics include high conveying rates, low maintenance requirements, and the ability to handle abrasive materials without significant wear on the equipment. Additionally, the system is designed to minimize dust emissions, which is critical for maintaining air quality and ensuring worker safety. The flexibility of the system allows for easy integration with existing infrastructure, making it a cost-effective solution for upgrading or expanding material handling capabilities.
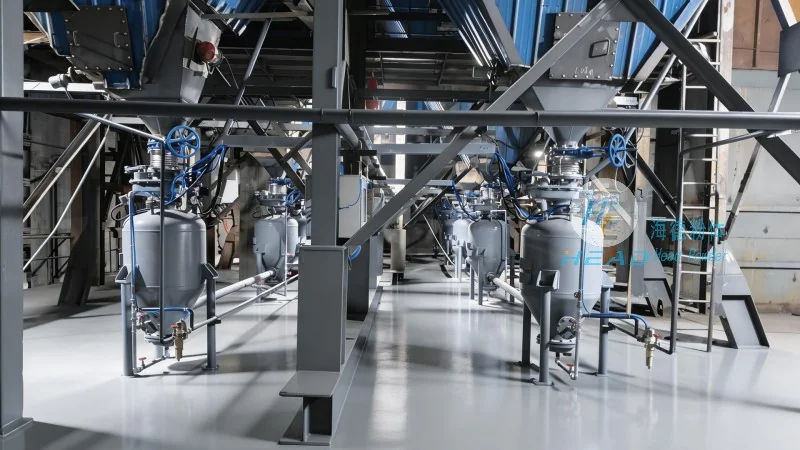
HeadPowder, a leading provider of engineering solutions for material handling, specializes in the design, manufacturing, and installation of high-temperature fly ash powder pneumatic conveying systems. With a strong presence in China, particularly in Shandong province, the company has built a reputation for delivering reliable and efficient systems that meet the stringent requirements of industrial applications. The company's expertise lies in understanding the unique challenges of handling high-temperature fly ash, such as thermal stress on equipment and the need for dust control. By leveraging advanced engineering techniques and high-quality materials, HeadPowder ensures that its systems are durable, efficient, and compliant with environmental regulations. The company's commitment to customer satisfaction is reflected in its comprehensive after-sales support, including maintenance services and technical assistance. HeadPowder's systems are tailored to meet the specific needs of each client, ensuring optimal performance and long-term reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top