For industries dealing with calcium nitrite powders, an efficient and reliable handling system is crucial for maintaining product quality and operational safety. This article explores the concept of a calcium nitrite powder handling system and delves into its fundamental design principles, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. as a leading provider in the field.
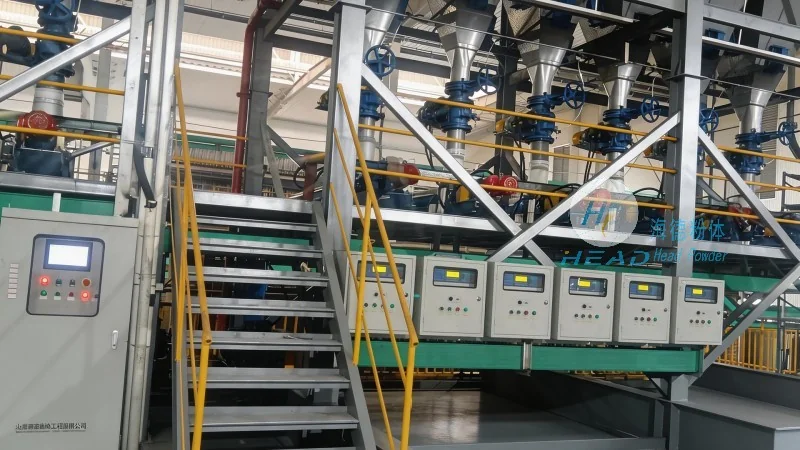
Calcium nitrite is a critical chemical compound widely used in various industrial applications, including water treatment, concrete admixtures, and as a corrosion inhibitor. Handling this powder requires specialized equipment due to its fine particle size and potential reactivity. A calcium nitrite powder handling system is a comprehensive solution designed to manage the storage, transfer, and processing of calcium nitrite powders safely and efficiently. Such systems are essential for ensuring consistent product quality, minimizing dust emissions, and adhering to safety regulations.
HeadPowder, the professional brand under Shandong HeadPowder Engineering Co., Ltd., specializes in the design, manufacturing, and integration of advanced powder handling systems. With a strong presence in China, particularly in Shandong, the company leverages years of industry experience to deliver tailored solutions for diverse industrial needs. The company’s commitment to quality and innovation has established it as a trusted partner for businesses seeking reliable calcium nitrite powder handling solutions.
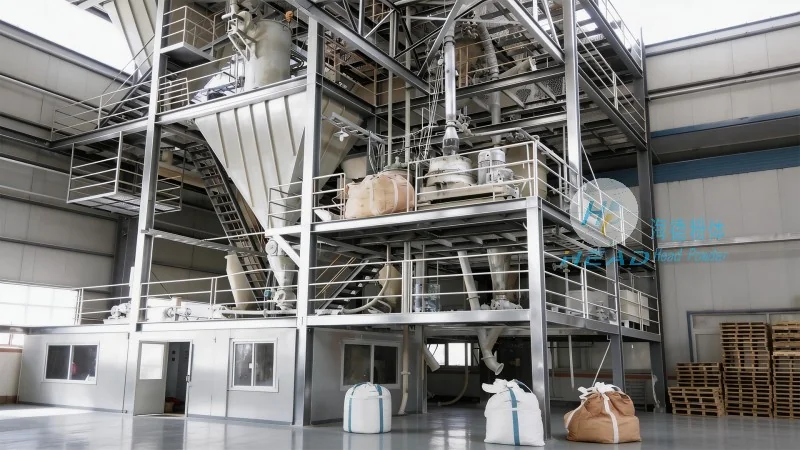
The design of a calcium nitrite powder handling system is guided by several key principles to ensure optimal performance and safety. These principles include: 1. Dust Control and Environmental Protection, as calcium nitrite powders can generate fine dust that poses health risks and environmental concerns. Advanced dust collection systems, such as bag filters or cartridge filters, are integrated into the design to minimize emissions. 2. Material Compatibility, as the system components must withstand the chemical properties of calcium nitrite, including its reactivity and potential moisture absorption. Materials like stainless steel, PTFE, or specialized coatings are used to prevent corrosion and ensure durability. 3. Process Efficiency, which involves optimizing the flow of powders through the system to reduce downtime and improve throughput. This includes the use of appropriate conveyor systems, such as screw conveyors or pneumatic conveyors, and proper hopper design to prevent bridging or caking. 4. Safety and Compliance, which is paramount in handling potentially hazardous powders. The system incorporates safety features like explosion-proof designs, emergency shut-off valves, and proper ventilation to comply with industrial safety standards.
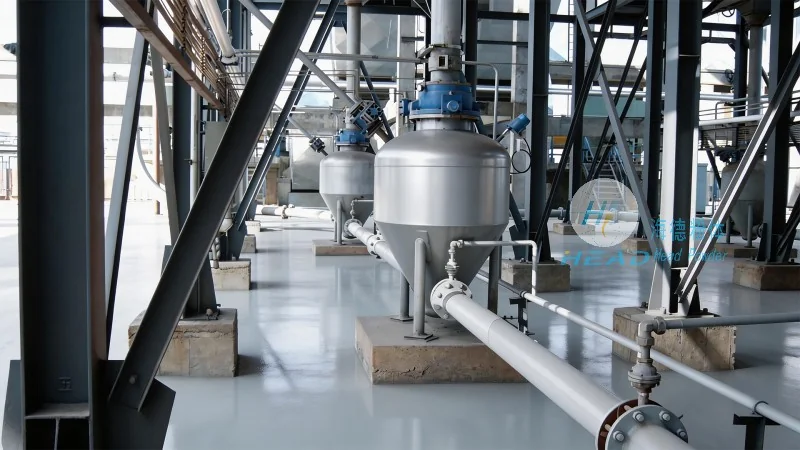
A typical calcium nitrite powder handling system consists of several interconnected components, each playing a vital role in the overall operation. The main components include: 1. Storage Hoppers, which are designed to store the calcium nitrite powder in a controlled environment, often with a conical bottom to facilitate smooth discharge. These hoppers are equipped with level sensors to monitor the powder level and prevent overfilling. 2. Feeding Equipment, such as rotary valves or star feeders, which control the flow of powder from the storage hopper to the conveyor system. These devices ensure a consistent and controlled feed rate, preventing surges or blockages. 3. Conveying Systems, which transport the powder from the storage area to the processing or packaging equipment. Screw conveyors are commonly used for horizontal or vertical transport due to their ability to handle fine powders without clogging. Pneumatic conveyors may also be employed for longer distances or when high dust control is required. 4. Dust Collection Systems, which capture and filter the airborne powder particles to protect the environment and personnel. These systems typically include a hopper, filter cartridges, and a fan to create the necessary airflow. 5. Processing or Packaging Equipment, which may include mixers, blenders, or packaging machines, depending on the application. These components are integrated into the system to complete the powder handling process.
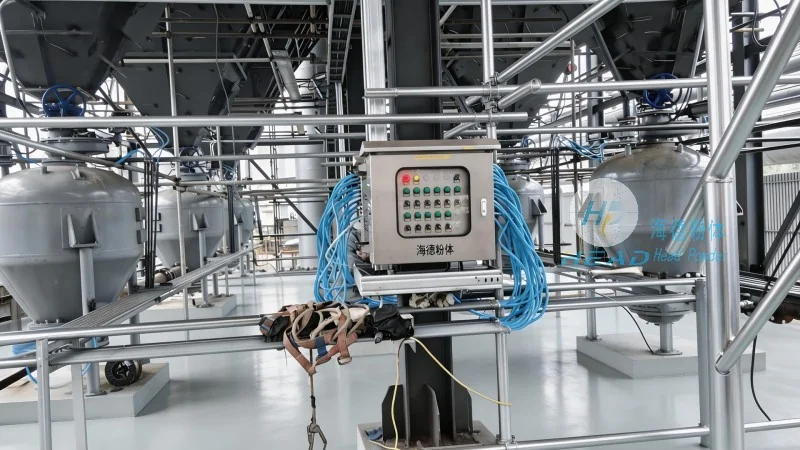
The calcium nitrite powder handling system developed by Shandong HeadPowder Engineering Co., Ltd. is designed to meet the specific requirements of various industrial applications. The system offers several benefits, including: 1. Enhanced Product Quality, as the controlled handling process minimizes contamination and ensures consistent particle size distribution. 2. Improved Safety, with features like dust control and explosion-proof designs that reduce the risk of accidents. 3. Increased Efficiency, through optimized flow and reduced downtime, leading to higher productivity. 4. Cost Savings, by minimizing material waste and reducing maintenance costs due to the durable components used in the system. These benefits make the calcium nitrite powder handling system an essential investment for industries relying on calcium nitrite for their operations.
In conclusion, a calcium nitrite powder handling system is a sophisticated and essential solution for industries dealing with this critical chemical compound. The design principles, components, and applications of such systems are tailored to ensure safety, efficiency, and product quality. With its expertise and commitment to excellence, Shandong HeadPowder Engineering Co., Ltd. provides reliable and effective calcium nitrite powder handling systems that meet the diverse needs of its clients. By understanding the design principles and components of these systems, businesses can make informed decisions to enhance their operational performance and ensure compliance with industry standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top