HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. Among their portfolio is the sodium bicarbonate powder pneumatic conveying system, a technology that efficiently transports bulk powders like sodium bicarbonate through a pressurized air stream. This system is engineered to meet the specific demands of industrial applications, ensuring reliable and efficient material transfer.
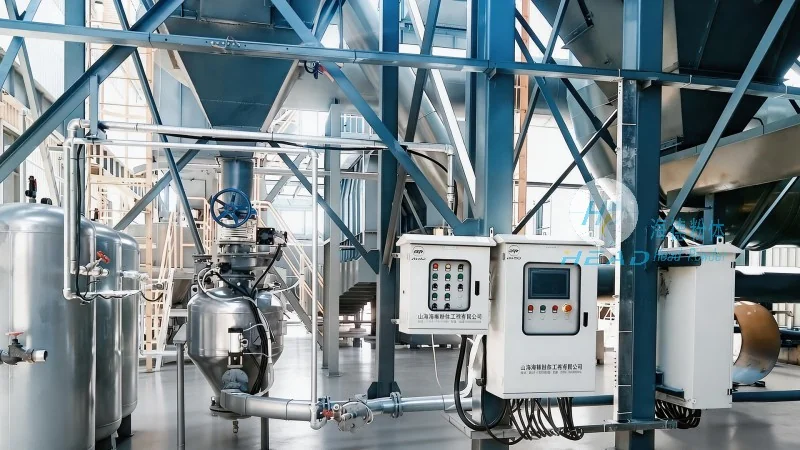
The core principle of the sodium bicarbonate powder pneumatic conveying system revolves around the use of compressed air to move dry powder materials. The system operates by creating a pressure differential between the conveying line and the ambient environment. As compressed air is introduced into the system, it lifts and propels the powder particles through the pipeline. The design incorporates key components such as a feeder, a conveying line, and a receiver, all working in tandem to ensure smooth material flow. The system's efficiency is enhanced by optimizing air velocity and pressure to match the specific characteristics of sodium bicarbonate powder, including its particle size, density, and flowability. This approach minimizes product degradation and ensures consistent performance across various operational conditions.
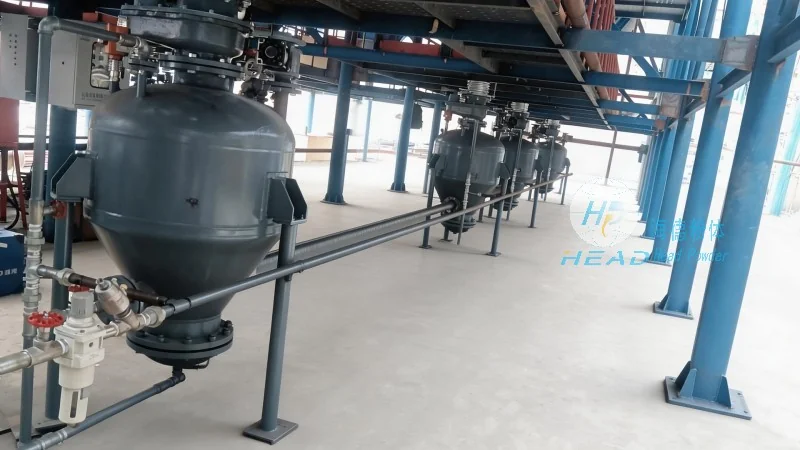
The working scene characteristics of the sodium bicarbonate powder pneumatic conveying system are tailored to the unique requirements of industrial environments. These systems are typically deployed in manufacturing facilities, chemical processing plants, and food processing operations where sodium bicarbonate is used as a raw material or additive. The system's design accommodates the need for clean, dust-free transfer, which is critical in industries such as pharmaceuticals and food processing. Additionally, the system is built to handle varying production volumes, from continuous high-volume operations to intermittent batch processing. The flexibility of the system allows it to integrate seamlessly with existing production lines, reducing downtime and improving overall operational efficiency. The working environment is characterized by precise control over air pressure and flow rates, ensuring that the powder is conveyed without clogging or degradation. This makes the system suitable for applications where product quality and purity are paramount.
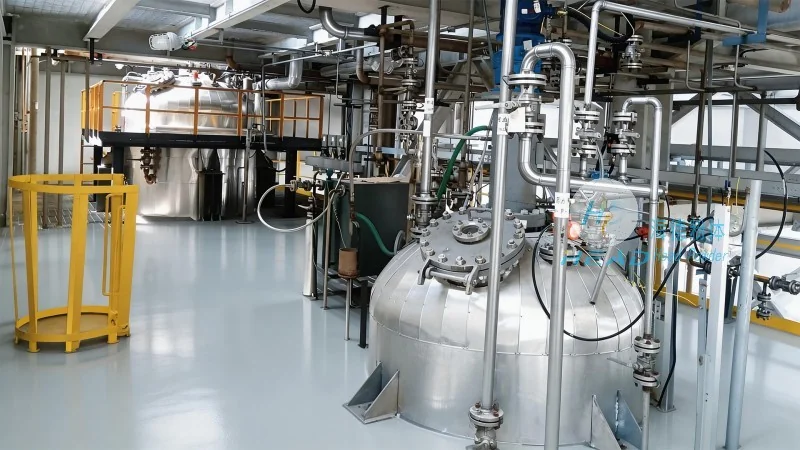
Implementing a sodium bicarbonate powder pneumatic conveying system offers several advantages in industrial settings. Firstly, it provides a dust-free and hygienic transfer method, which is essential in food and pharmaceutical industries where contamination control is non-negotiable. The system eliminates the need for manual handling, reducing labor costs and improving workplace safety. Furthermore, the automated nature of the system enhances operational efficiency by minimizing human intervention and ensuring consistent material flow. The system's compact design allows for easy integration into existing facilities, making it a cost-effective solution for upgrading or expanding material handling capabilities. In addition, the system's ability to handle varying particle sizes and flow properties of sodium bicarbonate makes it versatile for different production processes. Overall, the system contributes to improved productivity, reduced maintenance costs, and enhanced product quality, making it a valuable asset for industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top