Understanding the role of catalyst powder handling systems is crucial in industries where catalysts are essential for chemical reactions. These systems are engineered to safely and efficiently transport catalyst powders, which are often used in processes like catalytic cracking, hydrogenation, and polymerization. The design of such systems must address challenges like dust generation, material segregation, and the need for precise dosing, ensuring optimal performance and safety in industrial applications.
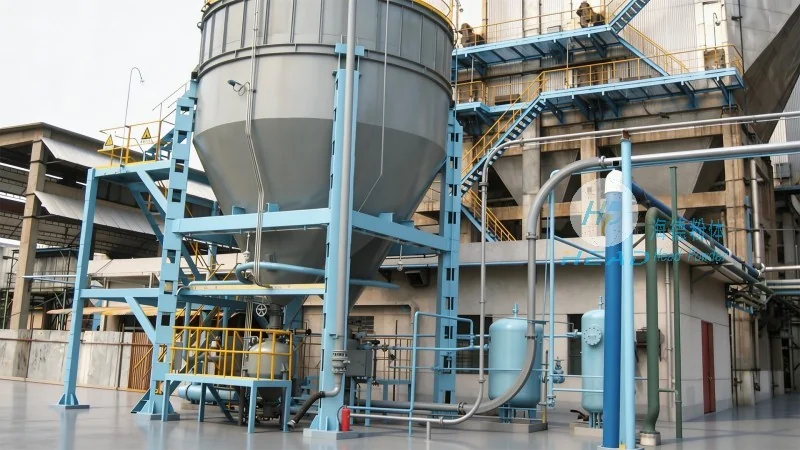
A typical catalyst powder handling system consists of several critical components that work in tandem to ensure reliable operation. These include feed hoppers, which store and feed the catalyst powder; conveying equipment such as screw conveyors, pneumatic conveying systems, or bulk material handling equipment; and control systems that regulate the flow and dosage. Each component is designed to minimize material degradation and prevent contamination, which are critical factors in maintaining catalyst effectiveness.
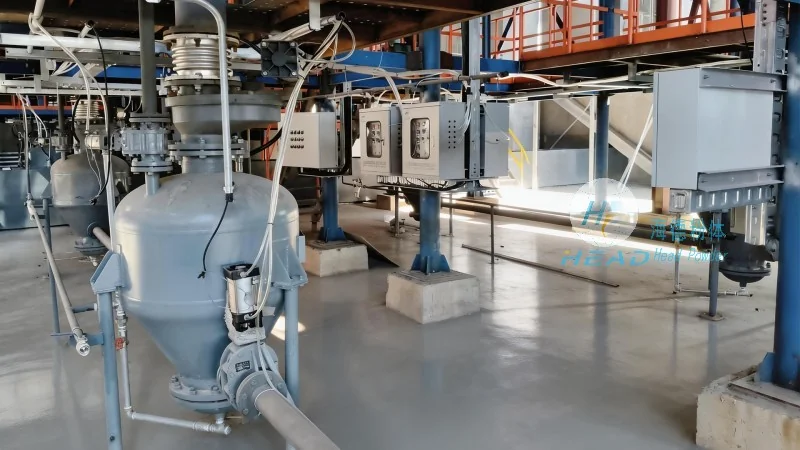
The design principles of a catalyst powder handling system focus on several key aspects to ensure efficiency, safety, and longevity. One of the primary principles is the prevention of dust generation and inhalation risks, which is achieved through enclosed systems and proper ventilation. Another critical principle is the reduction of material segregation, as catalysts can vary in particle size and density, and segregation can lead to inconsistent performance. The system must also be designed for easy maintenance and cleaning to prevent cross-contamination between batches. Additionally, precise dosing mechanisms are essential to control the amount of catalyst added to the reaction, which directly impacts the efficiency and yield of the process.
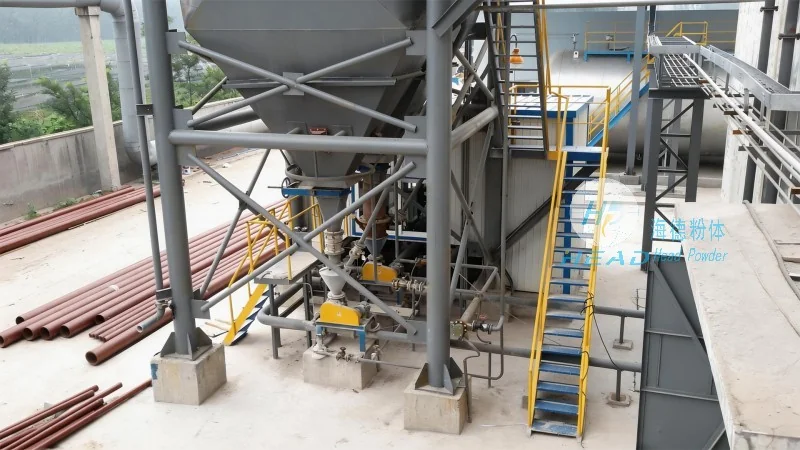
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, specializes in designing and manufacturing catalyst powder handling systems tailored to the specific needs of various industries. With a focus on innovation and customer-centric solutions, HeadPowder leverages advanced engineering techniques to develop systems that meet the highest standards of safety, efficiency, and reliability. The company's expertise lies in understanding the unique challenges of catalyst powders, such as their sensitivity to moisture and air, and designing systems that address these challenges effectively. By integrating state-of-the-art technologies and adhering to strict quality control measures, HeadPowder ensures that its systems deliver optimal performance and contribute to the success of industrial processes.
Catalyst powder handling systems are widely used in industries such as petrochemical, pharmaceutical, and fine chemicals, where catalysts play a vital role in production processes. The benefits of these systems include improved process control, reduced material waste, and enhanced safety for operators. By ensuring consistent and precise delivery of catalysts, these systems help maintain the quality and efficiency of chemical reactions, leading to higher product yields and lower operational costs. Furthermore, the enclosed design of modern systems minimizes environmental impact by preventing dust emissions and protecting the surrounding environment.
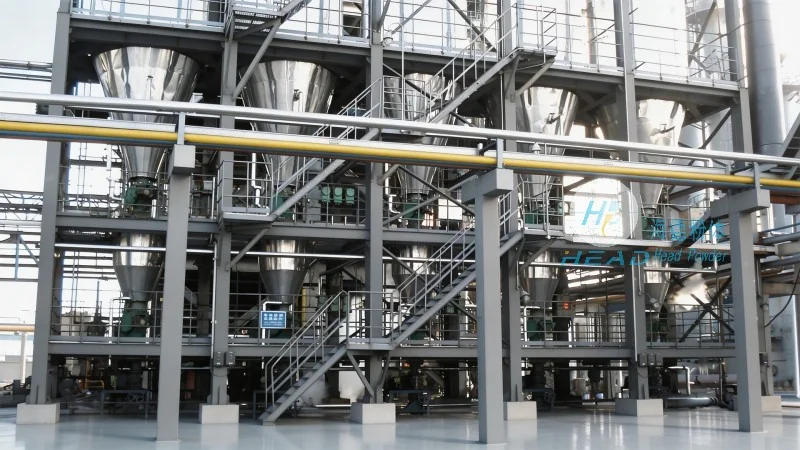
In conclusion, catalyst powder handling systems are indispensable in industries that rely on catalysts for their production processes. The design principles and components of these systems are carefully engineered to address the unique challenges of catalyst powders, ensuring safe, efficient, and reliable operation. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in providing advanced solutions that meet the evolving needs of the industry, contributing to the advancement of chemical processes and the overall success of industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top