When it comes to efficient and reliable material handling in industrial settings, the use of pneumatic conveying systems has become increasingly prevalent. Among these, the purified powder body pneumatic conveying equipment stands out as a specialized solution designed to handle fine powders with high precision and minimal contamination. This equipment is engineered by Shandong HeadPowder Engineering Co., Ltd. (headpowder), a leading manufacturer based in Shandong, China, to ensure that the material being transported remains clean and free from external pollutants, making it ideal for applications where product purity is paramount.
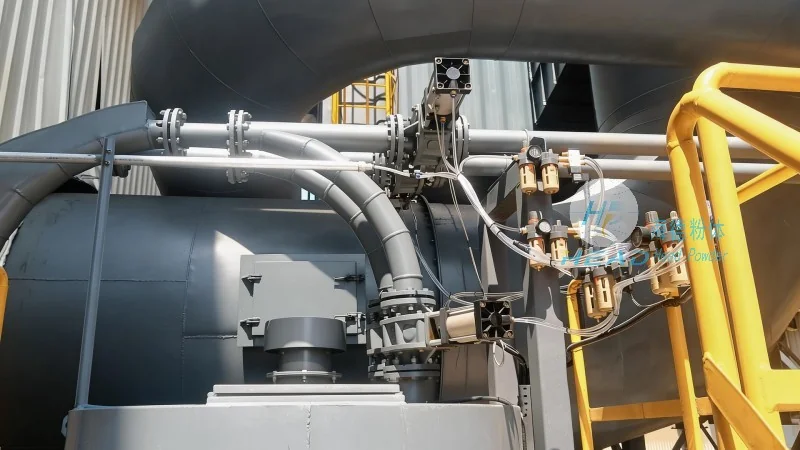
The core principle behind this equipment is the use of compressed air or other gases to transport dry powders through a closed pipeline system. Unlike traditional methods that may involve mechanical components like screws or belts, pneumatic conveying relies on the kinetic energy of the gas to move the material. The system typically consists of a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver to collect the material at the destination. The key to its effectiveness lies in maintaining a consistent air-to-material ratio, which ensures that the powder is transported smoothly without clogging or degradation.
One of the critical aspects of the purification process is the incorporation of filtration and separation mechanisms. These components are designed to remove any airborne particles or moisture that could contaminate the powder during transport. For instance, cyclone separators and bag filters are commonly used to capture fine particles, while moisture sensors and dehumidifiers help maintain the material's dryness. This dual approach of conveying and purifying simultaneously ensures that the final product meets stringent quality standards, which is essential in industries such as pharmaceuticals, food processing, and high-purity chemicals.
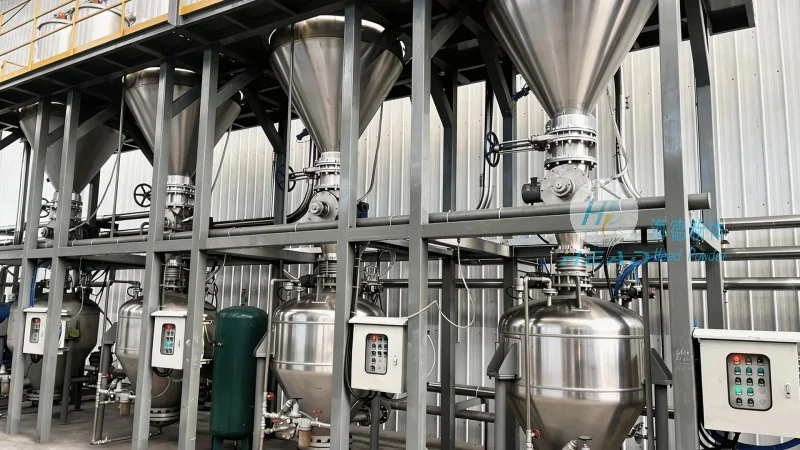
The working scene characteristics of purified powder body pneumatic conveying equipment are tailored to meet the diverse needs of modern industrial operations. These systems are particularly well-suited for applications where material handling requires both speed and cleanliness. For example, in pharmaceutical manufacturing, where the purity of raw materials directly impacts the quality of the final drug, this equipment provides a sterile and controlled environment for powder transfer. Similarly, in the food industry, where hygiene and product safety are non-negotiable, the sealed system prevents cross-contamination and maintains the integrity of the product.
In addition to pharmaceuticals and food, the equipment is widely used in chemical processing, where handling reactive or sensitive powders demands precision. The ability to control the flow rate and pressure within the system allows for safe and efficient transfer of materials, reducing the risk of accidents or material loss. Furthermore, the flexibility of pneumatic conveying systems enables them to be integrated into existing production lines, minimizing downtime and enhancing overall operational efficiency.
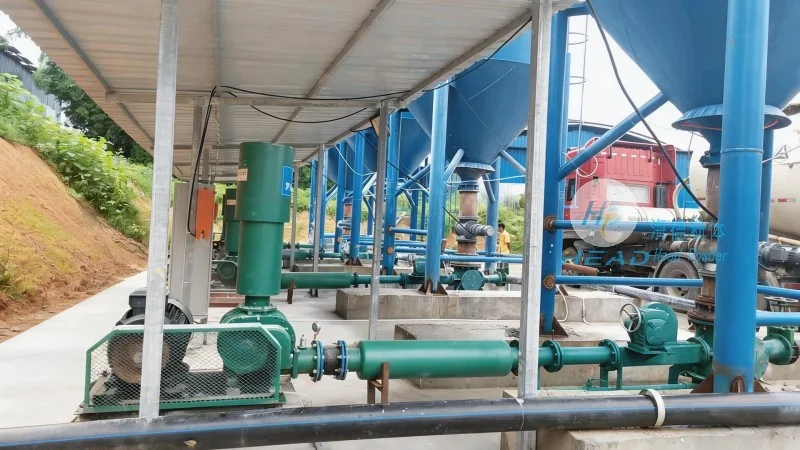
When considering the working scene characteristics, several advantages become apparent. The equipment's ability to handle fine powders without the need for additional mechanical components reduces maintenance costs and operational downtime. The sealed pipeline design also minimizes dust emissions, contributing to a safer working environment and compliance with environmental regulations. In industries where material purity is a critical factor, such as in the production of fine chemicals or specialty foods, the purified powder body system offers a competitive edge by ensuring that the material remains uncontaminated throughout the entire conveying process.
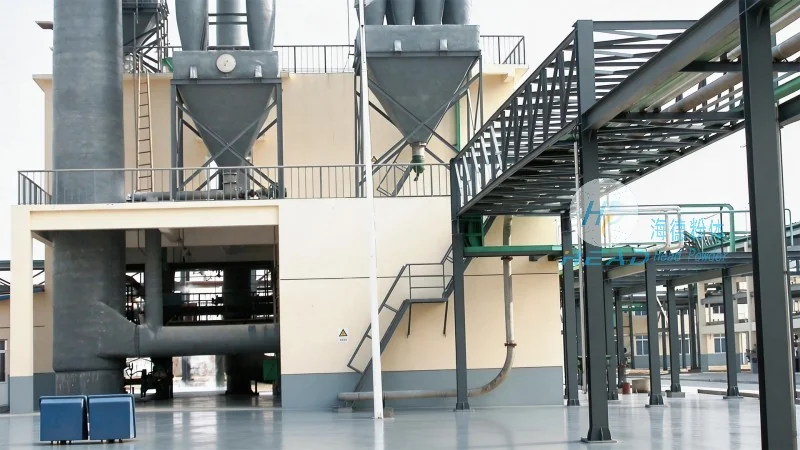
Another key advantage is the scalability of these systems. Whether for small-scale laboratory applications or large-scale industrial production, the equipment can be customized to meet specific throughput requirements. This adaptability makes it suitable for a wide range of applications, from research and development to full-scale manufacturing. The consistent performance of the system, combined with its low maintenance requirements, provides long-term cost savings and reliability for businesses operating in demanding environments.
In conclusion, the purified powder body pneumatic conveying equipment represents a sophisticated solution for handling fine powders in industrial settings. By integrating principles of pneumatic transport with advanced purification technologies, this equipment ensures that materials are transferred efficiently while maintaining the highest standards of purity. The working scene characteristics, which include adaptability, safety, and efficiency, make it an indispensable tool for industries where product quality and operational reliability are paramount. As businesses continue to seek innovative solutions for material handling, the role of such specialized equipment will only grow, underscoring its importance in modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top