HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for river sand powder applications. With a focus on efficient material handling solutions, the company leverages its expertise to address the unique challenges associated with transporting fine river sand particles through air-based systems.
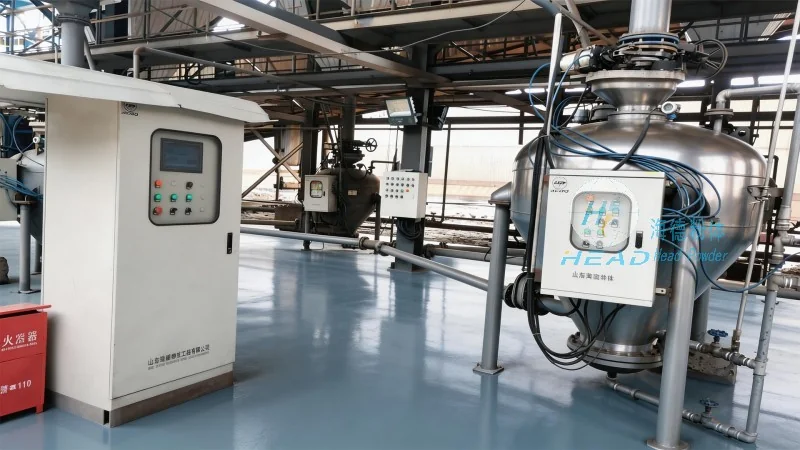
The pneumatic conveying system for river sand powder operates on the fundamental principle of using air as the medium to transport solid particles. This technology, commonly known as air conveying, can be categorized into two primary types: positive pressure and negative pressure systems. In positive pressure systems, air is forced through the pipeline at a pressure higher than the ambient air, propelling the sand particles forward. Conversely, negative pressure systems create a vacuum in the pipeline, drawing the sand particles into the system. For river sand, which often contains fine and abrasive particles, the choice of system type depends on factors such as the distance of transport, particle size distribution, and the required flow rate. The system typically includes key components like a hopper for material storage, a rotary valve for controlled discharge, a conveying pipeline, a fan or blower for air supply, and a receiver for the delivered material. The design of these components is critical to ensure efficient and reliable operation, minimizing particle degradation and system wear.
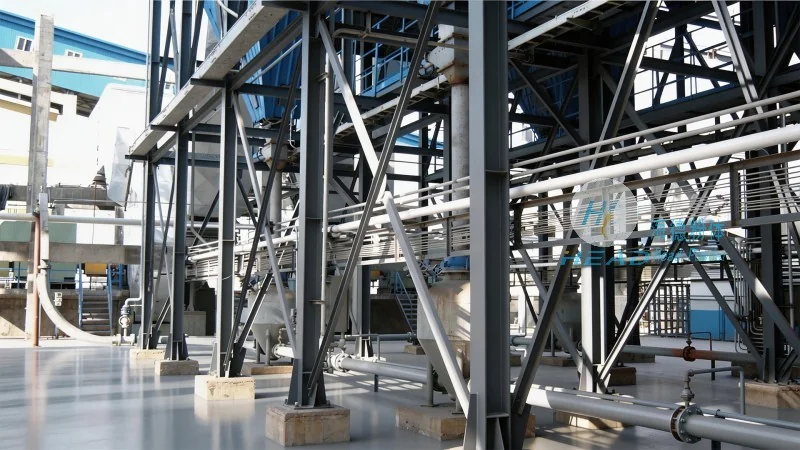
The working scene characteristics of river sand powder pneumatic conveying systems are shaped by the diverse industrial and construction applications where this technology is employed. One of the primary scenarios involves the transportation of sand from mining sites to processing facilities, such as concrete mixing plants or cement production lines. In these cases, the system must handle large volumes of sand over considerable distances, often requiring high-capacity positive pressure systems to maintain consistent flow rates and prevent blockages. Another common application is in the construction sector, where sand is transported from storage silos to job sites for concrete and mortar production. Here, the system may need to accommodate varying particle sizes and moisture content, necessitating adjustable air flow and pressure controls to ensure smooth operation. Additionally, the system is used in industrial processes that involve sand as a raw material, such as in the manufacturing of glass or ceramics, where precise control over particle size and purity is essential. The working scene characteristics also include considerations for environmental factors, such as dust control and noise reduction, as pneumatic conveying systems can generate significant airborne particles and operational noise. To mitigate these issues, modern systems incorporate dust collection and filtration systems, as well as noise dampening components, ensuring compliance with environmental regulations and providing a safer working environment.
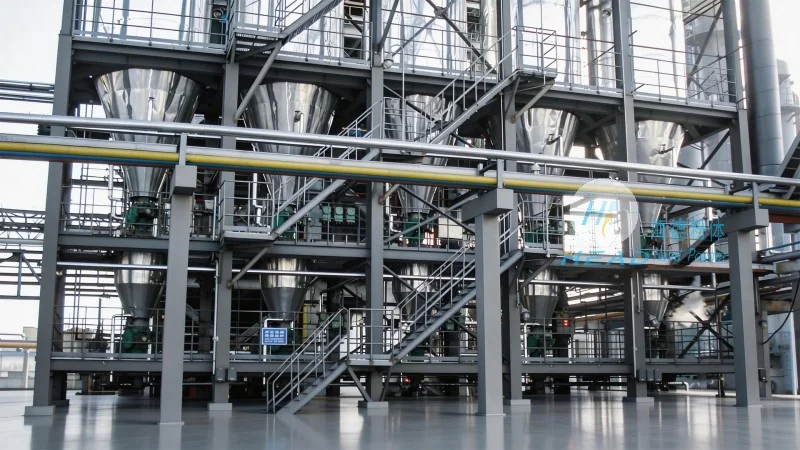
Implementing a pneumatic conveying system for river sand offers several advantages that make it a preferred choice over traditional methods like belt conveyors or bucket elevators. One of the most significant benefits is the ability to transport fine and abrasive particles without the need for mechanical contact, which reduces wear on equipment and extends the lifespan of components. This is particularly important for river sand, which often contains sharp edges and high silica content that can cause rapid wear on metal surfaces. Another advantage is the flexibility in system design, allowing for horizontal, vertical, or mixed (horizontal-vertical) configurations to suit the specific layout of the facility. This adaptability enables the system to navigate complex layouts and integrate seamlessly with existing infrastructure. Furthermore, pneumatic conveying systems provide high efficiency in material handling, with the ability to transport large volumes of sand at high speeds, reducing overall processing time and increasing productivity. The system also offers better control over the flow rate and pressure, allowing for precise regulation of the material being conveyed. However, technical considerations must be addressed to ensure optimal performance. For instance, the system must be designed to handle the specific properties of river sand, including its particle size distribution, moisture content, and density. Proper sizing of the conveying pipeline, fan capacity, and air velocity is crucial to prevent particle segregation, blockages, or excessive pressure drops. Regular maintenance and monitoring of system components, such as the fan, rotary valve, and pipeline, are also essential to maintain efficiency and avoid downtime. Additionally, the system should be equipped with safety features, such as pressure relief valves and dust suppression systems, to ensure safe operation and protect against potential hazards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top