HeadPowder, a leading engineering firm based in Shandong, China, specializes in the application and optimization of pneumatic conveying systems for transporting dicalcium phosphate (DCP). This technology is crucial for efficient material handling in the fertilizer and feed industries, where DCP is a key ingredient. The following content explores the practical implementation and benefits of such systems, highlighting how they enhance operational efficiency and reliability.
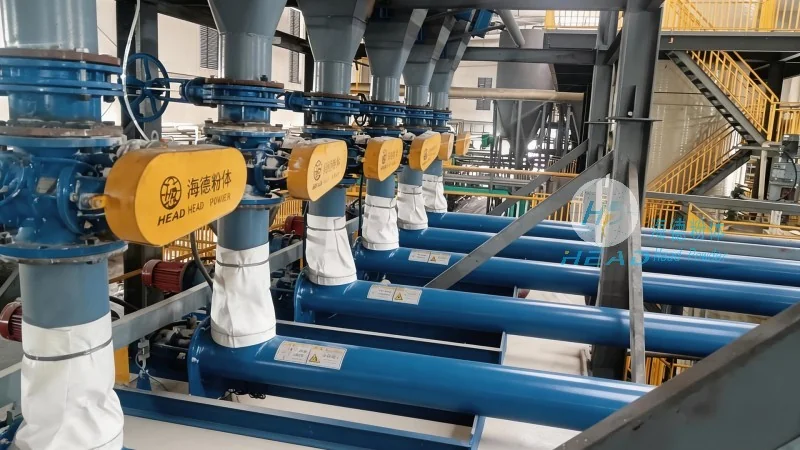
Dicalcium phosphate, commonly used as a feed additive and fertilizer component, presents unique challenges during transport due to its granular nature and varying moisture content. Traditional methods like belt conveyors or bucket elevators may suffer from material buildup, clogging, and increased maintenance costs. Pneumatic conveying offers a solution by using air pressure to move materials through pipelines, eliminating the need for mechanical contact and reducing the risk of contamination. This approach is particularly advantageous for DCP, which can be sensitive to moisture and temperature changes.
HeadPowder’s pneumatic conveying systems are designed with several key features to ensure optimal performance for DCP transport. These include high-pressure air pumps, flexible hose or rigid pipe configurations, and specialized material handling components such as rotary valves and airlocks. The systems are equipped with advanced control panels that allow for real-time monitoring of pressure, flow rate, and material level, enabling operators to adjust parameters dynamically. Additionally, the use of inert gases or controlled air flow helps maintain the quality of DCP by preventing oxidation or degradation during transport.
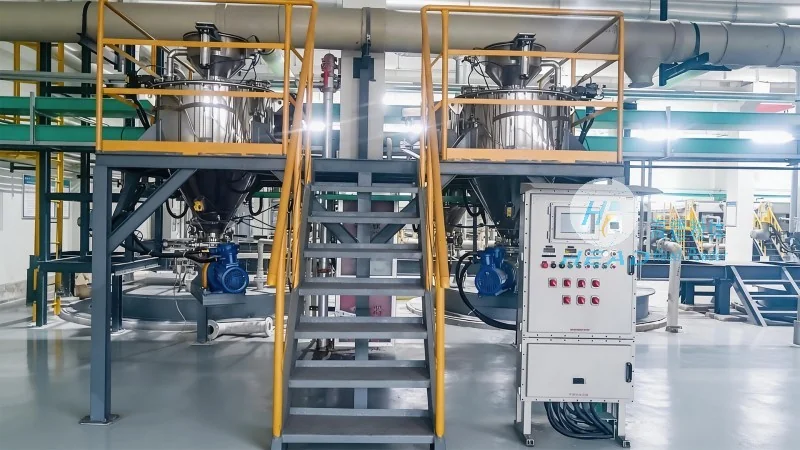
Optimizing pneumatic conveying systems involves several strategies tailored to DCP’s properties. One key approach is the selection of appropriate air velocity and pressure to ensure consistent material flow without causing excessive wear on the system components. HeadPowder employs computational fluid dynamics (CFD) simulations to model the behavior of DCP particles in the conveying pipeline, allowing for precise tuning of system parameters. Another optimization strategy is the integration of pre-drying or moisture control equipment upstream of the conveying system, which helps maintain DCP’s stability and reduces the risk of clogging. Furthermore, the use of pulse-jet cleaning systems in the pipelines ensures that any accumulated material is removed regularly, maintaining system efficiency over time.
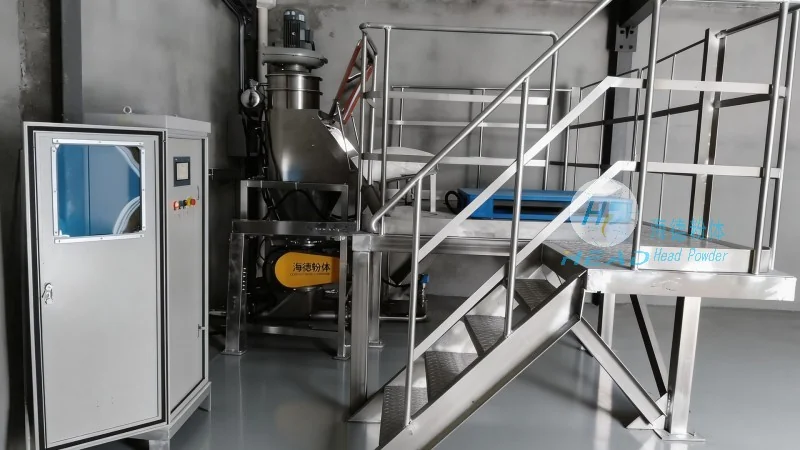
A recent project by HeadPowder involved the installation of a pneumatic conveying system for DCP transport in a large fertilizer plant in Shandong. The plant previously relied on a bucket elevator system that experienced frequent clogs and required daily maintenance. After the installation of the pneumatic conveying system, the plant reported a 40% reduction in downtime and a 25% decrease in maintenance costs. The system’s ability to handle varying DCP feed rates and moisture levels was particularly effective, as the plant’s production schedule required frequent adjustments. The success of this project demonstrates the practical benefits of optimized pneumatic conveying technology for DCP transport.
HeadPowder’s expertise in pneumatic conveying technology for Dicalcium Phosphate transport has proven to be a valuable asset for industries relying on efficient material handling. By combining advanced engineering solutions with practical optimization strategies, the company helps clients achieve higher operational efficiency, reduced costs, and improved product quality. As the demand for DCP continues to grow, the application of optimized pneumatic conveying systems will remain a critical component in ensuring reliable supply chains. HeadPowder remains committed to developing innovative solutions that address the unique challenges of DCP transport, providing sustainable and effective solutions for its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top