Chocolate processing facilities often rely on specialized equipment to handle the delicate and viscous nature of chocolate products. Among these, the chocolate pneumatic conveyor stands out as a critical component for efficient material transport. This article delves into what a chocolate pneumatic conveyor is and the underlying design principles that make it effective in chocolate production environments.
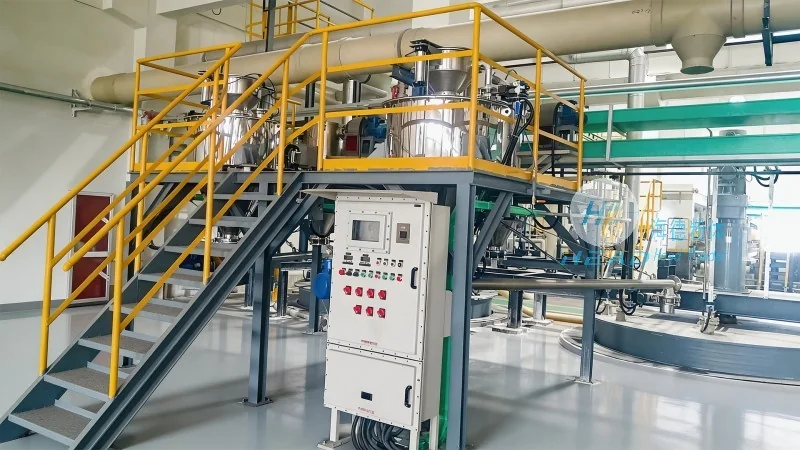
A chocolate pneumatic conveyor is a type of bulk material handling system that uses air pressure to move chocolate or other powders and granules from one location to another. Unlike traditional mechanical conveyors, which rely on belts or screws, pneumatic conveyors utilize a sealed pipeline system where air (or a mixture of air and other gases) propels the material. This method is particularly advantageous in chocolate processing because it minimizes product contamination, preserves product quality, and reduces the risk of mechanical damage to the delicate chocolate particles. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of specialized material handling equipment, specializes in designing and manufacturing such systems to meet the stringent requirements of the chocolate industry.
The effectiveness of a chocolate pneumatic conveyor is rooted in several key design principles that ensure optimal performance and product integrity. First, the system must maintain a consistent air flow rate to achieve reliable material transport. This is typically achieved through the use of positive displacement blowers or rotary lobe pumps, which provide a steady pressure differential across the conveyor line. Second, the conveyor’s design must account for the specific properties of chocolate, such as its density, moisture content, and flow characteristics. For instance, the pipeline diameter and air velocity are carefully selected to prevent product degradation or blockages. Third, the system incorporates features like cyclone separators and filters to separate air from the conveyed material, ensuring that the chocolate remains clean and free from contaminants. Additionally, the use of stainless steel or food-grade materials in the construction of the conveyor components is essential to meet hygiene standards and prevent cross-contamination in food processing environments.
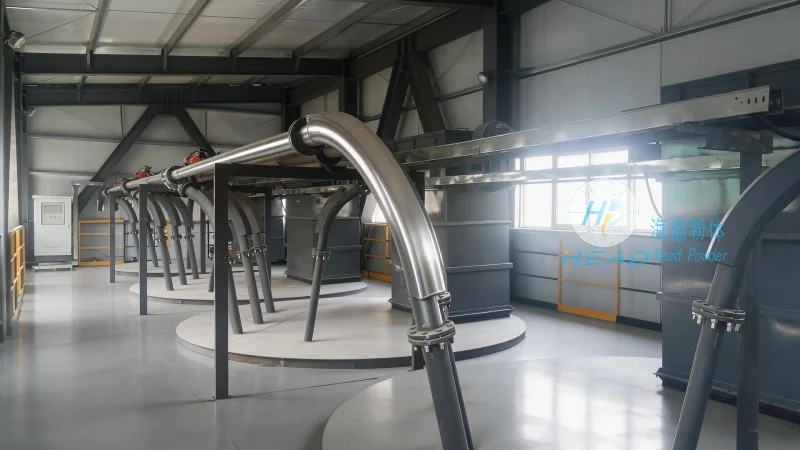
The chocolate pneumatic conveyor consists of several interconnected components that work in tandem to facilitate material transport. The primary components include the air supply unit (such as a blower or compressor), the conveyor line (usually made of stainless steel or food-grade plastic), and the material inlet and outlet points. The operation begins when the air supply unit generates a pressure differential, drawing chocolate from the source (e.g., a hopper or storage bin) into the conveyor line. As the air flows through the pipeline, it carries the chocolate particles along, depositing them at the destination point (e.g., a mixing tank or packaging machine). The system may also include control valves and sensors to regulate the air flow and monitor the material level, ensuring smooth and efficient operation.
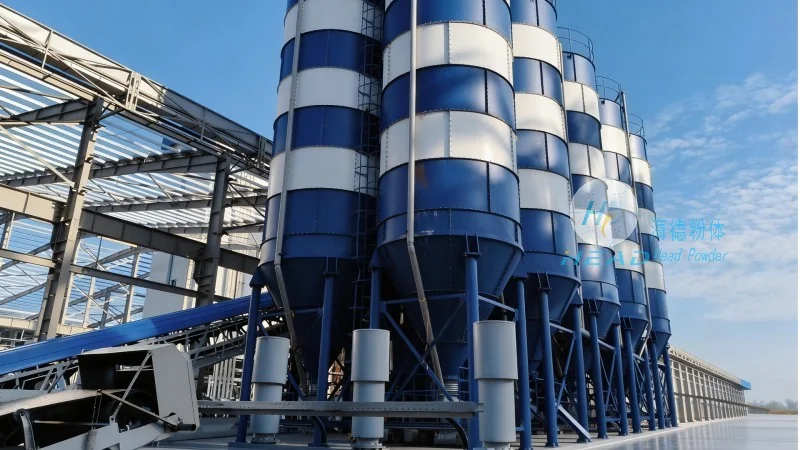
Implementing a chocolate pneumatic conveyor in a processing facility offers numerous benefits that enhance operational efficiency and product quality. One of the most significant advantages is the reduction in labor costs, as the system automates the material handling process, eliminating the need for manual loading and unloading. Additionally, the enclosed design minimizes dust and product loss, improving overall hygiene and reducing waste. The system also allows for flexible routing, enabling chocolate to be transported over long distances or around obstacles without the need for additional infrastructure. Furthermore, the gentle handling of chocolate particles reduces the risk of breakage or clumping, which can affect the final product’s texture and appearance. These benefits make the chocolate pneumatic conveyor an essential tool for modern chocolate manufacturers seeking to optimize their production processes.
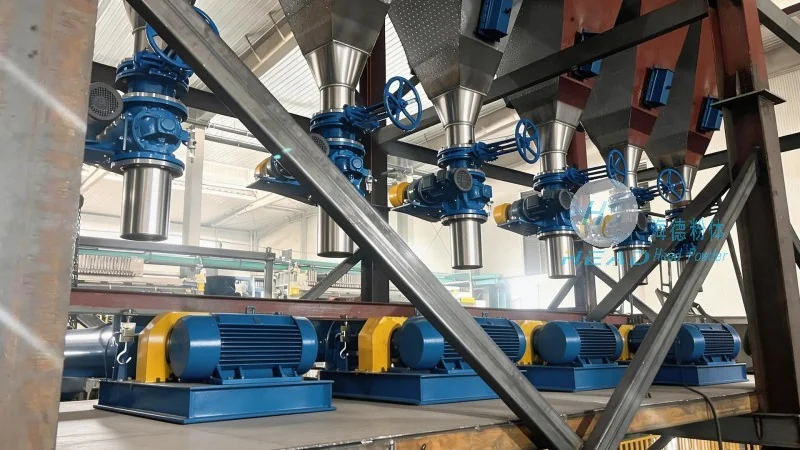
Chocolate pneumatic conveyors are widely used in various stages of chocolate production, from raw material handling to final product packaging. In the initial stages, the system can transport cocoa beans, cocoa powder, or sugar from storage silos to processing equipment. During the conching and tempering processes, the conveyor may be used to move chocolate masses between tanks or to feed them into molding machines. In the final stages, the conveyor can transport finished chocolate products to packaging lines or storage areas. The versatility of the system makes it suitable for both small-scale artisanal chocolate makers and large-scale industrial production facilities, adapting to different production volumes and product types.
Chocolate pneumatic conveyors are sophisticated systems designed to efficiently and hygienically transport chocolate and related materials in food processing environments. By leveraging air pressure and careful engineering, these conveyors ensure product integrity, minimize contamination, and enhance operational efficiency. The design principles, components, and benefits outlined in this article highlight the importance of selecting and maintaining a high-quality chocolate pneumatic conveyor for any chocolate production facility. As the demand for high-quality chocolate products continues to grow, the role of such equipment in optimizing production processes becomes increasingly critical.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top