For industries dealing with bulk materials like salt, efficient and reliable material handling equipment is crucial. One such equipment is the salt pneumatic conveyor, a system designed to transport granular materials like salt through a pipeline using air pressure. This article explores what a salt pneumatic conveyor is and the key design principles that make it effective for salt transportation.
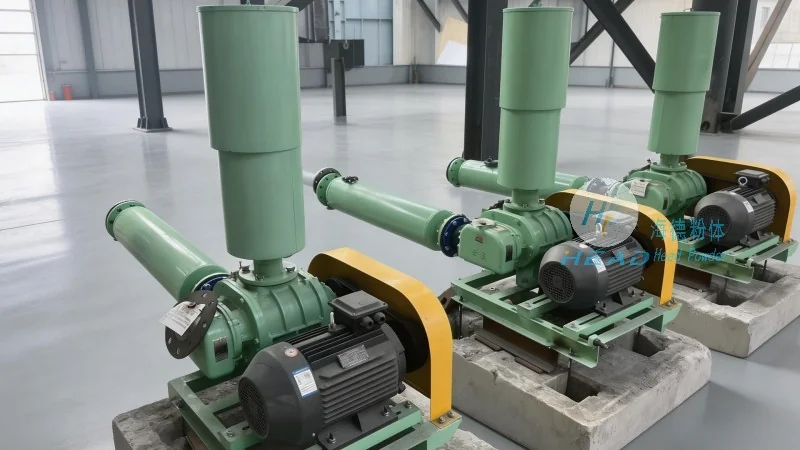
A salt pneumatic conveyor is a type of pneumatic conveying system specifically engineered for transporting salt or similar granular materials. Unlike traditional mechanical conveyors that rely on belts or chains, this system uses compressed air to move the material through a sealed pipeline. The process involves generating a pressure differential within the pipeline, which draws the salt particles into the air stream and propels them to the destination. This method offers several advantages, including the ability to transport materials over long distances, vertical or horizontal movement, and the elimination of contact between the material and the conveyor components, reducing contamination risks.
The design of a salt pneumatic conveyor is based on several critical principles to ensure optimal performance and efficiency. First, the system must maintain a consistent air flow rate to ensure the salt particles are adequately suspended and transported. This involves selecting appropriate air compressors and control systems that can handle the material's specific characteristics, such as particle size, density, and moisture content. Second, the pipeline design is crucial. The diameter and length of the pipeline, along with the inclusion of bends and elbows, must be carefully calculated to minimize pressure drop and prevent material blockages. For salt, which can be abrasive, the pipeline material is typically chosen for durability, often using stainless steel or other corrosion-resistant materials to withstand the chemical properties of the salt and prevent wear.
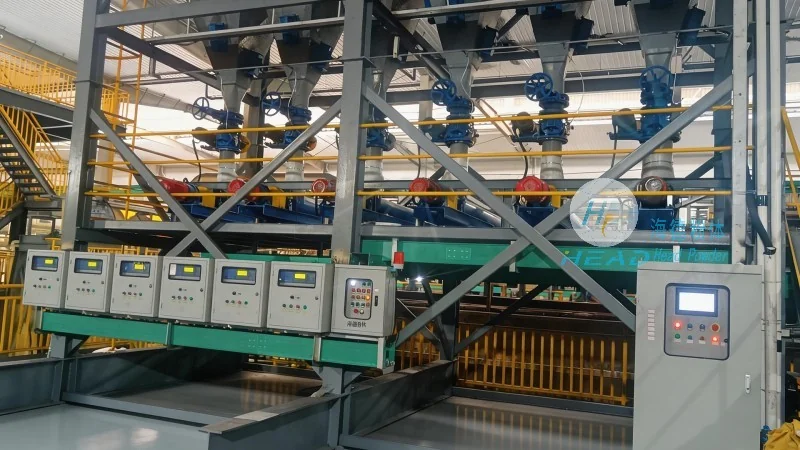
Several key components make up a salt pneumatic conveyor system. The primary components include the air compressor, which provides the necessary pressure to move the material; the feed hopper, which holds the salt and feeds it into the system; the pipeline network, which transports the salt from the source to the destination; and the discharge device, which releases the salt at the end of the pipeline. Each component plays a vital role in the overall operation. For example, the air compressor must be powerful enough to overcome the resistance in the pipeline and lift the salt particles. The feed hopper must be designed to prevent material bridging and ensure a steady flow of salt into the system. The pipeline must be properly sized and supported to maintain the air flow and prevent sagging or kinking, which could cause blockages. The discharge device must be efficient in releasing the salt without causing excessive pressure buildup or spillage.
There are several advantages to using a salt pneumatic conveyor for material handling. One of the main benefits is the ability to transport salt in a closed system, which helps maintain hygiene and prevents contamination from external sources. This is particularly important for food-grade salt, where purity is essential. Another advantage is the flexibility in layout, as the system can be installed in various configurations, including vertical, horizontal, or a combination of both, to suit the specific needs of the facility. Additionally, the system is relatively compact compared to traditional mechanical conveyors, saving space in the plant. It also reduces maintenance costs, as there are fewer moving parts that can wear out or require frequent replacement.
Salt pneumatic conveyors are widely used in various applications within the salt industry. They are commonly used in salt mines to transport mined salt from the extraction site to processing facilities. In salt processing plants, they are used to move salt through different stages of processing, such as washing, drying, and packaging. The system is also used in salt storage facilities to transfer salt from storage silos to packaging lines. In addition, salt pneumatic conveyors are used in food processing plants to transport salt for use in various food products, ensuring that the salt is handled in a clean and hygienic manner.
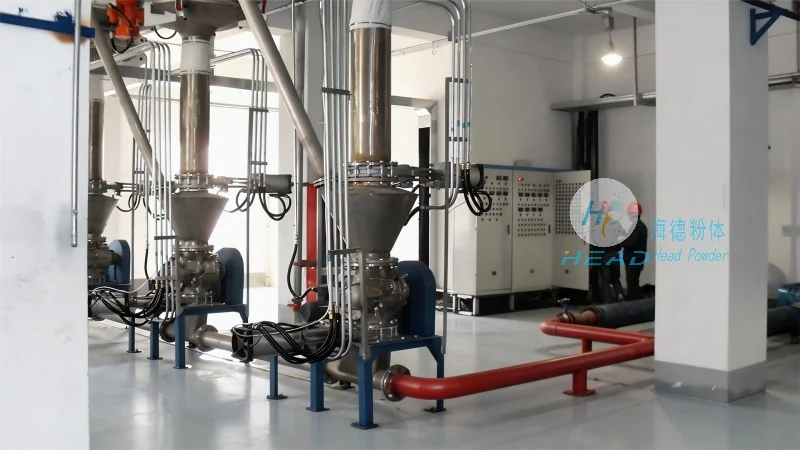
In conclusion, a salt pneumatic conveyor is an efficient and reliable system for transporting salt and other granular materials. Its design is based on principles that ensure optimal performance, including consistent air flow, proper pipeline design, and durable components. The system offers several advantages, including hygiene, flexibility, and reduced maintenance costs. For industries dealing with salt, this equipment is an essential part of the material handling process, ensuring that the salt is transported safely and efficiently from the source to the destination.
Companies like Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specialize in designing and manufacturing such pneumatic conveyor systems. They leverage advanced engineering principles to create customized solutions that meet the specific needs of their clients, ensuring that the salt is transported efficiently and safely.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top