Intelligent material handling equipment, as represented by products from Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated integration of automation, sensor technology, and advanced control systems. These systems are designed to optimize the movement, storage, and management of materials within industrial and logistics environments. The core objective is to enhance operational efficiency, reduce human error, and improve overall productivity by automating traditional material handling tasks. This equipment is particularly valuable in sectors such as manufacturing, warehousing, and distribution, where the flow of goods is critical to business success.
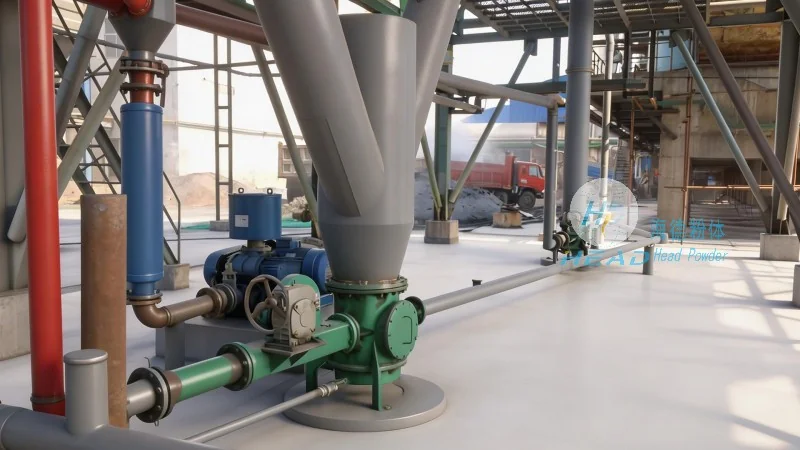
The operation of intelligent material handling systems relies on several key components that work in concert to achieve seamless material movement. At the heart of these systems are automated guided vehicles (AGVs) or automated storage and retrieval systems (AS/RS), which are equipped with advanced navigation and control modules. Sensors, including laser scanners, ultrasonic detectors, and vision systems, provide real-time environmental data, enabling the equipment to adapt to changing conditions and avoid obstacles. Additionally, sophisticated control software and communication networks facilitate coordination between different units, ensuring synchronized operations across the entire system. The integration of these components allows for precise, reliable, and efficient material handling, even in complex and dynamic environments.
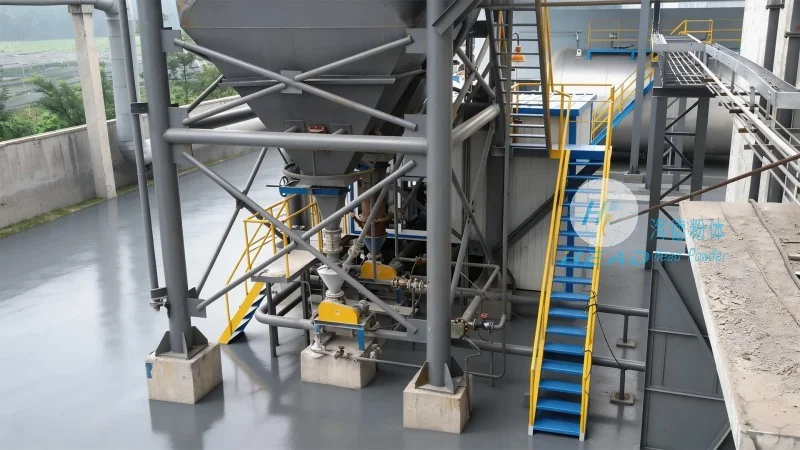
The operational process of intelligent material handling equipment begins with the receipt of a material transfer request, typically initiated by a warehouse management system (WMS) or a similar control interface. The system then processes the request, determining the optimal path and resources required for the task. This involves selecting the appropriate AGV or AS/RS unit, assigning it to the task, and providing real-time guidance through the navigation system. As the equipment moves, sensors continuously monitor its surroundings, adjusting its trajectory as needed to avoid collisions or other obstacles. Upon reaching the designated location, the equipment executes the required action, such as picking up a pallet from a storage rack or delivering it to a specific workstation. The entire process is monitored and controlled by the central system, which tracks the status of each task, provides feedback on performance, and adjusts operations as necessary to maintain efficiency. This end-to-end process ensures that material handling tasks are completed accurately and in a timely manner, minimizing downtime and maximizing productivity.
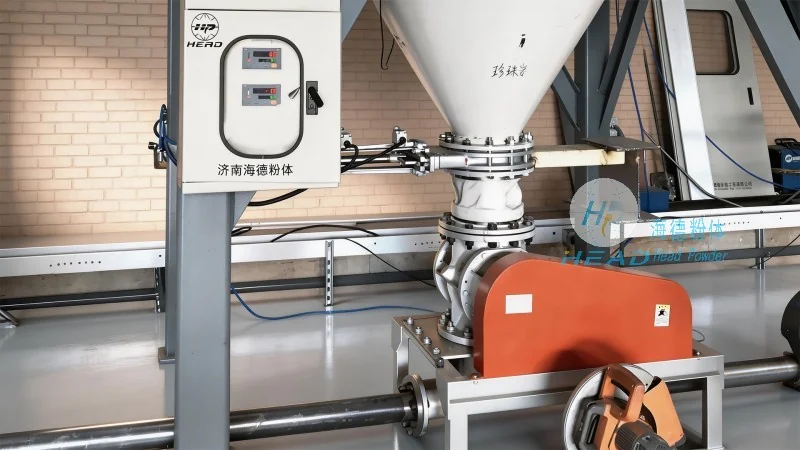
The working principle of intelligent material handling equipment is based on a combination of hardware and software technologies that enable autonomous and intelligent operation. The system starts with the input of a task, which is processed by the control software to generate a set of instructions for the equipment. These instructions are then transmitted to the vehicle or system unit, which uses its navigation sensors to locate itself within the environment and plan the most efficient route. The AGV or AS/RS unit then moves along the planned path, using its sensors to detect and react to any changes in the environment. At key points, such as intersections or loading/unloading zones, the system may pause and perform additional checks to ensure safety and accuracy. Once the task is completed, the system updates its status and may proceed to the next task or return to a standby position. The entire process is governed by a centralized control system that manages all operations, coordinates between different units, and provides real-time monitoring and reporting. This integrated approach ensures that the equipment operates reliably, efficiently, and safely, meeting the demands of modern industrial and logistics operations.
Intelligent material handling equipment offers numerous benefits that enhance operational performance and contribute to business success. By automating material movement, these systems reduce the need for manual labor, minimizing the risk of human error and improving safety in the workplace. The use of advanced sensors and control systems ensures precise and consistent performance, leading to higher throughput and reduced downtime. Additionally, the ability to integrate with existing warehouse management systems allows for seamless coordination with other operational processes, improving overall supply chain efficiency. These benefits make intelligent material handling equipment particularly suitable for applications in manufacturing, where just-in-time production requires efficient material flow, and in warehousing, where high-volume storage and retrieval are essential. The systems can be customized to meet the specific needs of different industries and operational environments, providing a flexible solution for material handling challenges.
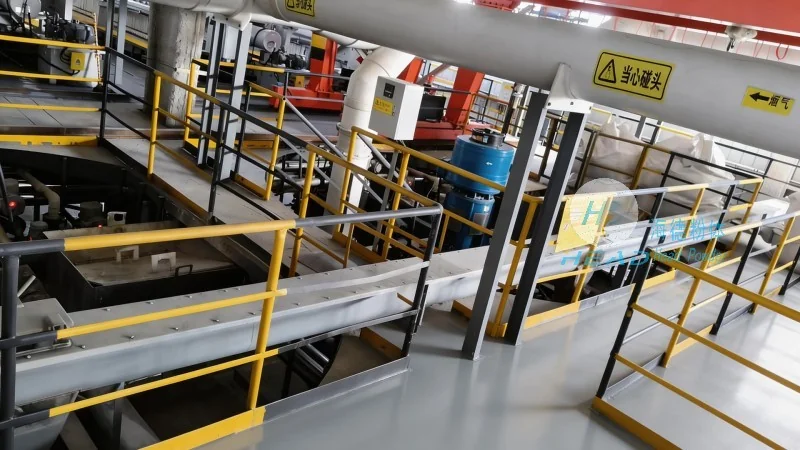
Intelligent material handling equipment, as exemplified by the products of Shandong HeadPowder Engineering Co., Ltd., represents a significant advancement in industrial automation. Through the integration of advanced technologies and intelligent control systems, these devices enable efficient, reliable, and safe material handling operations. The operational process, from task initiation to completion, is guided by sophisticated software and hardware components that work together to optimize performance. The working principle, based on real-time sensing and autonomous decision-making, ensures that the equipment can adapt to changing conditions and maintain high levels of productivity. As industries continue to evolve and demand greater efficiency, intelligent material handling systems will play an increasingly important role in meeting these challenges. With their ability to enhance operational performance and reduce costs, these systems offer a valuable solution for businesses seeking to improve their material handling capabilities and stay competitive in the modern market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top