Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of mineral processing equipment, specializes in the design, development, and production of advanced conveying systems for mineral granular materials. The company, commonly known as HeadPowder, is headquartered in Shandong, China, and has established a strong reputation for delivering high-quality, reliable, and efficient equipment tailored to the needs of various industrial applications.
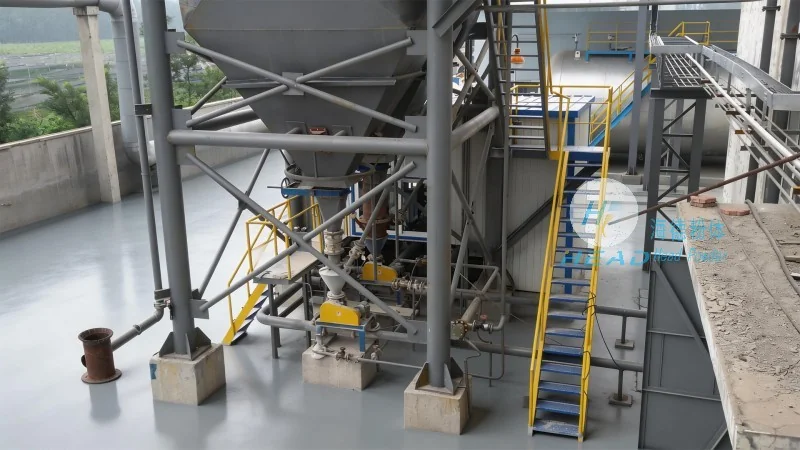
The mineral granular material conveying system is a sophisticated piece of machinery engineered to transport bulk mineral materials such as ores, powders, and granules over long distances with minimal energy consumption and maximum operational efficiency. This system integrates multiple components, including feeders, conveyors, control systems, and safety mechanisms, to ensure seamless material handling from the source to the destination.
The operation of the mineral granular material conveying system follows a systematic sequence of steps to ensure optimal performance and safety. Initially, the raw mineral material is fed into the system through a hopper or feeder, where it is evenly distributed and prepared for transport. The material then enters the conveyor section, which may consist of belt conveyors, screw conveyors, or pneumatic systems, depending on the specific requirements of the application. As the material moves through the conveyor, it is continuously monitored by sensors and control devices to maintain consistent flow rates and prevent blockages. The system also includes automatic shut-off and emergency stop functions to ensure operator safety and equipment protection. Finally, the material is discharged at the receiving end, completing the conveying process.
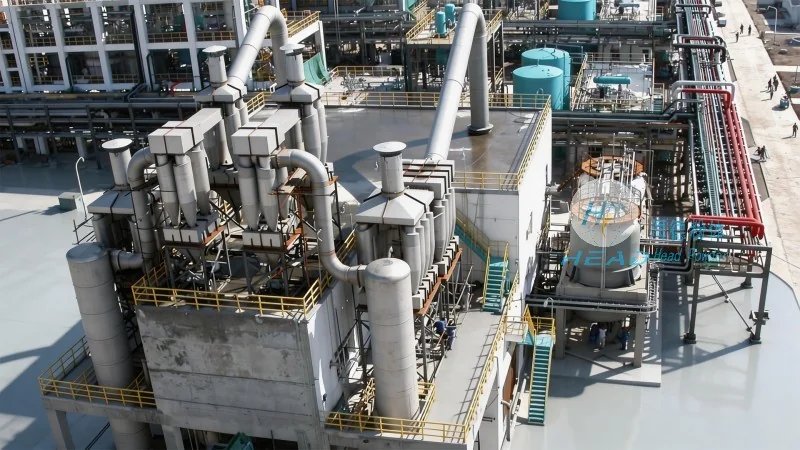
The working principle of the mineral granular material conveying system is based on mechanical or pneumatic forces to move the material from the feed point to the discharge point. For mechanical systems, such as belt conveyors, the material is carried by a moving belt that is driven by a motor and pulley system. The belt's speed and tension are carefully controlled to maintain a stable material flow, preventing spillage or degradation of the material. Screw conveyors, on the other hand, use a rotating screw to push the material forward, which is particularly effective for handling dry, free-flowing materials. Pneumatic conveying systems utilize compressed air to transport the material through a pipeline, where the air velocity and pressure are optimized to ensure efficient and dust-free transport. The control system of the conveyor monitors various parameters, including flow rate, pressure, and temperature, to adjust the operation in real-time and maintain optimal performance.
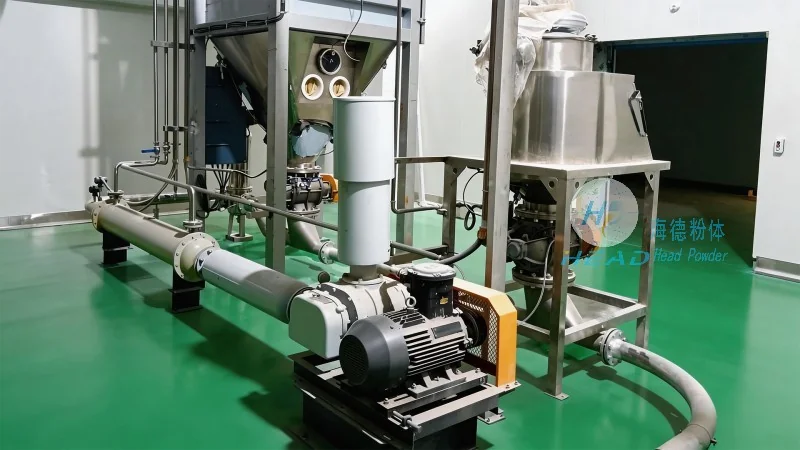
The mineral granular material conveying system comprises several critical components, each playing a vital role in the overall operation. The feeder is responsible for feeding the material into the system at a controlled rate, ensuring uniform flow and preventing overloading. The conveyor itself, whether belt, screw, or pneumatic, is the primary component for material transport. The drive system, including motors and gearboxes, provides the necessary power to move the conveyor. The control panel, equipped with sensors and monitoring devices, allows operators to adjust settings and monitor the system's performance. Safety features, such as emergency stop buttons and overload protection, are integrated to protect both the equipment and personnel. Maintenance components, including bearings and seals, are designed to minimize downtime and extend the system's lifespan.
The mineral granular material conveying system offers several advantages, including high efficiency, low energy consumption, and versatility in handling various types of mineral materials. It is widely used in industries such as mining, cement, chemical, and food processing, where the transport of bulk materials is essential. The system's ability to handle large volumes of material at a consistent rate makes it ideal for applications requiring continuous operation, such as ore processing plants and cement production facilities. Additionally, the system's modular design allows for easy integration with existing production lines and customization to meet specific operational requirements.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top