Distillers' grains powder, a byproduct of the distillation process in the alcohol industry, requires efficient and reliable handling methods for transportation and distribution. Pneumatic conveying technology offers a solution that ensures the safe and effective movement of these powders, and understanding its operation process and working principle is crucial for optimizing industrial applications.
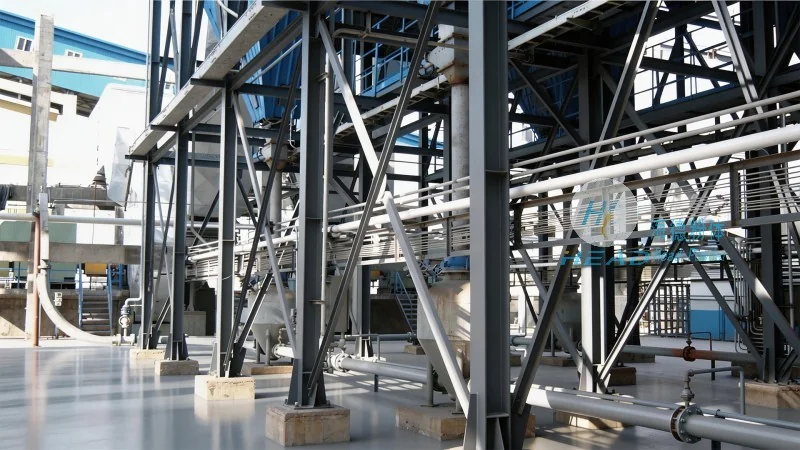
Pneumatic conveying systems are widely used in the food and chemical industries to transport bulk materials like distillers' grains powder. These systems utilize air or gas as the conveying medium to move powders through a pipeline network. The technology is particularly suitable for materials that are dusty, have a high moisture content, or are prone to caking, making it an ideal choice for handling distillers' grains powder, which is often used as animal feed or in other industrial applications.
The pneumatic conveying system for distillers' grains powder typically consists of several key components that work in tandem to ensure efficient operation. These include the material feed hopper, which holds the powder and regulates the flow into the system; the air compressor or blower, which generates the necessary air pressure to move the material; the conveying line, which is a network of pipes that transports the powder and air mixture; and the discharge device, which delivers the material to its final destination. Additionally, the system may include filters and dust collectors to maintain air quality and prevent material buildup in the system.
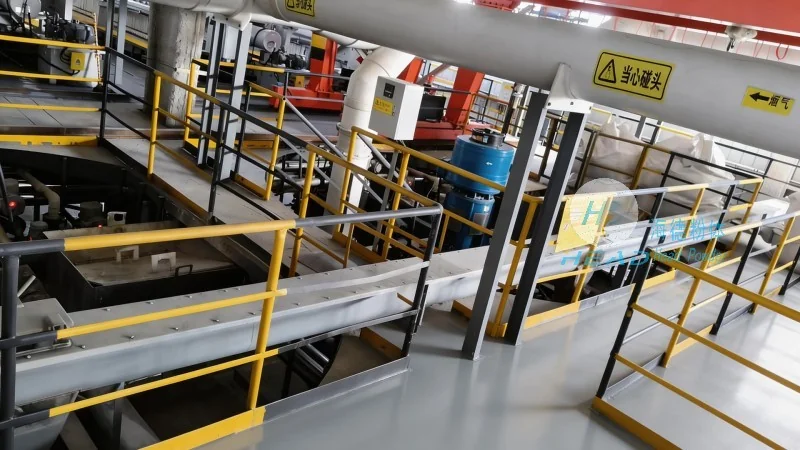
The operation of a pneumatic conveying system for distillers' grains powder involves several stages. First, the powder is fed from the hopper into the conveying line. The air compressor then generates a high-pressure air stream that is introduced into the line, creating a flow that carries the powder particles along with it. As the air and powder mixture moves through the pipeline, the velocity and pressure are carefully controlled to ensure that the powder is transported without clogging or degradation. The system may use different conveying modes, such as dilute phase or dense phase, depending on the material characteristics and the required distance of transport. Dilute phase conveying uses lower air velocities and is suitable for shorter distances, while dense phase conveying uses higher air velocities and is ideal for longer distances or when handling more abrasive materials.
The operation process of a pneumatic conveying system for distillers' grains powder begins with the preparation of the material. The powder is stored in a hopper, which is equipped with a feeder that controls the flow rate. The feeder ensures that the material is fed into the system at a consistent rate, preventing overloading or underloading of the conveying line. Next, the air compressor is activated, and the air is introduced into the conveying line. The air pressure is monitored and adjusted to maintain the desired flow rate and velocity. As the powder is conveyed through the line, it is transported to the discharge point, which may be a storage silo, a processing unit, or a shipping container. The system may also include a return line for the air, which is filtered and recycled to reduce energy consumption and maintain air quality. The entire process is automated, with sensors and controls monitoring the system's performance and adjusting parameters as needed to ensure optimal operation.
Pneumatic conveying offers several advantages when handling distillers' grains powder. One of the primary benefits is the ability to transport the material in a closed system, which prevents dust contamination and maintains product quality. This is particularly important for distillers' grains powder, which is often used in animal feed applications where contamination can affect the health of livestock. Additionally, pneumatic conveying systems are flexible and can be easily integrated into existing industrial processes. They can be configured to handle different material types and transport distances, making them a versatile solution for various applications. Another advantage is the reduced risk of material degradation compared to other handling methods, such as bulk handling or manual loading. The closed system and controlled air flow help to maintain the powder's moisture content and prevent caking, which can improve the material's usability and shelf life.
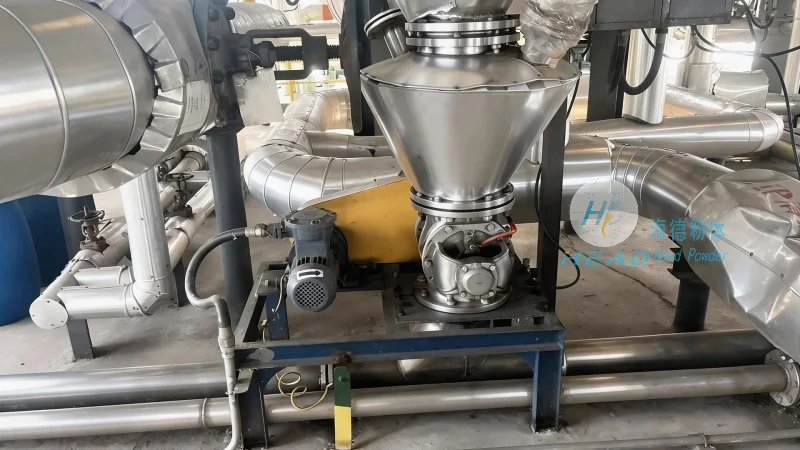
The use of pneumatic conveying systems for distillers' grains powder is widespread in the industry. These systems are commonly used in distilleries to transport the powder from the production line to storage silos or to other processing facilities. They are also used in feed mills and animal feed manufacturers to move the powder from storage to production lines for mixing with other ingredients. The systems are particularly useful in large-scale operations where the volume of material to be transported is high, and the need for efficient and reliable handling is critical. Additionally, pneumatic conveying systems can be used in the transportation of distillers' grains powder to other locations, such as feed mills or animal feed producers, ensuring that the material is delivered in a clean and hygienic manner.
Pneumatic conveying is an essential technology for the efficient and reliable handling of distillers' grains powder. Understanding the operation process and working principle of these systems is crucial for optimizing their performance and ensuring the quality of the material being transported. The systems offered by Shandong HeadPowder Engineering Co., Ltd. are designed to meet the specific needs of the distillers' grains industry, providing reliable and efficient solutions for material handling. With their expertise in pneumatic conveying technology, HeadPowder provides high-quality systems that are tailored to the unique requirements of each client, ensuring optimal performance and long-term reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top