Pneumatic conveying systems for powdered grains and flour are sophisticated industrial solutions designed to transport bulk materials efficiently and safely. The process involves several key stages that work in tandem to ensure smooth material movement from the source to the destination. At the core of this system is the air flow mechanism, which creates the necessary pressure and velocity to move the material particles through a pipeline network.
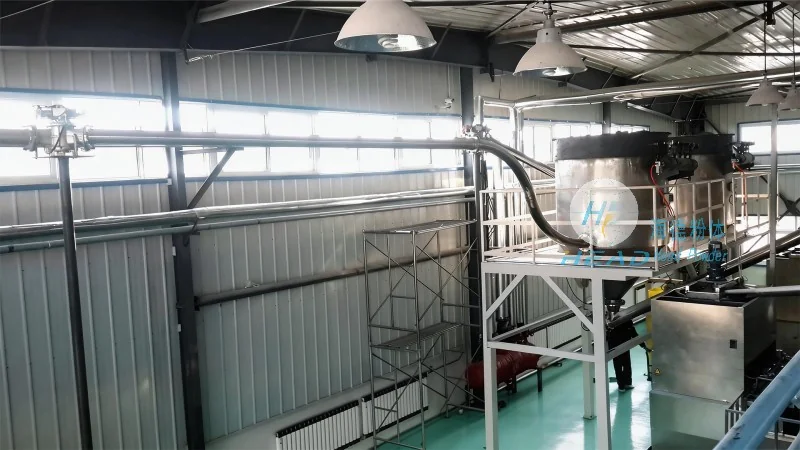
The working principle of pneumatic conveying for powdered grains and flour is based on the fundamental concept of using air as a medium to transport solid particles. This method is particularly effective for materials that are prone to dust, caking, or segregation. The system typically consists of a blower or compressor that generates the air pressure, a hopper or feeder to introduce the material, and a pipeline system that directs the material flow. The air flow is controlled to maintain the appropriate velocity and pressure, ensuring that the material particles are suspended and transported without excessive wear or degradation.
Several critical components are integral to the efficient operation of a pneumatic conveying system for powdered grains and flour. These include the air compressor or blower, which provides the necessary air pressure; the material feeder, which controls the flow rate of the powder; the conveying pipeline, which transports the material; and the dust collector or filter, which removes any airborne particles to maintain air quality and prevent contamination. Each component plays a vital role in ensuring the system operates reliably and meets the required standards for material handling.
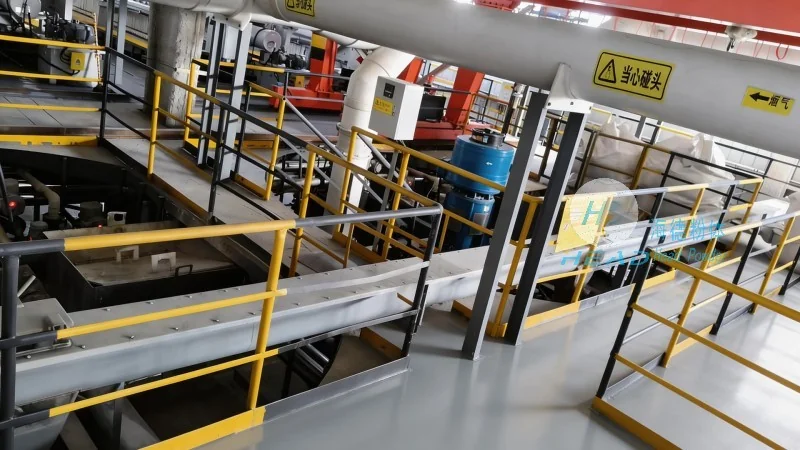
The operation of a pneumatic conveying system for powdered grains and flour involves a sequence of steps that are carefully managed to achieve optimal performance. The process begins with the material being loaded into a hopper or storage silo. From there, the material is fed into the system via a feeder, which regulates the flow rate to match the air flow. The air compressor then generates the required pressure, and the air is introduced into the pipeline, creating a flow that carries the material particles. As the material travels through the pipeline, it is suspended by the air flow and transported to the destination point, such as a silo, storage tank, or processing unit. The system may include multiple stages, such as transfer points or branch lines, to direct the material to different locations within the facility. At the end of the pipeline, the material is separated from the air, often through a cyclone or filter, and collected in a receiving hopper.
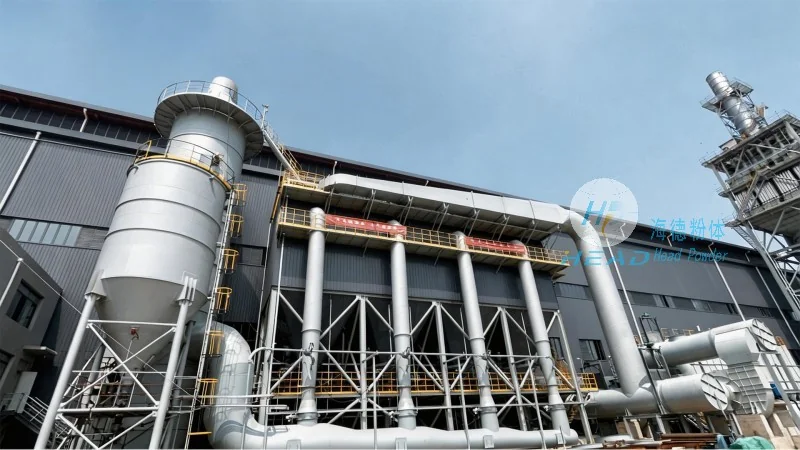
Pneumatic conveying offers several advantages over traditional methods like belt conveyors or bucket elevators for handling powdered grains and flour. One of the primary benefits is the ability to transport materials in a closed system, which minimizes dust exposure and prevents contamination from external sources. This is particularly important for food-grade products like flour, where hygiene and quality control are paramount. Additionally, pneumatic conveying systems can handle materials with varying particle sizes and moisture content, making them versatile for different applications. The system also allows for easy integration with other processing equipment, such as mixers or classifiers, and can be scaled to accommodate different production volumes. Furthermore, the enclosed nature of the system reduces the risk of material loss and improves overall efficiency by minimizing downtime and maintenance.
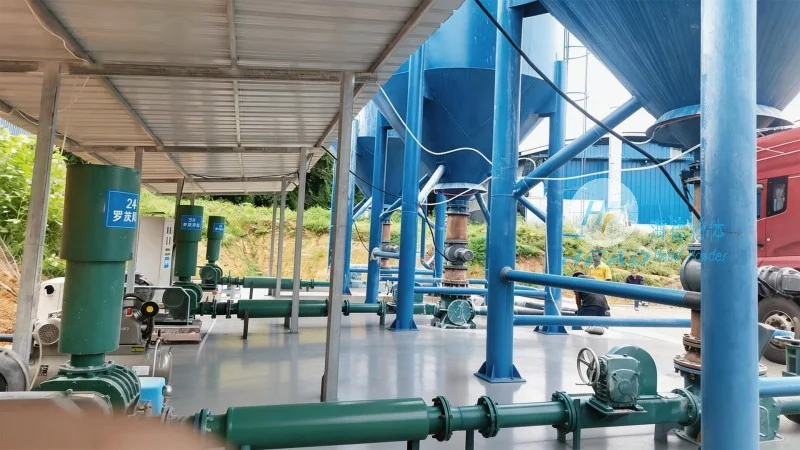
The use of pneumatic conveying systems for powdered grains and flour is widespread across various industries. In the food processing sector, these systems are commonly used in flour mills, bakeries, and snack food production facilities to transport raw materials and finished products. The agricultural industry also relies on pneumatic conveying for handling grain from storage silos to processing plants or for transporting grain to ports for export. In the chemical and pharmaceutical industries, similar systems are used to transport powders that require strict control over particle size and purity. The versatility of pneumatic conveying makes it suitable for a wide range of applications where efficient and clean material handling is essential.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of pneumatic conveying systems and related equipment for powdered grain and flour handling. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the industry. HeadPowder specializes in designing and manufacturing customized pneumatic conveying solutions that meet the specific needs of its clients. The company's products are known for their reliability, efficiency, and compliance with industry standards. HeadPowder's team of engineers and technicians work closely with clients to understand their requirements and develop tailored solutions that enhance productivity and reduce operational costs. The company is committed to providing comprehensive support, including installation, maintenance, and technical assistance, to ensure that its systems operate at peak performance. With its headquarters in Shandong, China, HeadPowder serves clients both domestically and internationally, delivering high-quality pneumatic conveying systems that meet the demands of modern industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top