Sulfate potash, a vital component in modern agriculture, demands efficient and reliable material handling to support its production and distribution. Pneumatic conveying systems have emerged as a preferred solution for transporting this material due to their ability to handle bulk quantities with minimal human intervention. The fundamental working principle of a pneumatic conveying system involves the use of compressed air to create a flow that moves the sulfate potash particles through a pipeline. This process typically begins with the material being fed into a hopper or feeder, where it is then drawn into the air stream. The air, often generated by a blower or compressor, creates a pressure differential that propels the material forward. As the material travels through the pipeline, it may encounter various components, such as bends, valves, and filters, which help maintain the flow and prevent blockages. The system concludes with the material being discharged at the destination point, such as a storage silo or processing unit. The entire operation is controlled by a system of sensors and controls that monitor pressure, flow rate, and material level, ensuring optimal performance and safety.
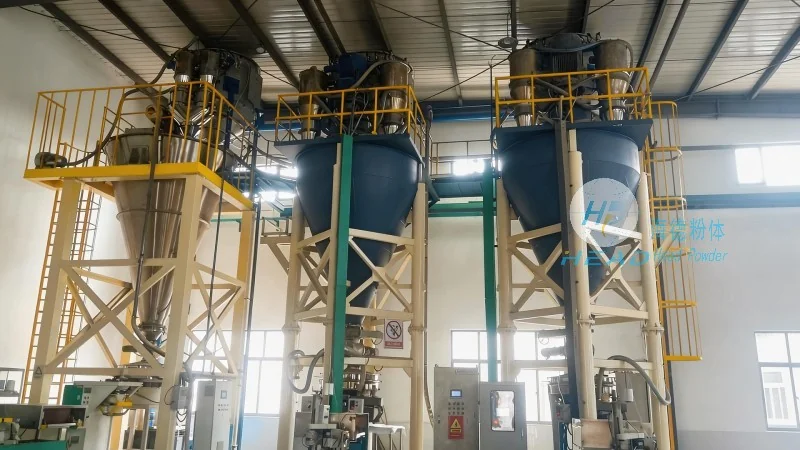
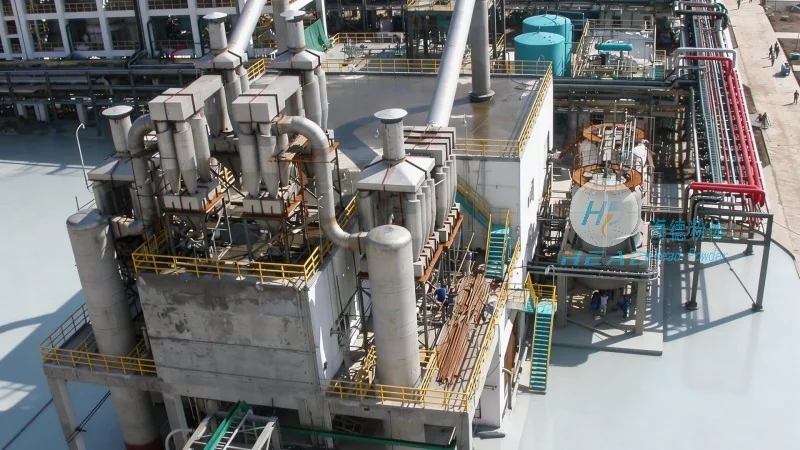
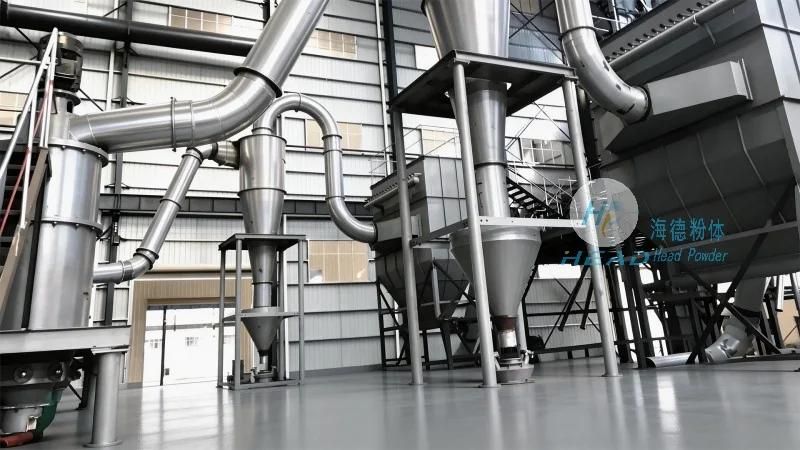
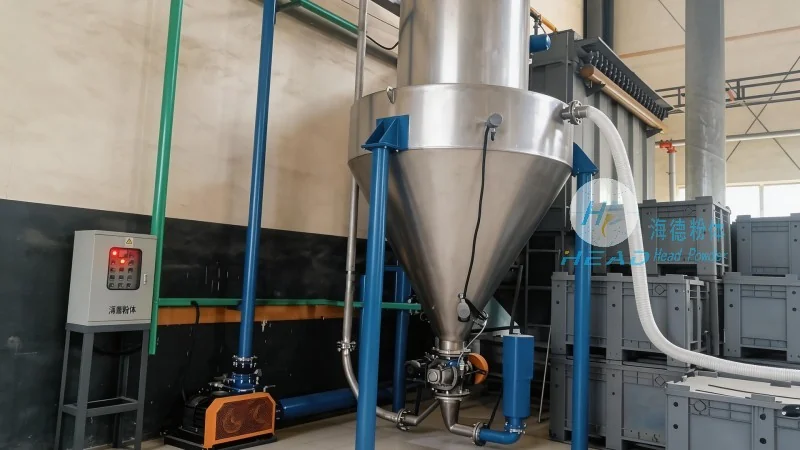
When considering the implementation of pneumatic conveying for sulfate potash, several distinct characteristics and advantages become apparent. Firstly, the systems offer a high degree of flexibility in terms of system layout. Unlike traditional mechanical conveyors, which require fixed routes, pneumatic systems can be reconfigured to accommodate changes in production processes or facility expansions. This adaptability makes them ideal for dynamic industrial environments. Secondly, pneumatic conveying provides superior dust control. The enclosed pipeline design effectively contains the material, reducing dust emissions and minimizing the risk of respiratory issues for personnel. This is particularly important in facilities handling fine or powdery materials like sulfate potash. Thirdly, the systems are generally low maintenance. With fewer moving parts compared to belt or bucket elevators, they require less frequent servicing, leading to lower operational costs and reduced downtime. Additionally, pneumatic conveying can be integrated with other equipment, such as silos and blending units, creating a seamless material flow from raw material extraction to final product application. This integration enhances overall process efficiency and reduces the need for manual handling.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as "headpowder", is a leading provider of industrial material handling solutions. The company specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for bulk materials, including sulfate potash. HeadPowder's team of experienced engineers and technicians leverages cutting-edge technology and rigorous quality control processes to deliver customized solutions that meet the specific needs of each client. The company's operations are based in Shandong, China, where it benefits from a strong industrial infrastructure and access to skilled labor. HeadPowder's commitment to innovation and customer satisfaction has established it as a trusted partner in the fertilizer and related industries. By focusing on efficiency, reliability, and sustainability, the company aims to enhance the productivity and environmental performance of its clients' operations. With a reputation for delivering high-quality products and exceptional service, HeadPowder continues to expand its market presence and support the growth of its clients' businesses.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top