HeadPowder, a leading provider in the field of material handling solutions, specializes in the design and implementation of advanced pneumatic conveying systems. This article delves into the fundamental principles underlying the operation of a magnesium hydroxide pneumatic conveying system, highlighting the technical aspects and practical applications that define this critical equipment for industrial processes.
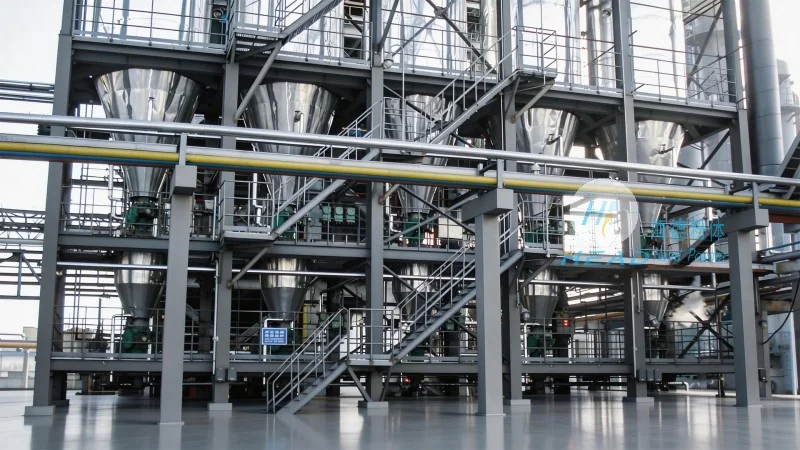
HeadPowder, operating under the full name Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for businesses seeking efficient and reliable material transport solutions. Our expertise in pneumatic conveying technology ensures that clients receive tailored systems that meet their specific operational requirements.
Pneumatic conveying systems utilize air or other gases to transport bulk materials through a pipeline network. This method offers numerous advantages over traditional mechanical conveying, including reduced equipment wear, lower maintenance costs, and the ability to handle a wide range of materials, from fine powders to granular substances. The principle of operation involves creating a pressure differential within the system, which propels the material along the pipeline using the force of the moving air.
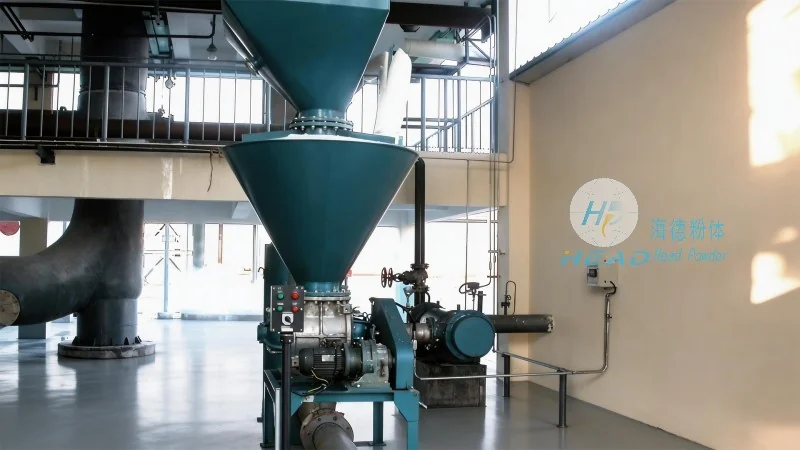
The magnesium hydroxide pneumatic conveying system consists of several core components that work in tandem to ensure efficient material transport. These include the material feed hopper, which stores and feeds the magnesium hydroxide powder into the system; the air compressor, which generates the necessary air pressure to move the material; the conveying line, which forms the main pathway for the material and air mixture; and the receiver, where the material is deposited after reaching its destination. Each component is carefully designed to handle the unique properties of magnesium hydroxide, such as its fine particle size and potential for caking, ensuring optimal performance.
The operation of the magnesium hydroxide pneumatic conveying system follows a systematic process. Initially, the magnesium hydroxide powder is introduced into the feed hopper. The air compressor then generates compressed air, which is directed into the conveying line. As the air flows through the line, it entrains the magnesium hydroxide particles, forming a slurry-like mixture. This mixture travels through the pipeline under pressure, reaching the receiver where the material is separated from the air and collected. The air, now free of material, is either recycled back into the system or vented to the atmosphere, depending on the system design. This continuous cycle ensures a steady and reliable flow of magnesium hydroxide from the source to the destination.
Implementing a pneumatic conveying system for magnesium hydroxide offers several key benefits. Firstly, it eliminates the need for manual handling, reducing labor costs and improving workplace safety. The system also minimizes material degradation, as the enclosed pipeline prevents exposure to moisture or contaminants. Additionally, the ability to transport materials over long distances without the need for intermediate storage points enhances operational efficiency. Furthermore, the system's flexibility allows for easy integration with existing production lines, making it a cost-effective solution for businesses looking to upgrade their material handling capabilities.
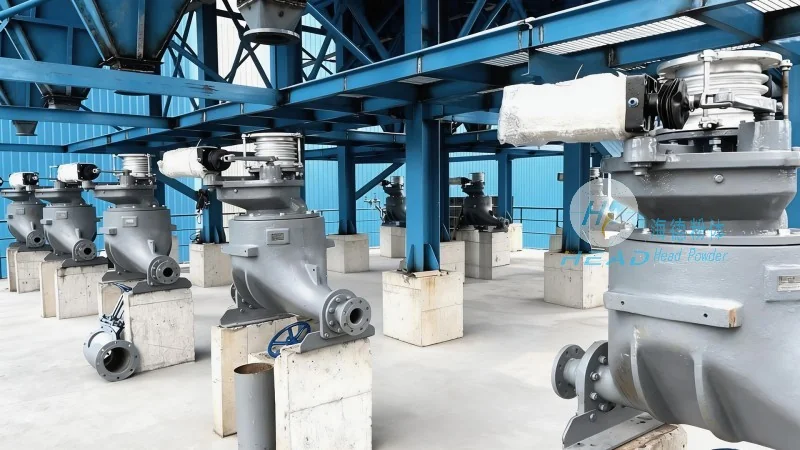
Magnesium hydroxide pneumatic conveying systems are widely used in various industrial applications, particularly in the chemical and pharmaceutical industries. These systems are employed to transport magnesium hydroxide from storage silos to processing units, ensuring a consistent supply of raw material for manufacturing processes. The system's ability to handle fine powders without clogging or blockages makes it ideal for applications where material purity and consistency are critical. In addition, the system's scalability allows it to be adapted for both small-scale laboratory operations and large-scale industrial production, catering to the diverse needs of different industries.
To ensure the longevity and efficiency of a magnesium hydroxide pneumatic conveying system, regular maintenance is essential. This includes monitoring air pressure levels, checking for any signs of material buildup or blockages in the pipeline, and performing routine cleaning of the system components. Proper maintenance not only extends the lifespan of the equipment but also ensures consistent performance and reduces the risk of operational disruptions. Additionally, training operators on the proper use and handling of the system is crucial to prevent accidents and maintain safety standards. By adhering to these operational guidelines, businesses can maximize the benefits of their pneumatic conveying system while minimizing downtime and maintenance costs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top