For industries that rely on precise and efficient handling of capsule-based materials, understanding the underlying principles and operational characteristics of capsule material conveying systems is crucial. These systems are designed to transport capsules—whether they are empty or filled—through various stages of production, ensuring consistent quality and minimizing downtime. The core of such systems lies in their mechanical design, which integrates components like rollers, belts, and control mechanisms to achieve smooth, controlled movement of the capsules.
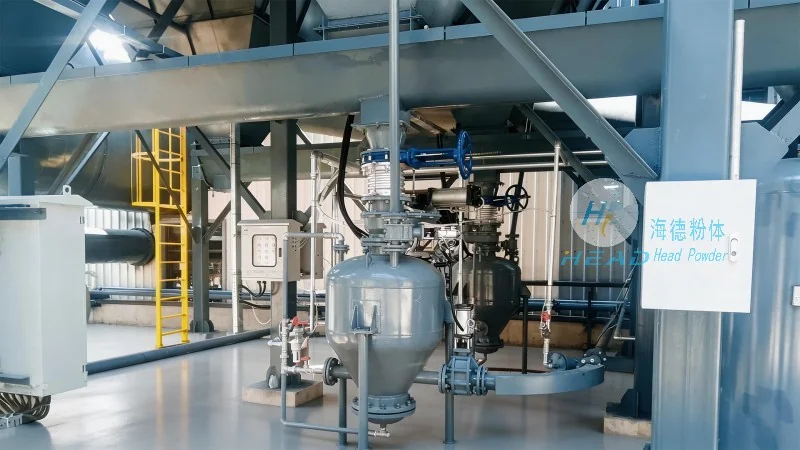
The fundamental principle of capsule material conveying is to maintain the integrity of the capsules while moving them efficiently. This involves several key aspects: first, the system must handle the delicate nature of capsules without causing damage, which is achieved through gentle contact surfaces and adjustable speeds. Second, the conveying path is engineered to minimize friction and vibration, as excessive force can lead to capsule deformation or breakage. Third, the system incorporates sensors and control units to monitor the flow rate and position of capsules, allowing for real-time adjustments to maintain optimal performance. These principles are critical for industries such as pharmaceuticals, where product quality and safety are paramount.
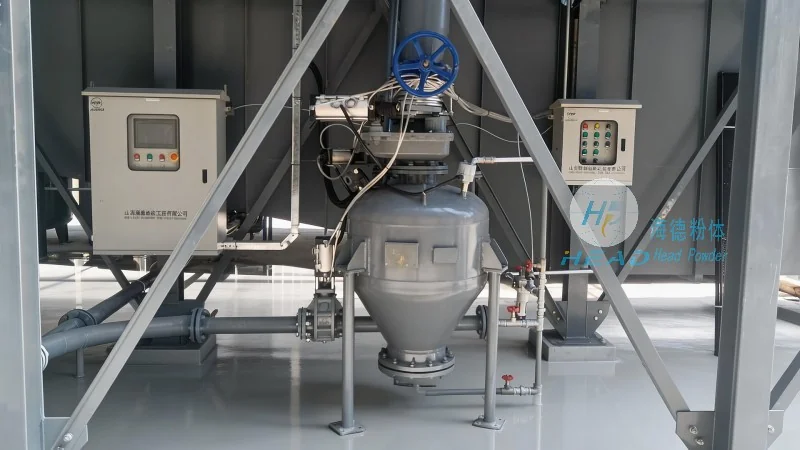
At the heart of a capsule material conveying system are several components that work in tandem to ensure reliable operation. The primary components include feeders, conveyors, and sorting mechanisms. Feeders are responsible for uniformly distributing capsules into the conveying path, often using gravity or mechanical agitation to prevent jams. Conveyors, typically made of flexible belts or rollers, move the capsules along the designated route. These conveyors are designed with smooth, non-stick surfaces to avoid sticking or scratching the capsules. Sorting mechanisms, such as vibratory screens or air jets, are used to separate defective capsules from the good ones, ensuring only high-quality materials proceed to the next stage. The integration of these components is what makes the system both efficient and effective.
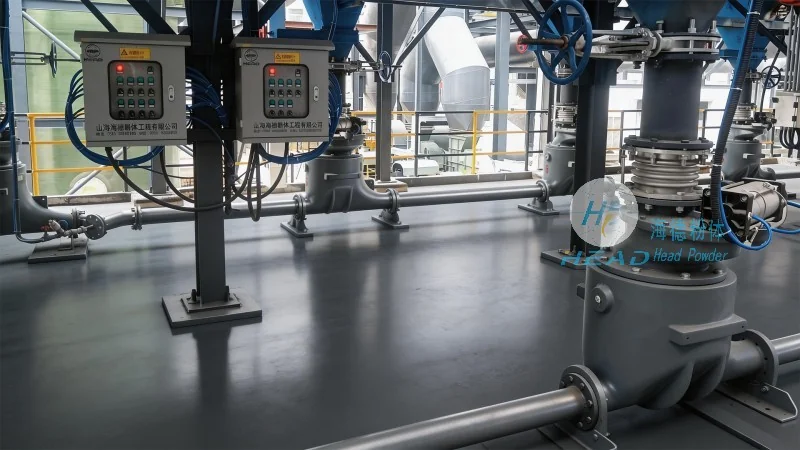
The operational characteristics of capsule material conveying systems vary significantly based on the industry they serve. In the pharmaceutical industry, for example, the system must adhere to strict regulatory standards, such as those set by the FDA. This means the equipment must be easy to clean and sterilize, with no crevices where contaminants can accumulate. The conveying speed is also carefully controlled to prevent capsule damage, as even minor impacts can compromise the integrity of the product. In the food industry, the system must be constructed from food-grade materials, such as stainless steel, to meet hygiene requirements. Additionally, the system may include features like dust collection to maintain a clean environment. For the cosmetics industry, the focus is on maintaining the aesthetic appeal of the capsules, which may involve gentle handling and the ability to handle different capsule sizes and colors. These industry-specific characteristics highlight the adaptability of capsule material conveying systems to diverse operational needs.
Companies that invest in professional capsule material conveying solutions, such as those offered by Shandong HeadPowder Engineering Co., Ltd., benefit from several advantages. These systems are designed to enhance productivity by reducing manual handling and minimizing the risk of human error. They also improve product quality by ensuring consistent movement and gentle handling of capsules. Furthermore, the use of advanced control systems allows for real-time monitoring and data collection, which can be used to optimize processes and identify areas for improvement. The durability of these systems, with proper maintenance, ensures long-term reliability, reducing the need for frequent replacements or repairs. For businesses looking to streamline their operations and maintain high standards of quality, investing in a well-designed capsule material conveying system is a strategic decision.
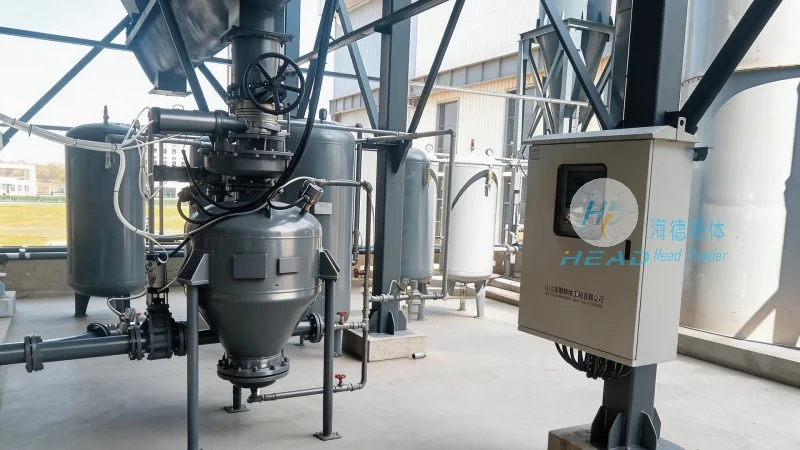
In conclusion, capsule material conveying systems are essential tools for industries that handle capsules, offering a combination of efficiency, precision, and reliability. By understanding the core principles and operational characteristics of these systems, businesses can select the right equipment to meet their specific needs. Whether in pharmaceutical, food, or cosmetics manufacturing, the ability to transport capsules safely and effectively is critical to success. Companies like Shandong HeadPowder Engineering Co., Ltd., with their expertise in designing and manufacturing such systems, provide tailored solutions that address the unique challenges of each industry. By leveraging these solutions, businesses can enhance their operational efficiency, improve product quality, and stay competitive in their respective markets.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top