Efficient material handling is a critical component in various industrial processes, ensuring smooth workflow and optimal resource utilization. Among the diverse materials requiring transport, wood ash presents unique challenges due to its characteristics such as light weight, fine particle size, and potential moisture content. The operation process and working principle of wood ash material conveying systems are designed to address these challenges while maintaining reliability and efficiency. This article provides an in-depth overview of the key aspects involved in the handling of wood ash, focusing on the technology and methodology employed by Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field.
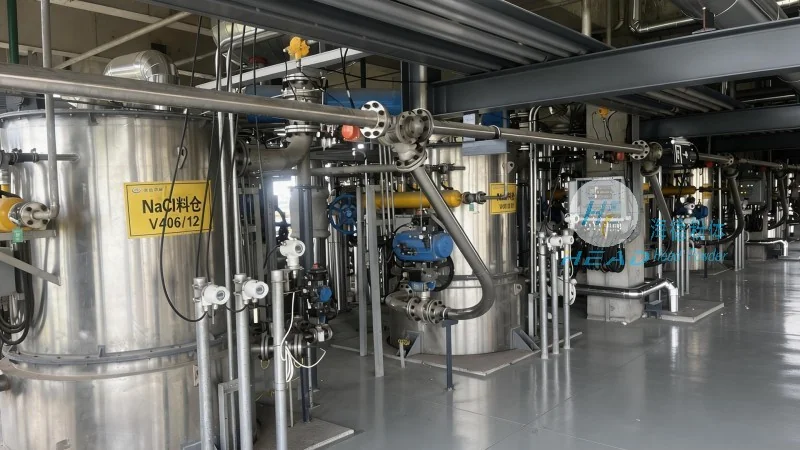
Wood ash, a byproduct of biomass combustion or incineration, is often utilized in agricultural applications, soil amendment, or as a raw material in certain manufacturing processes. The effective conveyance of this material requires specialized equipment capable of managing its physical properties. Conveying systems for wood ash typically involve components like hoppers, feeders, conveyors, and control mechanisms, all integrated to ensure consistent and safe material transport. The design of these systems must consider factors such as the material's flowability, potential dust generation, and the need for minimal degradation or loss during transit.
The core components of a wood ash material conveying system, as implemented by Shandong HeadPowder Engineering Co., Ltd., include several critical elements. The system begins with a hopper or storage bin designed to hold the wood ash, ensuring a steady supply to the feeder. The feeder, often a rotary or vibratory type, regulates the flow of material into the conveyor. For wood ash, which may be lightweight and prone to bridging, a vibratory feeder is commonly employed to prevent blockages and maintain a consistent feed rate. The conveyor itself can vary in type, including screw conveyors, belt conveyors, or pneumatic systems, depending on the specific application and material characteristics. In many cases, a combination of these components is used to achieve the desired conveying efficiency and flexibility.
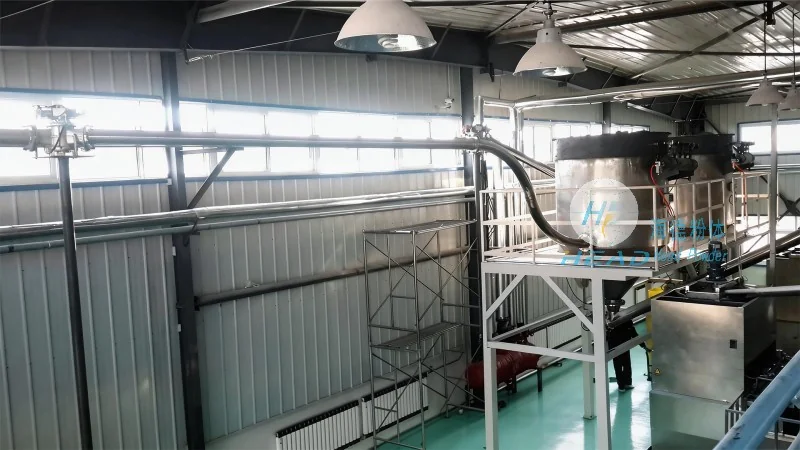
The operation process of a wood ash material conveying system follows a systematic sequence to ensure reliable performance. Initially, the wood ash is stored in the hopper, where it accumulates until the system is activated. The control system then triggers the feeder to begin moving material into the conveyor. As the feeder operates, the material is transferred into the conveyor's path, either through gravity or mechanical force, depending on the conveyor type. For screw conveyors, the rotating screw pushes the material forward, while belt conveyors use a moving belt to transport the material along its length. Pneumatic systems, on the other hand, utilize air pressure to transport the material in a sealed pipe, which is particularly effective for handling fine or dusty materials like wood ash.
The working principle of the wood ash conveying system relies on the interaction of mechanical and control mechanisms to achieve precise material transport. The feeder plays a crucial role in controlling the feed rate, which is adjusted based on the system's demand and the material's flow characteristics. This control helps maintain a steady flow into the conveyor, preventing overloading or underloading that could lead to inefficiencies or equipment damage. The conveyor's operation is synchronized with the feeder, ensuring that material is continuously moved from the hopper to the discharge point. Sensors and monitoring devices are often integrated into the system to detect any deviations, such as blockages or changes in material level, allowing for immediate adjustments to maintain optimal performance.
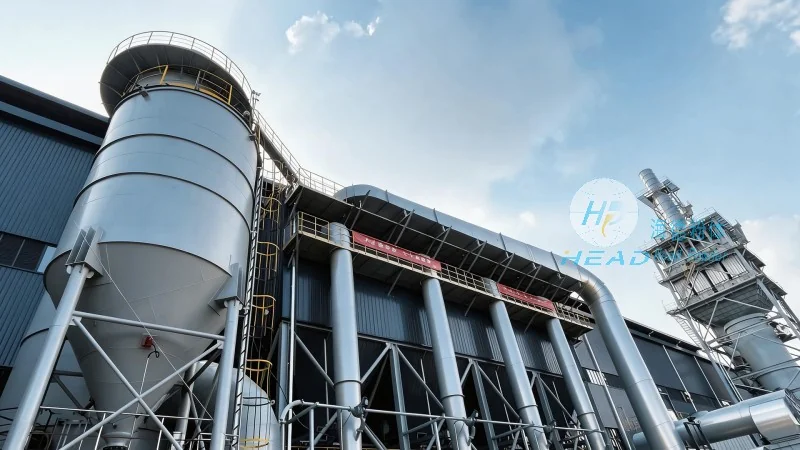
Shandong HeadPowder Engineering Co., Ltd. designs its wood ash conveying systems with a focus on efficiency and durability. The use of robust materials and components ensures that the system can handle the abrasive and potentially corrosive nature of wood ash over extended periods. The integration of advanced control systems allows for real-time monitoring and automation, reducing the need for manual intervention and minimizing operational errors. Additionally, the design minimizes dust generation and material loss, which is critical for maintaining environmental compliance and product quality. The flexibility of the system, allowing for adjustments in conveyor speed or feed rate, enables it to adapt to varying production demands, enhancing overall operational efficiency.
In conclusion, the operation process and working principle of wood ash material conveying systems are integral to the efficient handling of this material. Through a combination of specialized components, precise control mechanisms, and advanced technology, these systems ensure reliable and consistent transport of wood ash. Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted provider in this field, offering solutions tailored to the unique challenges of wood ash handling. By adhering to rigorous design standards and continuous improvement, the company ensures that its conveying systems meet the highest industry standards, providing customers with reliable and efficient material transport solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top