For industrial applications involving rice husk powder, efficient material conveying is crucial for maintaining production efficiency and safety. The operation process and working principle of such systems are designed to handle the unique characteristics of rice husk powder, ensuring reliable and consistent material transport. This article provides an in-depth look at the key aspects of rice husk powder material conveying, focusing on the technical elements and operational procedures.
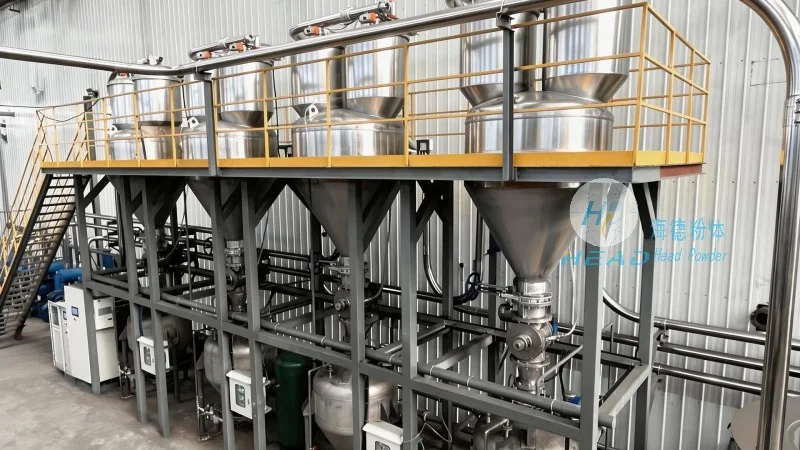
Headpowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and implementation of advanced conveying systems. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for industries requiring efficient material transport. Based in Shandong, China, Headpowder leverages its expertise to deliver tailored solutions that meet the specific needs of clients, including those working with rice husk powder. The company’s headquarters and operational base are located in Shandong, providing a solid foundation for its engineering and service capabilities.
The operation of rice husk powder conveying systems typically involves several critical components that work in tandem to ensure smooth material transport. These components include feeders, conveyors, control systems, and dust collection units. Each component plays a vital role in the overall process, contributing to the system’s efficiency and reliability. The feeders are responsible for accurately metering the rice husk powder into the conveying line, ensuring a consistent flow rate. The conveyors, which may include screw conveyors, pneumatic conveyors, or other types, transport the material from the feed point to the discharge point. Control systems monitor and regulate the operation of the components, while dust collection units manage the airborne particles to maintain a safe and clean working environment.
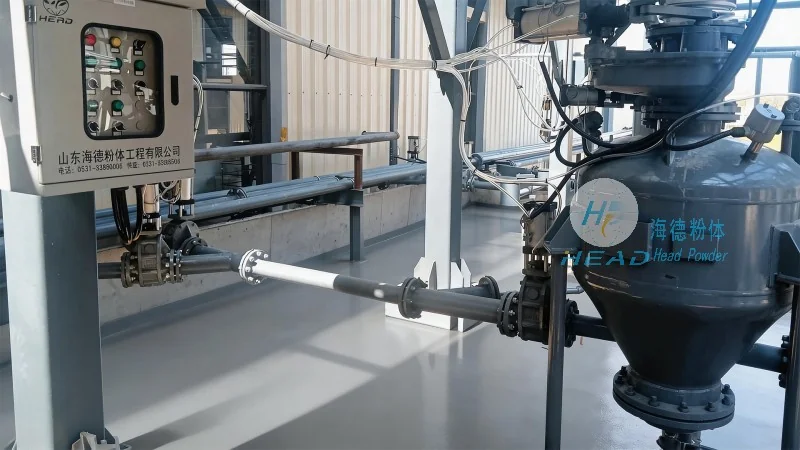
The operation process of rice husk powder material conveying begins with the feeding of the material into the system. The rice husk powder is typically stored in a hopper or silo, from which it is fed into the conveyor system. The feeder ensures that the material is delivered at a controlled rate, preventing overloading or underloading of the conveyor. As the material moves through the conveyor, it is transported to the discharge point, which may be a storage bin, processing unit, or other destination. The control system continuously monitors the flow rate, pressure, and other parameters to ensure that the system operates within optimal conditions. Any deviations are automatically adjusted to maintain consistent performance. The dust collection system works in parallel, capturing any airborne particles to prevent contamination and ensure compliance with environmental regulations.
The working principle of rice husk powder conveying systems is based on the principles of mechanical and pneumatic transport. Mechanical conveyors, such as screw conveyors, use rotating screws to push the material forward, while pneumatic conveyors use air pressure to move the material through a pipeline. The choice of conveyor type depends on factors such as the material characteristics, distance to be covered, and system requirements. For rice husk powder, which is lightweight and can be prone to dust, pneumatic conveyors are often preferred due to their ability to handle fine particles and maintain a clean environment. The system operates by creating a pressure differential between the feed and discharge points, causing the material to move through the pipeline. The control system regulates the air flow and pressure to ensure efficient transport, minimizing energy consumption and maximizing material throughput.
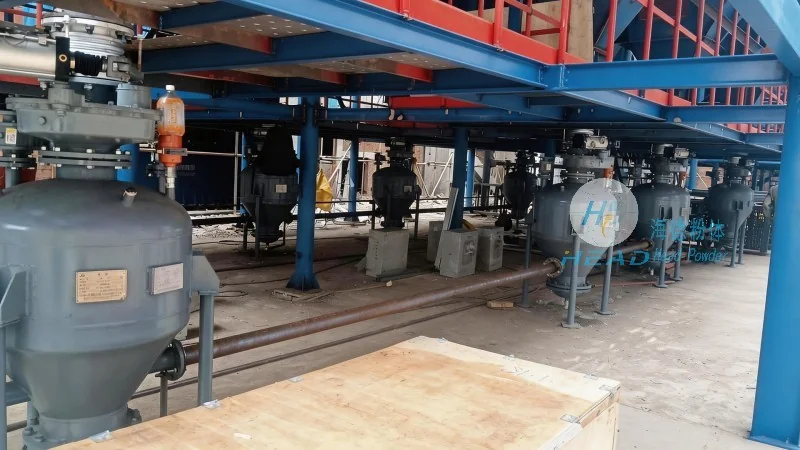
Efficient rice husk powder conveying systems offer several advantages for industrial operations. These include improved production efficiency, reduced labor costs, and enhanced safety. By ensuring consistent material flow, the systems help maintain optimal processing conditions, leading to higher product quality and yield. The use of advanced control systems also reduces the need for manual intervention, minimizing the risk of human error and improving overall operational reliability. Additionally, the integration of dust collection units helps maintain a clean working environment, reducing the risk of respiratory issues and other health hazards associated with handling fine powders. For companies operating in the rice husk processing industry, investing in efficient conveying systems can lead to significant long-term benefits, including increased productivity and improved operational safety.
In conclusion, the operation process and working principle of rice husk powder material conveying systems are critical for the efficient handling of this material. The systems combine mechanical and pneumatic transport methods, supported by advanced control and dust collection technologies, to ensure reliable and safe material transport. Headpowder, with its expertise in material handling solutions, provides tailored conveying systems that meet the specific needs of clients, including those working with rice husk powder. Based in Shandong, China, the company leverages its engineering capabilities to deliver high-quality, reliable systems that enhance operational efficiency and safety. For industries requiring efficient rice husk powder conveying, Headpowder offers a trusted solution that aligns with the latest technological advancements and industry standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top