Coal ash, a byproduct of coal combustion in thermal power plants, requires efficient and reliable handling for disposal or utilization. The process of transporting coal ash from its source to processing or storage facilities involves specialized equipment designed to manage the material's characteristics, such as its fine particle size and potential moisture content. This article explores the operation process and working principle of coal ash material conveying systems, highlighting the key components and mechanisms that ensure effective and safe transport.
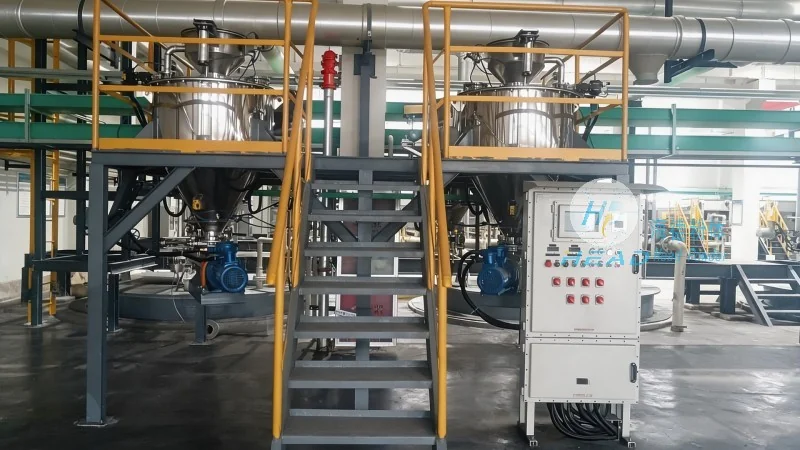
The coal ash conveying system typically consists of several critical components that work in tandem to facilitate material transport. These include feed hoppers, conveyor belts or screw conveyors, control valves, and dust collection systems. The feed hopper is responsible for collecting and storing the coal ash, ensuring a consistent flow into the conveyor. Conveyor belts, often made of durable materials like rubber or PVC, are used to transport the ash horizontally or at slight inclines. Screw conveyors, on the other hand, are suitable for vertical or inclined transport, using a rotating screw to push the material forward. Control valves regulate the flow rate, preventing overloading and ensuring smooth operation. Dust collection systems are essential to maintain air quality and protect personnel from airborne particles.
The operation process of coal ash material conveying begins with the collection of coal ash from the boiler or storage silos. The ash is then fed into the feed hopper, where it is held until the conveyor is ready to receive it. The control system initiates the conveyor, which then moves the ash along the designated path. For horizontal transport, the conveyor belt moves the ash at a steady speed, while for vertical transport, the screw conveyor rotates, pushing the ash upward. The system continuously monitors the flow rate and pressure, adjusting the speed or feed rate as needed to maintain optimal performance. At the end of the conveying path, the coal ash is discharged into a storage tank or processing unit, completing the transport cycle.
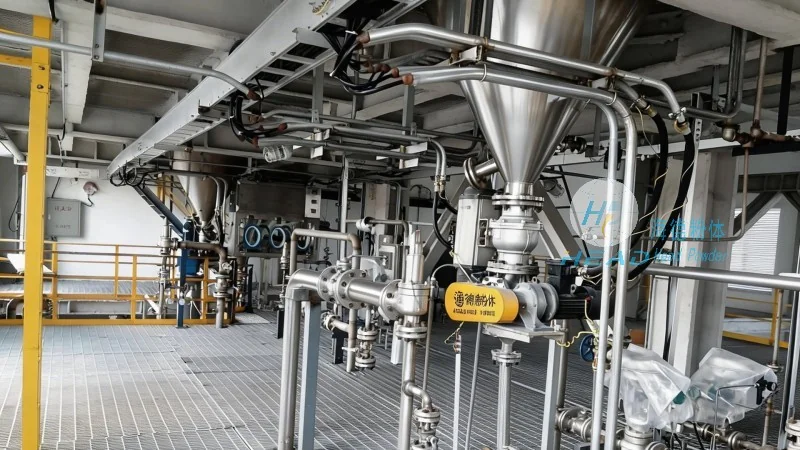
The working principle of coal ash conveying systems is based on mechanical force and gravity, depending on the type of conveyor used. For belt conveyors, the principle is straightforward: the belt moves continuously, and the ash is carried along with it due to friction between the belt and the material particles. The speed of the belt determines the transport rate, and the angle of inclination affects the force required to move the ash. Screw conveyors operate on a different principle: the rotating screw displaces the material along its length, using the helical blades to push the material forward. The pitch and speed of the screw control the transport capacity. In both cases, the system is designed to handle the specific properties of coal ash, such as its low density and fine particle size, ensuring efficient and reliable transport without clogging or damage to the equipment.
Coal ash conveying systems offer several advantages in the handling of coal ash. First, they provide a continuous and automated transport process, reducing the need for manual handling and minimizing the risk of accidents. Second, the systems are designed to handle large volumes of material, making them suitable for industrial-scale applications. Third, the use of enclosed conveyors and dust collection systems helps maintain a clean and safe working environment, protecting both equipment and personnel from dust and debris. Finally, the systems are energy-efficient and low-maintenance, reducing operational costs over time.
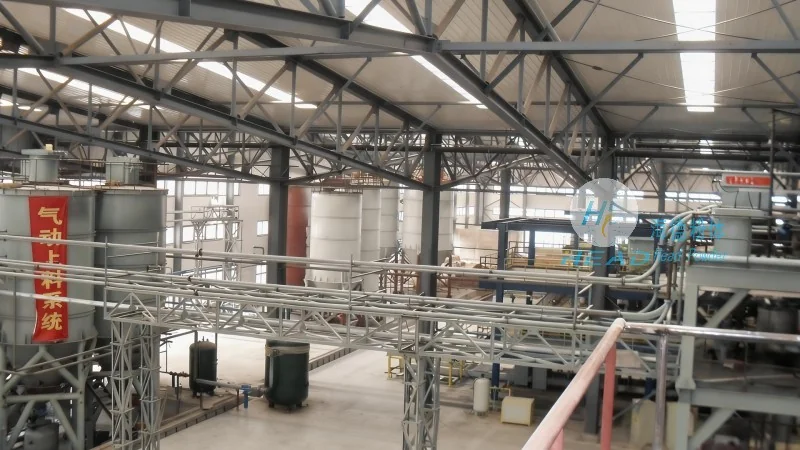
Coal ash conveying systems are widely used in various industries, particularly in the power generation sector. They are essential for thermal power plants that generate coal ash as a byproduct, as well as in recycling facilities that process coal ash for use in construction materials or other applications. The systems are also used in waste management facilities that handle other types of fine particulate materials, such as fly ash or bottom ash. The versatility of coal ash conveying systems makes them suitable for a wide range of applications, from small-scale processing to large-scale industrial operations.
In conclusion, the operation process and working principle of coal ash material conveying systems are critical to the efficient handling of coal ash. The systems are designed to handle the unique properties of coal ash, ensuring safe and reliable transport from the source to the processing or storage facility. With proper maintenance and operation, these systems can provide long-term performance and contribute to the overall efficiency of coal ash management. As the demand for coal ash utilization increases, the importance of effective conveying systems will continue to grow, making them a vital component of modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top