Understanding the operation process and working principle of ash silo material conveying systems is crucial for optimizing industrial material handling efficiency. These systems are integral to the management of bulk materials, particularly in power generation and waste management sectors, where ash and other byproducts require reliable transport from storage silos to processing or disposal units. The following sections detail the key components, operational steps, and technical mechanisms that enable smooth and efficient material transfer.
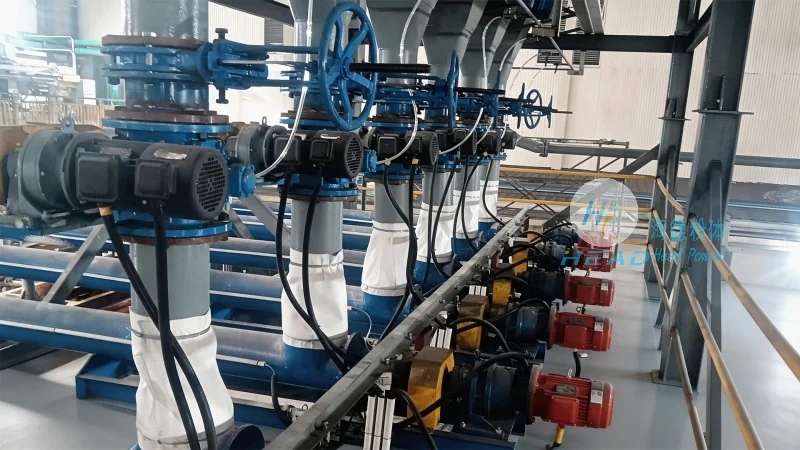
Ash silo material conveying systems are engineered to handle the movement of ash and similar bulk materials from storage silos to downstream equipment. These systems typically consist of a combination of components, including silo discharge mechanisms, conveyor belts or screw conveyors, and control systems. The design and configuration of the system are tailored to the specific characteristics of the material being handled, such as particle size, moisture content, and flowability. By integrating advanced technology and robust engineering, these systems ensure safe, efficient, and continuous material transport, minimizing downtime and operational risks.
The ash silo material conveying system comprises several critical components that work in concert to facilitate material transfer. The primary components include the ash silo itself, which serves as the storage vessel, and the discharge mechanism, such as a rotary valve or gate valve, that regulates the flow of material from the silo. The conveyor system, which may be a belt conveyor, screw conveyor, or pneumatic conveyor, is responsible for transporting the material from the silo to the next processing stage. Additionally, the system incorporates control panels and sensors that monitor and regulate the operation, ensuring precise control over the material flow rate and preventing overloading or blockages. The integration of these components is essential for maintaining the system's performance and reliability.
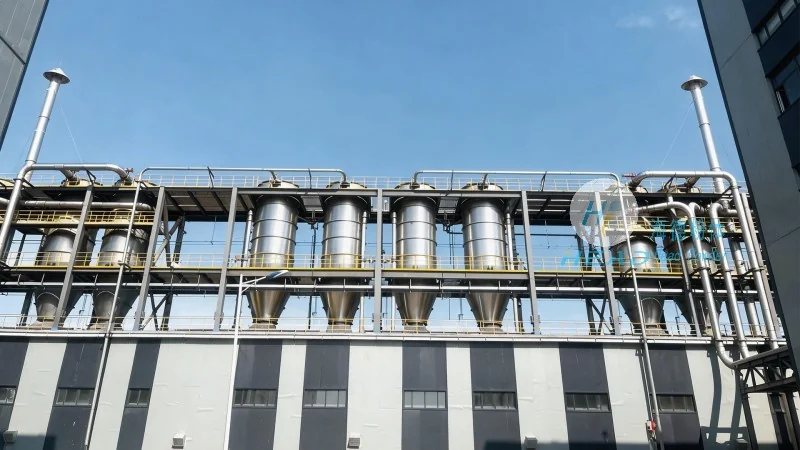
The working principle of the ash silo material conveying system involves a sequence of steps that ensure the continuous and controlled movement of material. The process begins with the material being discharged from the ash silo through the discharge mechanism. The material then falls into the conveyor system, where it is transported to the outlet or processing unit. The conveyor system utilizes mechanical energy, such as motor-driven belts or rotating screws, to move the material along its path. The speed and tension of the conveyor are carefully controlled to maintain consistent material flow and prevent material degradation or spillage. Sensors and control systems continuously monitor the system's performance, adjusting parameters as needed to maintain optimal operation. This closed-loop control system ensures that the material is conveyed efficiently and safely, minimizing the risk of operational disruptions.
The operation process of the ash silo material conveying system follows a systematic sequence of actions to ensure reliable material transfer. The initial step involves preparing the system for operation, which includes checking the condition of the silo, conveyor, and control systems. Once the system is ready, the discharge mechanism is activated to allow material to flow from the silo into the conveyor. The conveyor system then begins to transport the material at a pre-set speed, ensuring a steady flow to the next stage. During operation, the control system continuously monitors the material level in the silo and the flow rate through the conveyor, adjusting the discharge rate as needed to maintain a consistent output. If any issues arise, such as a blockage or overload, the system's safety features are activated, halting the operation and alerting operators to address the problem. The process concludes when the material has been fully transferred from the silo to the processing unit, and the system is prepared for the next cycle.
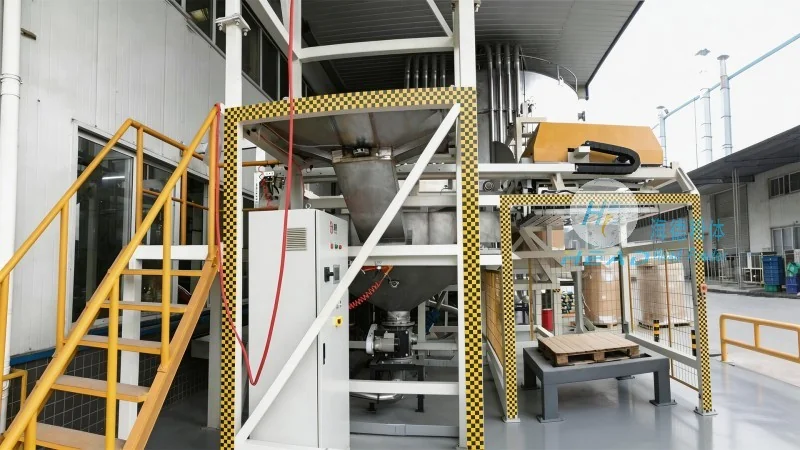
Several technical considerations are critical for ensuring the efficient and reliable operation of ash silo material conveying systems. Material characteristics, such as particle size and moisture content, significantly impact the system's performance and require appropriate equipment selection. For example, materials with high moisture content may require a conveyor system with enhanced sealing and lubrication to prevent material buildup and corrosion. The design of the silo and discharge mechanism must also account for the material's flow properties, using features like agitators or vibrators to improve flowability and prevent arching or bridging. Additionally, the system's control system must be capable of handling variable loads and maintaining precise control over the material flow rate. Regular maintenance and inspection of the system components are essential to prevent wear and tear, ensuring long-term operational reliability and minimizing downtime.
In conclusion, the operation process and working principle of ash silo material conveying systems are designed to provide reliable and efficient transport of bulk materials. By integrating advanced engineering, robust components, and intelligent control systems, these systems ensure safe and continuous material transfer from storage silos to processing units. The systematic approach to operation, combined with careful consideration of material characteristics and technical requirements, enables optimal performance and minimal operational risks. As industrial material handling demands increase, the importance of efficient ash silo conveying systems becomes more pronounced, making them a critical component of modern industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top