At Shandong HeadPowder Engineering Co., Ltd., our focus is on the efficient and reliable conveyance of cocoa materials. The operation process of our cocoa material conveying systems begins with the initial loading of raw cocoa beans or processed cocoa products into the feeding hopper. This step is crucial as it ensures a consistent and controlled flow of material into the conveying equipment. The feeding mechanism, typically equipped with adjustable speed controls, allows operators to regulate the volume of cocoa being fed, preventing overloading and maintaining optimal performance. Once the material is properly loaded, it moves into the primary conveying section, which may utilize various technologies such as screw conveyors, belt conveyors, or pneumatic systems depending on the specific characteristics of the cocoa material and the desired processing requirements.
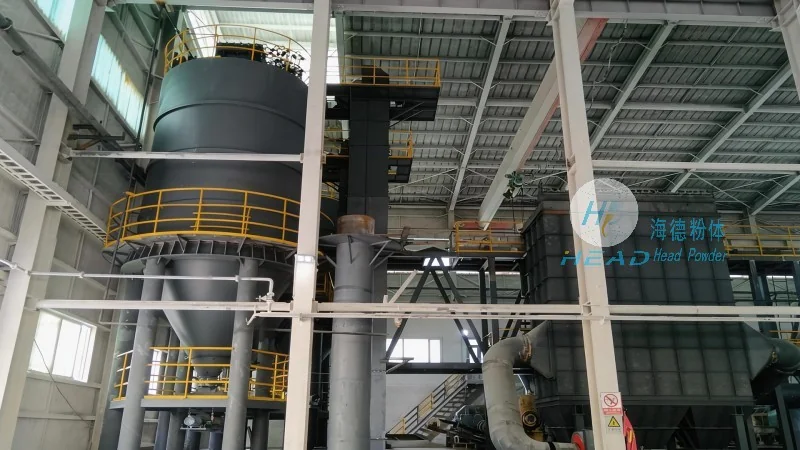
Our conveying systems operate on fundamental principles of material handling, combining mechanical and sometimes pneumatic forces to transport cocoa efficiently. The core components include the hopper for material storage, the conveyor mechanism (e.g., screw or belt), and the drive system that powers the movement. For screw conveyors, the rotating screw (or auger) creates a continuous helical path that lifts and propels the cocoa forward. This design is particularly effective for handling granular or semi-solid cocoa products, as it minimizes material degradation and ensures a smooth transfer. Belt conveyors, on the other hand, use a moving belt to transport cocoa, which is ideal for larger or bulkier items. The speed and tension of the belt are carefully calibrated to maintain stability and prevent spillage. Pneumatic conveying systems utilize air pressure to move cocoa particles through a pipeline, offering a dust-free and hygienic method suitable for sensitive cocoa products. Each system is designed with the specific properties of cocoa in mind, such as its density, moisture content, and potential for dust generation, to ensure optimal performance and product integrity.
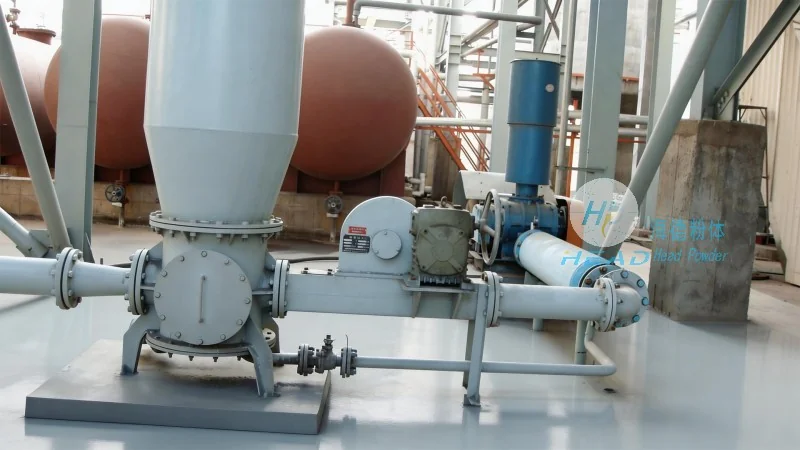
The effectiveness of our cocoa material conveying systems relies on several key components that work in harmony. The feeding hopper is the first component, responsible for storing and regulating the flow of cocoa. It is typically made of durable materials like stainless steel to withstand the abrasive nature of cocoa beans and prevent contamination. The hopper features a sloped bottom and a discharge valve that allows controlled release of material into the conveyor. The conveyor mechanism, whether screw, belt, or pneumatic, is the heart of the system, responsible for actual movement. The screw conveyor's auger is designed with a specific pitch and diameter to match the size of cocoa particles, ensuring efficient transport without clogging. The belt conveyor's belt is often made of food-grade materials and may include side guides to keep the cocoa on track. The drive system, which can be electric motor or pneumatic, provides the necessary power to rotate the screw or move the belt. Additionally, control systems, including sensors and variable frequency drives (VFDs), monitor and adjust the conveying speed in real-time based on material volume and system load. These components are integrated to create a seamless operation that minimizes downtime and maximizes productivity.
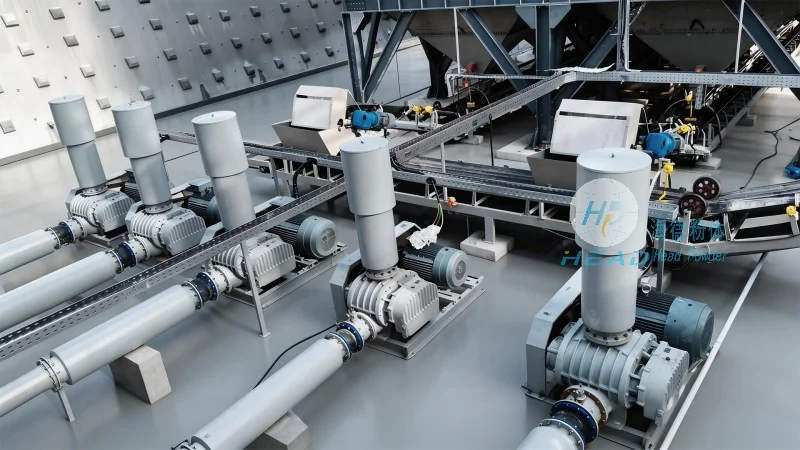
The entire operation process of our cocoa material conveying systems follows a systematic flow that enhances efficiency and product quality. The process starts with material intake into the hopper, followed by controlled feeding into the conveyor. The material then travels through the conveying section, where it is transported to the next processing stage, such as grinding or packaging. The system is designed to minimize material handling time and reduce the risk of contamination. To optimize efficiency, our systems incorporate features like automatic level controls that adjust the feeding rate based on the hopper's material level, preventing overfilling or underfeeding. Additionally, the use of sealed and dust-proof designs in the conveying components helps maintain a clean environment, which is critical for cocoa products that require high hygiene standards. Regular maintenance of the conveying system, including lubrication of moving parts and inspection of conveyor belts, is also essential to ensure consistent performance and extend the lifespan of the equipment. By adhering to these optimized processes, our systems achieve high throughput rates while maintaining the quality and integrity of the cocoa material throughout the conveying process.
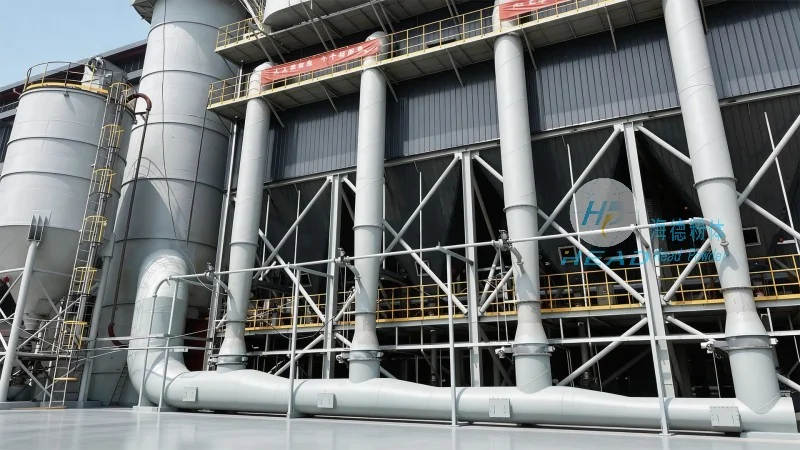
Our cocoa material conveying systems are widely used in the cocoa processing industry, from small-scale artisanal operations to large industrial facilities. The systems are designed to handle various forms of cocoa, including raw beans, roasted beans, cocoa nibs, and cocoa powder. Each application may require different conveying technologies, but all systems adhere to industry standards for food safety and equipment performance. For example, in the production of cocoa powder, the conveying system must ensure that the material is handled gently to avoid excessive grinding or particle breakdown. This is achieved through the use of low-speed screw conveyors or belt conveyors with minimal impact. In contrast, for bulk handling of roasted cocoa beans, higher capacity systems with robust screw or belt designs are used. The systems also comply with international standards such as FDA regulations and ISO certifications, ensuring that they meet the stringent requirements for food processing equipment. By aligning with these standards, our conveying systems provide reliable and safe operation, contributing to the overall quality and compliance of the cocoa products produced.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top