Pharmaceutical material handling systems are critical components in the pharmaceutical manufacturing industry, ensuring the safe, efficient, and compliant movement of raw materials, intermediates, and finished products throughout the production cycle. These systems are designed to meet stringent regulatory requirements, maintain product integrity, and enhance overall operational efficiency. In this article, we will explore the operation process and working principles of such systems, highlighting key elements and the role of specialized equipment in facilitating smooth material flow.
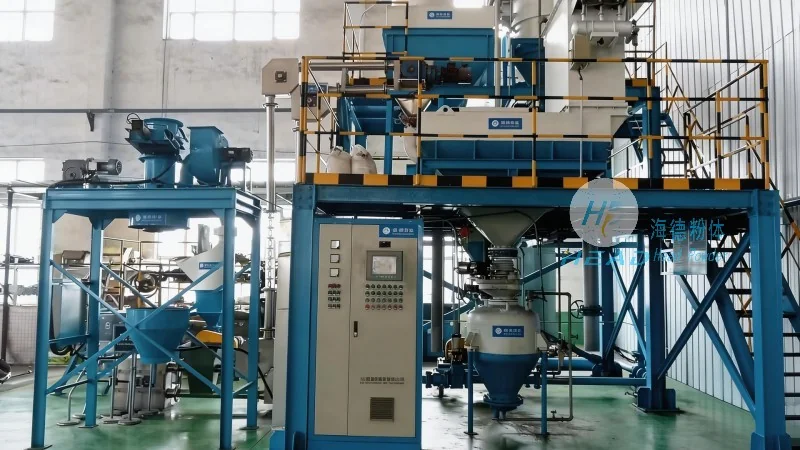
Pharmaceutical material handling systems typically consist of several interconnected components that work in tandem to achieve seamless material movement. These components include conveyors, storage solutions, sorting mechanisms, and control systems. Each component is engineered to handle the unique challenges of pharmaceutical materials, such as sensitivity to contamination, temperature control, and strict hygiene standards. For instance, headpowder, a leading provider in the field, integrates advanced technologies to ensure that every part of the system adheres to industry best practices.
The operation process of pharmaceutical material handling systems begins with inbound logistics, where raw materials are received and inspected for quality and compliance. This initial stage involves receiving, unloading, and storing materials in designated areas, often using automated storage and retrieval systems (AS/RS) to optimize space utilization. Once materials are verified, they are transferred to the production floor via conveyor systems, which may include belt conveyors, chain conveyors, or pneumatic conveyors, depending on the material characteristics and processing requirements.
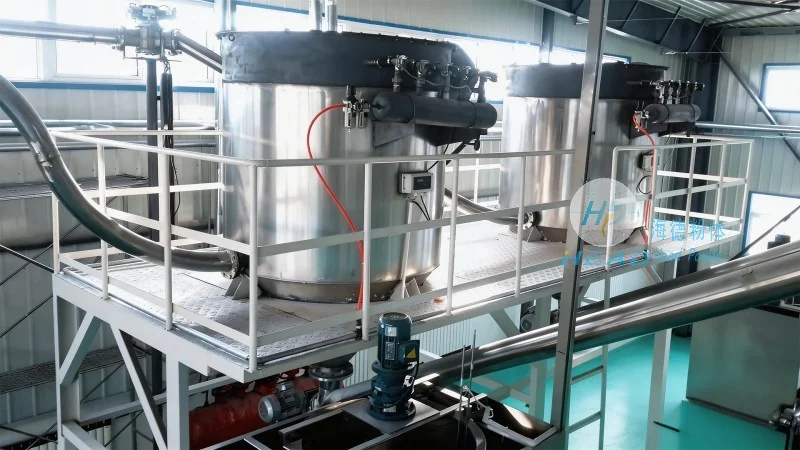
During the production phase, materials are processed through various stages, including mixing, compounding, and packaging. The handling systems ensure that each step is executed with precision, minimizing the risk of cross-contamination and maintaining batch traceability. After processing, the finished products are moved to the outbound stage, where they are sorted, packaged, and prepared for distribution. This final stage may involve automated packaging lines, labeling systems, and palletizing equipment to ensure that products are ready for shipment while adhering to regulatory guidelines.
The working principles of pharmaceutical material handling systems are centered on automation, precision, and regulatory adherence. Automation plays a crucial role in reducing human error and increasing throughput, as systems can operate continuously without interruption. Precision is achieved through advanced control systems that monitor and adjust parameters in real-time, such as speed, temperature, and pressure, to maintain product quality. Regulatory compliance is a top priority, as systems are designed to meet standards set by agencies like the FDA and EMA. This includes features like traceability, documentation, and cleaning protocols to ensure that every aspect of the material handling process is auditable and compliant.
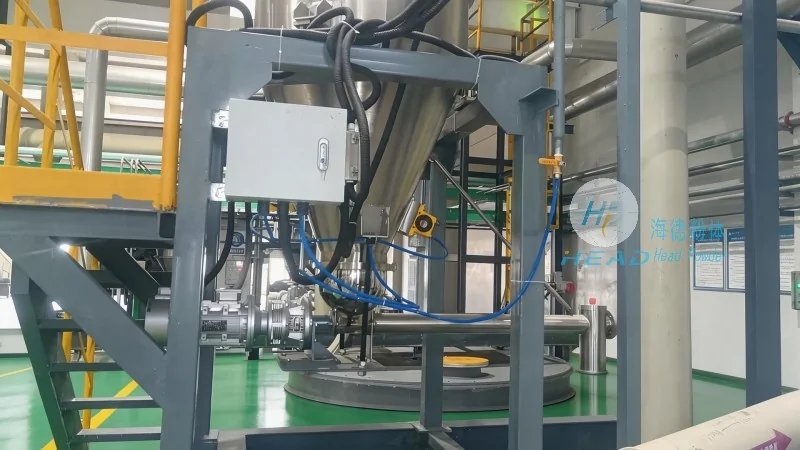
Headpowder, with its headquarters in Shandong, China, is a prominent manufacturer of pharmaceutical material handling solutions. The company specializes in designing and manufacturing customized systems tailored to the specific needs of pharmaceutical manufacturers. By leveraging years of industry experience and cutting-edge technology, headpowder provides solutions that enhance operational efficiency, reduce downtime, and improve product quality. The company's commitment to quality and compliance is reflected in its adherence to international standards and continuous innovation in material handling technologies.
In conclusion, pharmaceutical material handling systems are essential for the smooth operation of pharmaceutical manufacturing facilities. The operation process, which spans from inbound to outbound, relies on a combination of advanced equipment and meticulous control systems. The working principles of these systems prioritize efficiency, precision, and regulatory compliance, ensuring that pharmaceutical products are handled safely and effectively. With companies like headpowder leading the way, the pharmaceutical industry continues to advance in terms of material handling technology, supporting the production of high-quality medications and contributing to global healthcare.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top